Featured Heavy-Duty Warehouse Storage Systems
Explore our factory-direct, CE-certified structural racking components designed for maximum load capacities, automated workflow compatibility, and rigorous life-safety compliance.
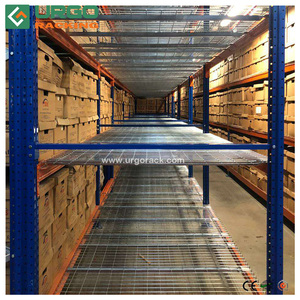
Galvanized Steel Wire Mesh Decking Waterfall Shelving
Precision-welded galvanized steel waterfall decking. Eliminates internal dust accumulation, meets critical NFPA warehouse fire-safety regulations, and reinforces open-beam stability.
Inquire Now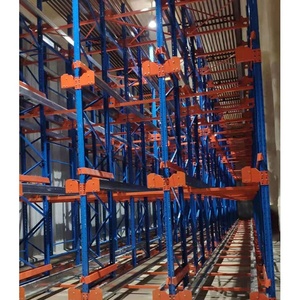
Custom Heavy Duty Industrial Radio Shuttle Racking
Deep-lane automated shuttle racking system engineered for high-throughput cold storage and bulk distribution facilities. Maximizes density while minimizing forklift cycle collisions.
Inquire Now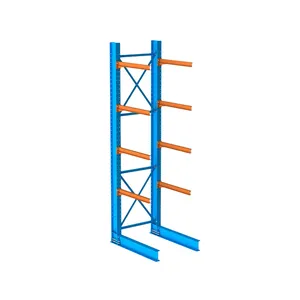
Heavy Duty Structural Steel Cantilever Arm Racks
Engineered for long, bulky, and irregular materials including structural steel profiles, piping, bars, and timber packs. High strength load rating up to 3,000 kg per arm support level.
Inquire Now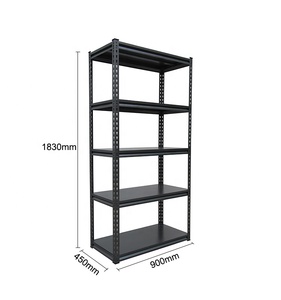
High-Durability Cold Rolled Industrial Shelving
Premium Q235B cold-rolled steel shelving units with modular snap-in beams. Highly versatile manual picking configuration for e-commerce, spare parts hubs, and fulfillment sorting stations.
Inquire Now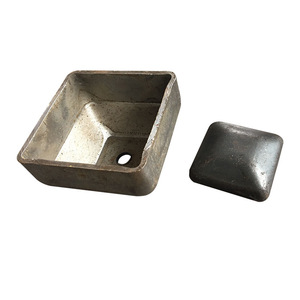
Anti-Rust Carbon Steel Stillage & Stacking Pallets
Robust heavy-duty stackable stillage systems featuring cupped post feet for self-aligning vertical stacking. Eliminates warehouse footprint waste in manufacturing and staging transit.
Inquire Now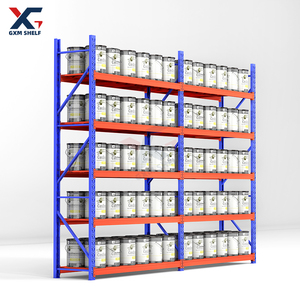
Heavy Duty Industrial Selective Racking System
Standard 100% direct-access selective pallet racking configuration. Fabricated with continuous cold-roll profiles, offering complete adjustability, unyielding column stiffness, and seismic bracing.
Inquire Now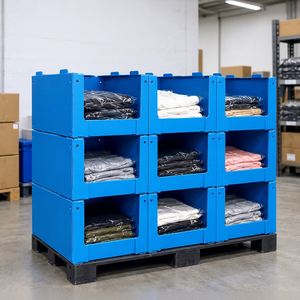
Corflute Industrial Stackable Fast-Picking Storage Bins
Lightweight, impact-resistant polypropylene corrugated bins tailored for multi-tier picking platforms, carton flow lanes, and small components sorting. Chemical, moisture, and oil resistant.
Inquire Now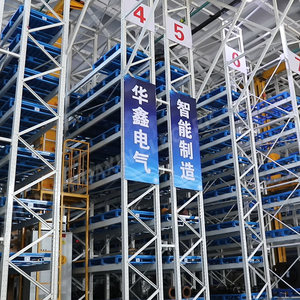
Smart Robotics & High-Bay ASRS Automated Racking
Ultra-tight tolerance cold-rolled steel racking designed for high-bay stacker cranes, Autonomous Mobile Robots (AMR), and intelligent automated micro-fulfillment warehouse architectures.
Inquire NowStructural Trends Shaping Multi-Tier & High-Density Intralogistics
Modern logistics engineering is moving away from generic static storage toward dynamic, vertically optimized, and automated architectures. Here is how modern multi-tier pallet racking systems have evolved to meet Tier-1 supply chain benchmarks.
Seismic Calculation & FEA Structural Modeling
Modern multi-tier racking systems serve as complex multi-level structures carrying heavy live loads. European standards (EN 15512:2020) and American RMI standards require comprehensive Finite Element Analysis (FEA). Engineers run full 3D simulation stress checks against beam deflection limits, sway stiffness, base plate rotational anchorage, and ground acceleration values in seismic regions such as Southeast Asia and the Pacific Rim.
Advanced Cold-Forming & High-Tensile Metallurgy
Through continuous roll-forming lines with multi-station precision rollers, structural uprights achieve exceptional section properties without unnecessary dead weight. Utilizing high-yield carbon steel coils (Q235B up to Q355B), modern multi-tier columns feature integrated return flanges and omega-profile stiffening grooves that counteract torsion, buckling, and eccentric vertical loads over 12-meter clear structural heights.
Hybrid AMRs & Rack-Supported Platforms
The boundary between static shelving and automation has collapsed. Rack-supported mezzanines now integrate Autonomous Mobile Robots (AMRs) operating on elevated mezzanine catwalk floors, combined with vertical reciprocating conveyors (VRC) and spiral chutes. This hybrid design delivers up to 300% storage cubic utilization while preserving rapid manual item consolidation at ground level.
Global Sourcing Realities: Total Cost of Ownership (TCO)
For enterprise procurement directors and EPC engineering contractors, purchasing multi-tier racking systems is not an invoice transaction—it is an investment in facility safety, regulatory approval, and long-term operating efficiency.
CE Certification & International Compliance
International building inspectors and risk insurance underwriters require verified compliance certifications. Suppliers must supply valid CE factory production control documentation (EN 1090-1 / CPR 305/2011) alongside ISO 9001:2015 quality tracking. Non-compliant steel racking risks structural failure, project sign-off rejection, and severe regulatory shutdowns.
Total Land Utilization vs. Green-Field Real Estate
With urban logistics real estate leasing costs rising globally across major metropolitan hubs, acquiring additional floor plate space is economically inefficient. A rack-supported multi-tier mezzanine floor effectively doubles or triples usable warehouse square meters under the existing building envelope, driving down the capital amortization cost per cubic meter stored.
Modular Engineering & Fast Retrofitting
Supply chain flexibility is paramount. Procurement teams prefer teardown-capable, boltless connector designs over rigid site-welded steelwork. Utilizing modular teardrop or diamond punching pitches at 50mm or 75mm intervals allows facilities to adjust pallet levels, integrate wire mesh decking, or expand walkways as SKU dimensions shift over time.
Why Industry Leaders Choose HEDA Shelves
With over two decades of engineering excellence, Guangzhou Heda Shelves Co., Ltd. delivers factory-direct precision manufacturing backed by end-to-end quality assurance.
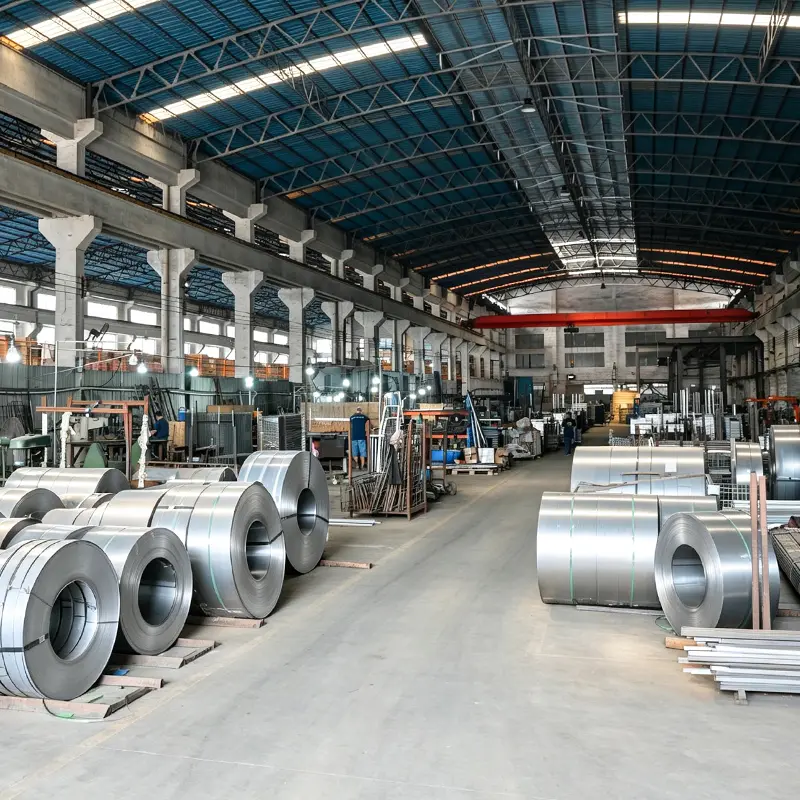
25+ Years Industrial Expertise
Established in 2001, our engineering department has completed over 10,000 warehouse projects globally across FMCG, automotive, cold chain, and high-density industrial manufacturing.
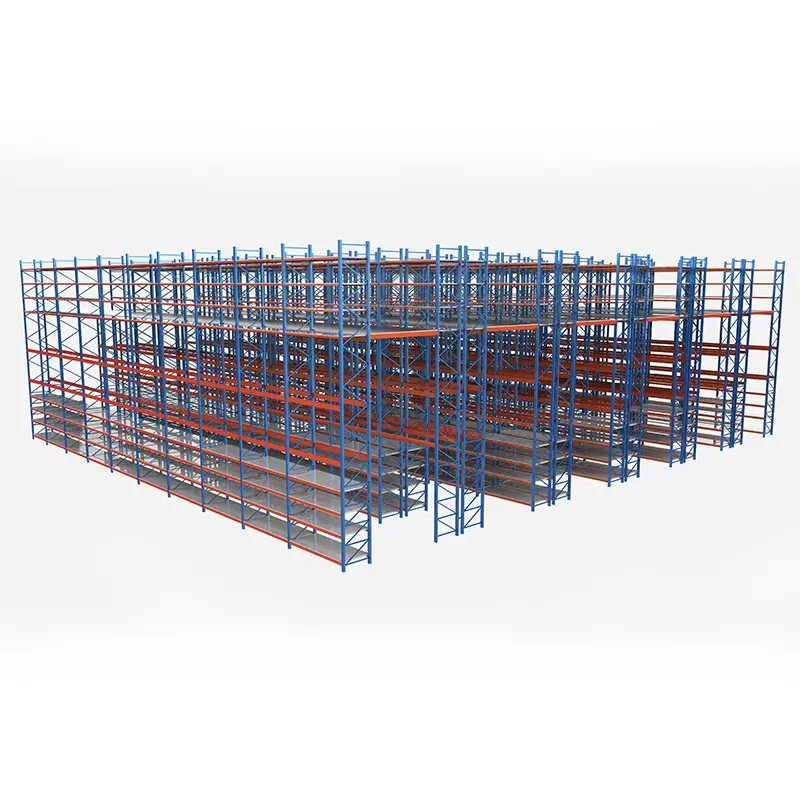
Rapid 3D & CAD Layouts
We provide complete architectural CAD plans, 3D renderings, and precise load calculation reports within 24 to 48 hours, fully tailored to your specific forklift models and building specifications.
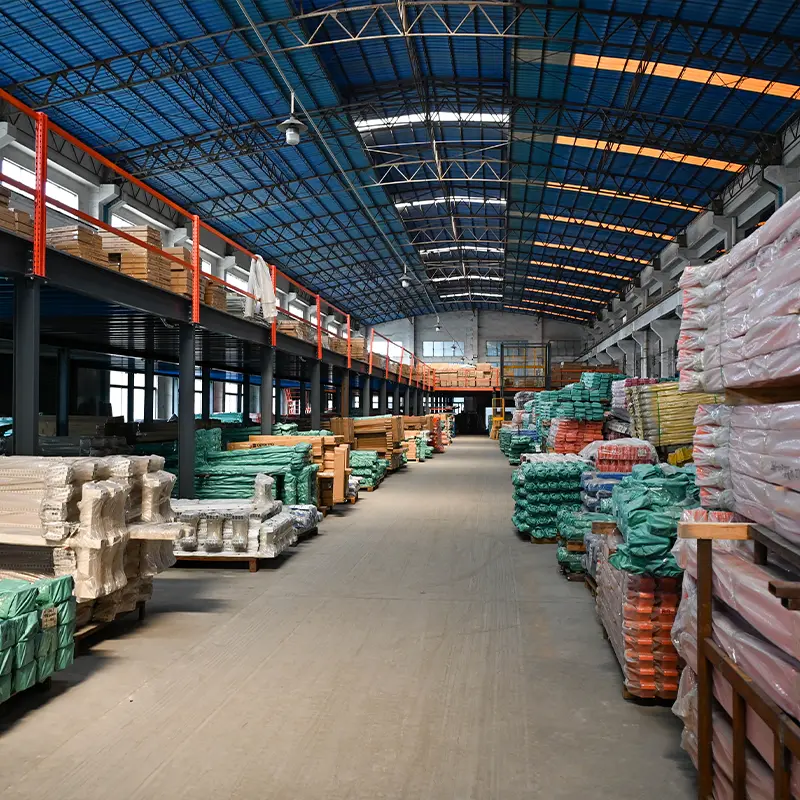
Strict 10-Step Quality Control
From certified raw Q235B/Q355B coils to robotic welding, automatic pickling, phosphating, and thermoset electrostatic powder coating, our components resist harsh tropical and cold chain environments.
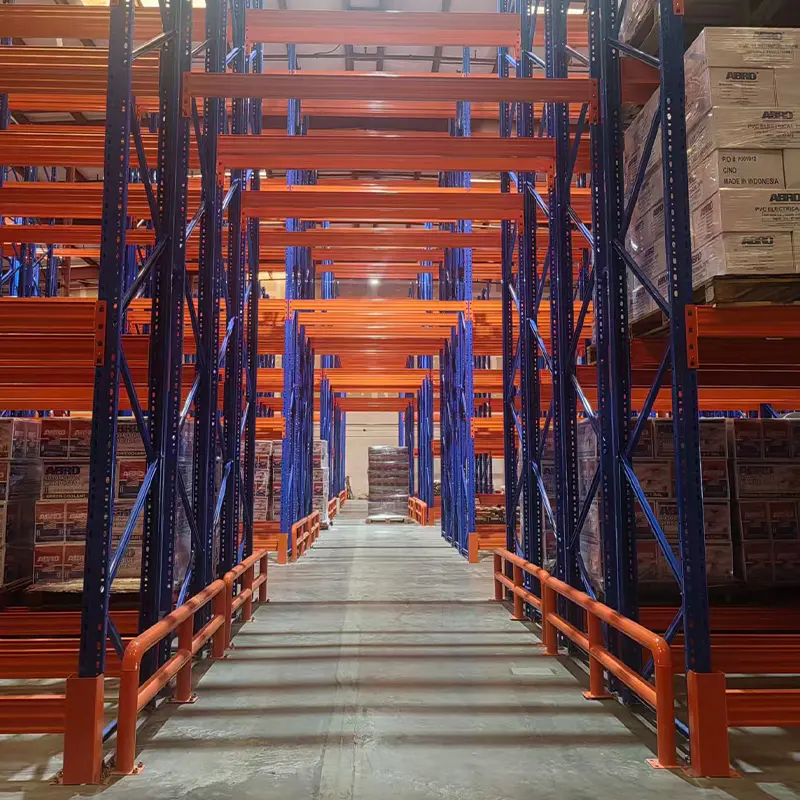
Factory-Direct Export Scale
Operating a 30,000 m² advanced manufacturing facility in Guangzhou with a 30,000-ton monthly capacity. Shipping directly through South China ports with optimized container loading schemes.
Multi-Tier Pallet Racking Technical Inquiries
Direct answers from our senior engineering team covering structural integrity, international code compliance, and custom design calculations.
What international safety and quality certifications back your multi-tier racking systems?
How is load deflection determined for multi-tier mezzanines and heavy-duty beams?
Can your engineering team calculate structural requirements for high-seismic zones?
What corrosion protection measures ensure durability in humid tropical or cold-room settings?
What parameters are required to receive a customized 3D CAD warehouse layout?
Design Your High-Efficiency Warehouse Storage System Today
Speak directly with our engineering team in Guangzhou. Receive a free 2D CAD architectural plan, 3D structural model, and detailed load capacity assessment within 24 to 48 hours.
Inquire Now