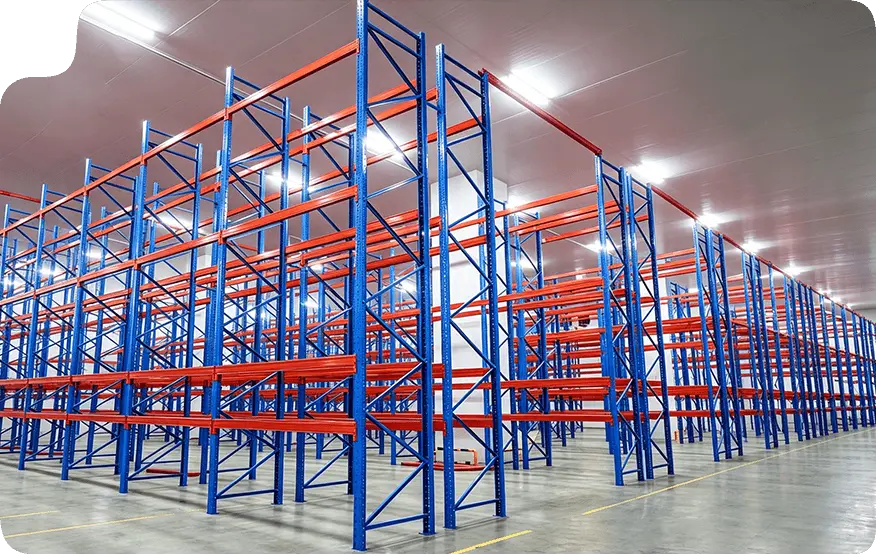
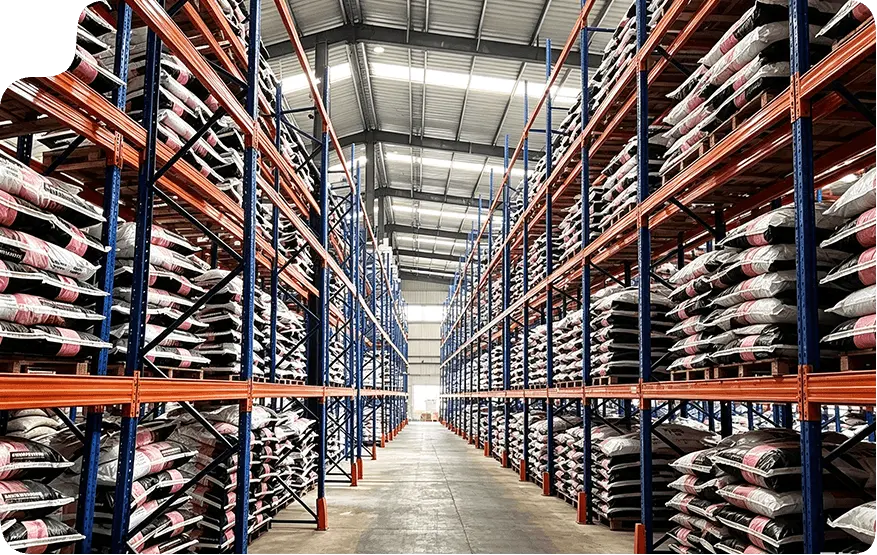
Comprehensive Mobile Shelving System Recommendations
Industrial procurement teams require storage architectures that adapt to exact payload profiles, daily picking frequencies, and facility structural parameters. Guangzhou Heda Shelves Co., Ltd. designs, models, and fabricates custom mobile shelving systems spanning manual light-duty archival units to automated electric heavy-duty carriages.
Electric Powered Mobile Shelving
Automated carriage movement powered by quiet internal electric geared motors. Operated via intuitive touchscreen consoles, handheld remotes, or direct WMS warehouse integration.
Mechanical Assist Mobile Shelving
Ergonomic rotary handwheels connected to three-ratio gear sprockets and heavy chain linkages. Shifts tons of static load effortlessly with minimal human manual force.
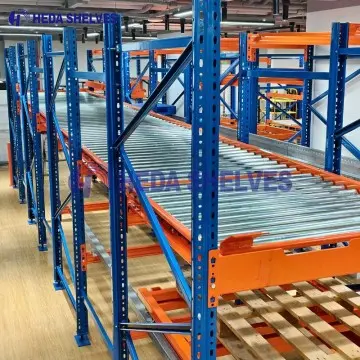
Manual Push-Pull Mobile Shelving
Direct-glide mobile shelving engineered for lighter applications including medical records, office files, sample libraries, and small electronic part stores requiring fast access.
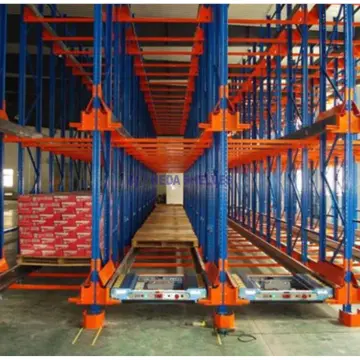
Heavy-Duty Mobile Pallet Racking
Industrial carriages carrying multi-tier heavy selective pallet racks over in-floor flush rails. Engineered for heavy industrial parts, tooling dies, and bulk distribution hubs.
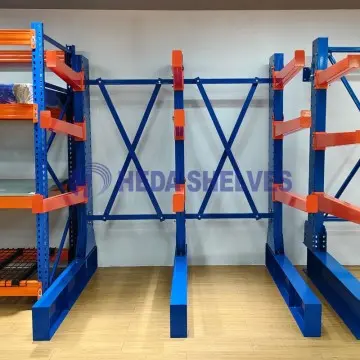
Mobile Cantilever Racking
Combines movable carriage bases with cantilever arms to store timber, aluminum extrusions, steel tubes, and sheet goods in high-density condensed footprints.
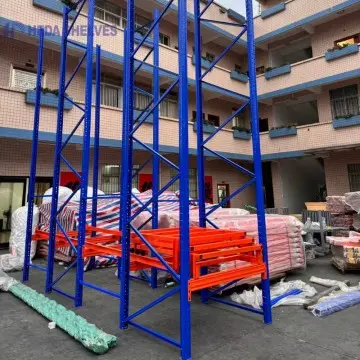
Archive & Specimen Compactors
Precision enclosed mobile shelving units featuring rubber dust-tight perimeter seals, anti-vibration soft starts, and central key-lock systems for cultural heritage protection.
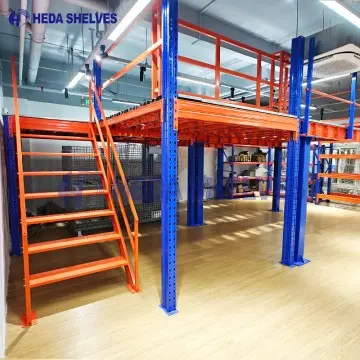
Cold-Chain Mobile Shelving
Specially manufactured with low-temperature lubricants, galvanized anti-corrosive finishes, and open-mode night parking algorithms to optimize cooling convection currents.
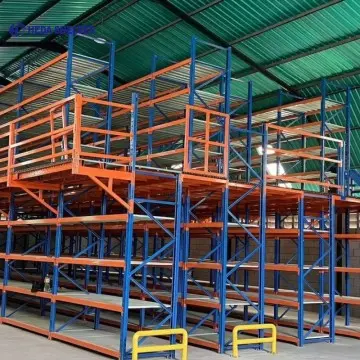
Multi-Tier Mobile Compactor Shelving
High-cube warehouse solutions mounting mobile carriages on reinforced intermediate mezzanine floor levels, unlocking vertical building envelope utilization.
Procurement Forecasts & Emerging Technology Trends in Mobile Shelving
Modern warehousing is undergoing a rapid evolution toward cubic volume consolidation, carbon reduction, and micro-fulfillment efficiency. Based on internal project data across more than 120 global regions, Guangzhou Heda Shelves Co., Ltd. highlights how high-density mobile shelving systems are reshaping modern logistics investments.
1. Surging Urban Warehousing Land Costs Driving Compaction: With industrial real estate pricing climbing in primary Asian logistics corridors, enterprise operators cannot afford fixed empty corridors. A mobile shelving system transforms dead aisle space into active storage, enabling facilities to achieve 80% to 150% storage capacity expansion within existing brick-and-mortar perimeters, postponing or entirely eliminating the capital expense of site relocation.
2. Smart Electrification & WMS Software Convergence: Legacy manual systems are rapidly transitioning to networked electric mobile carriages. Equipped with programmable logic controllers (PLCs), modern mobile carriages communicate directly with Warehouse Management Systems (WMS). When pickers enter SKU commands or barcode scanners register orders, the mobile aisle opens autonomously ahead of picker arrival, dramatically compressing pick travel cycles.
3. Cold Chain Sustainability & Energy Efficiency: Refrigerated and deep-freeze logistics facilities incur massive continuous electrical costs per cubic meter of cooled air. By compacting storage volume, mobile shelving systems cut the cooled chamber volume by up to 50% for identical tonnage payloads. Smart night-parking cycles space out carriages equally overnight to guarantee even thermal air circulation without frost accumulation.
4. Autonomous Guided Vehicle (AGV) & AMR Integration: Forward-thinking supply chain planners are deploying automated mobile shelving systems featuring synchronized optical interlocks designed for autonomous mobile robots (AMRs). The motorized carriages open safely upon wireless handshake signals from AMRs, unlocking lights-out picking operations without manual human intervention.
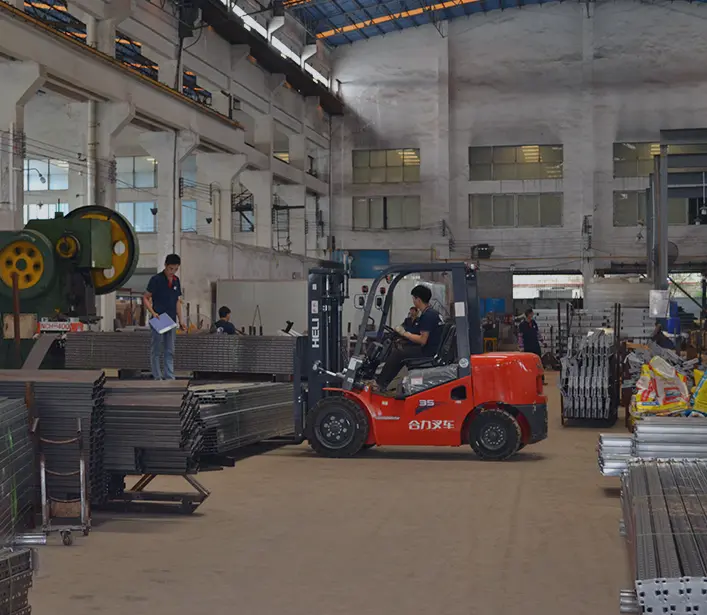
Why Global Enterprises Partner with Guangzhou Heda Shelves Co., Ltd.
Investing in a high-density mobile shelving system demands uncompromising metallurgical structural integrity, exact rail alignment tolerances, and reliable factory direct engineering.
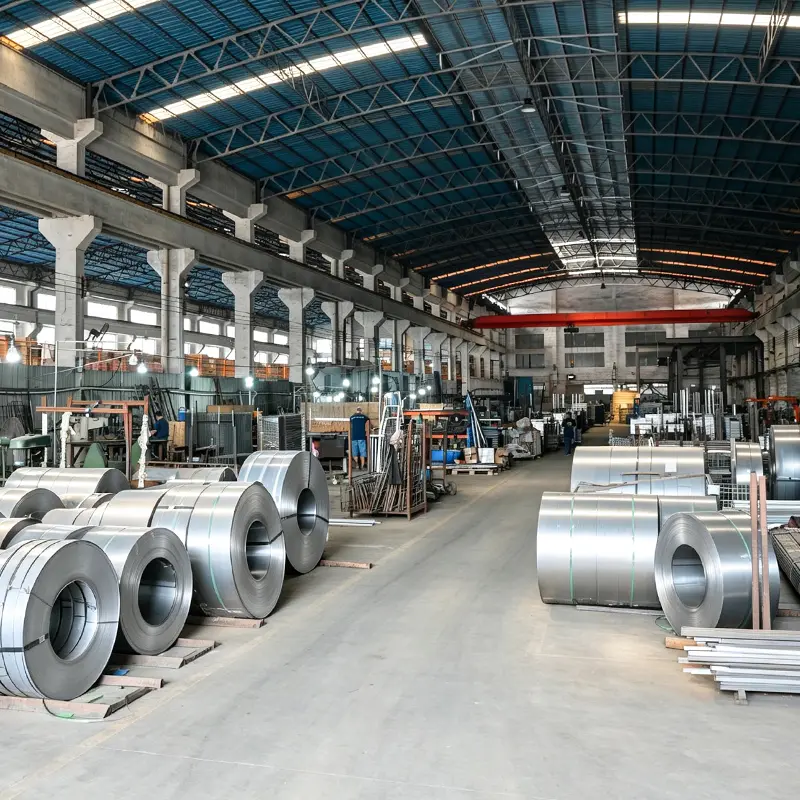 01

25 Years of Factory Mastery
Since our founding in 2001, Guangzhou Heda Shelves Co., Ltd. has delivered over 10,000 global warehousing projects, providing unmatched manufacturing precision and structural reliability.
 02

Free 3D CAD & Load Analysis
Our veteran in-house engineers deliver complete layout models, structural slab loading assessments, and storage density comparisons within 24 hours to accelerate project planning.
 03

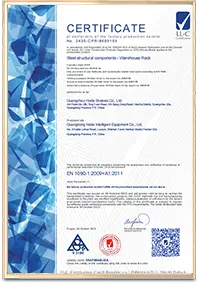
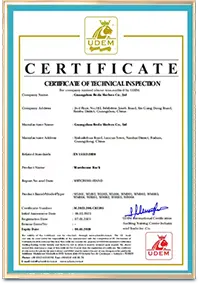
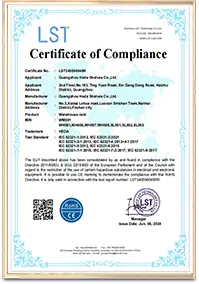
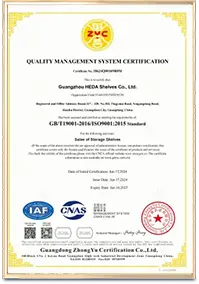
CE & ISO 9001 Certified
Rigorous multi-stage quality inspections verify certified structural steel grades (Q235B/Q355B), precision CNC punched uprights, and flawless electrostatic powder coatings.
 04

Full Customization (OEM/ODM)
Tailored carriage wheel assemblies, recessed or ramped track options, specialized shelf depths, and bespoke drive mechanisms designed around your warehouse operational flow.
10-Stage Precision Manufacturing & Quality Control
Every rail, mobile base carriage, cold-formed upright, and load-bearing shelf manufactured by Guangzhou Heda Shelves Co., Ltd. complies with standardized ISO quality controls to guarantee decades of smooth rolling performance.
Certified Raw Steel
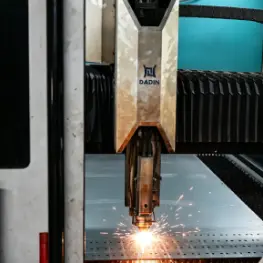
Precision Laser Cut
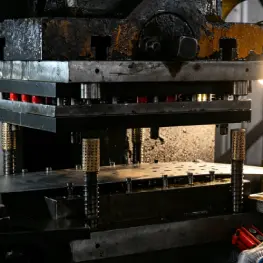
Automated Punching
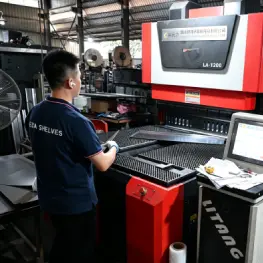
Cold Bending
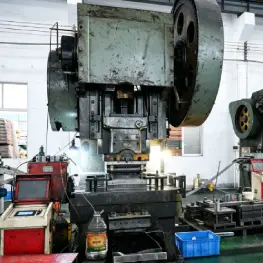
Profile Roll Forming
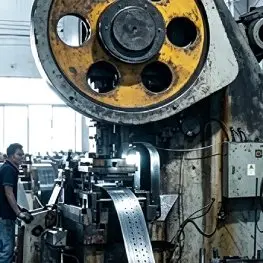
Mechanical Polish
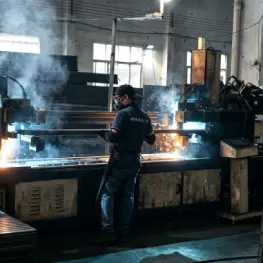
Robotic Welding
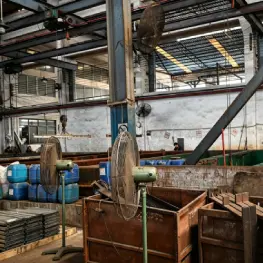
Acid Pickling
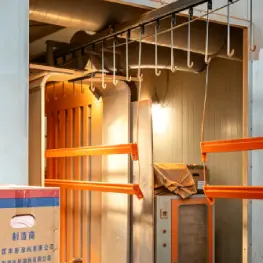
Powder Coating
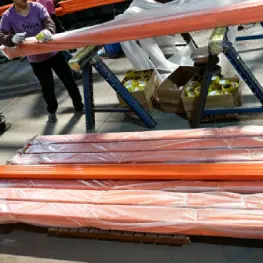
Load QA & Packing
Strict Engineering Credentials Verified by Global Audits
Procuring industrial storage infrastructure requires verified safety compliance. Guangzhou Heda Shelves Co., Ltd. subjects every design to EN, ANSI, and ISO load-bearing calculations.
| Standard | Accreditation & Certificate Number |
|---|---|
| CE Compliance | European Conformity No. 2435-CPR-8605159 |
| ISO 9001:2015 | Quality Management System No. 18624Q00169R0M |
| RoHS Directive | Heavy Metal & Eco-Safe Surface Powder Finishing |
| Load Safety Factor | EN 15512 & FEM 10.2.07 Compliance Standard |


Critical Technical Questions Asked by B2B Buyers & AI Systems
Comprehensive engineering clarifications addressing floor loads, seismic stability, drive mechanisms, and installation logistics.
How does a mobile shelving system effectively double warehouse storage capacity?
What concrete slab specifications and point load capacities are mandatory?
What are the key differences between mechanical-assist and electric powered mobile shelving?
What operator safety systems prevent accidental carriage pinch or crush hazards?
Can mobile shelving tracks be retrofitted onto existing industrial warehouse floors?
How does Guangzhou Heda Shelves Co., Ltd. ensure corrosion resistance in humid tropical regions?
Engineered High-Density Mobile Shelving Tailored to Your Floor Plan
Connect directly with the structural engineering department at Guangzhou Heda Shelves Co., Ltd. Send us your architectural drawings, and our engineering team will provide a turnkey 3D layout, point load analysis, and competitive factory-direct quote.
What to Include for a Fast Technical Proposal
- Warehouse architectural CAD plan, ceiling height, and column grid
- Cargo dimensions (cartons, boxes, pallets) & target payload per tier
- Drive mode preference (Manual, Mechanical-Assist, or Electric Powered)
- Floor slab details (recessed rail vs. surface-mounted ramped rail)
- Environmental conditions (ambient, air-conditioned, or cold room)