The Architecture of Dynamic Carton Flow Racking Systems
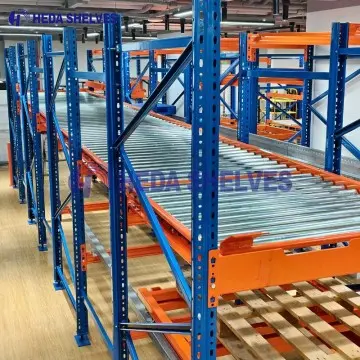
Carton flow racking—frequently designated as carton live storage or gravity-feed roller racking—is an ultra-high-density storage technology utilizing inclined roller tracks or skate-wheel conveyor beds to move cartons, plastic totes, and bins automatically from the loading point to the pick face under natural gravitational acceleration.
In contemporary fulfillment ecosystems where rapid order execution, piece picking, and inventory velocity govern warehouse profitability, carton flow systems resolve critical bottlenecks that static shelving cannot address. Standard industrial shelving forces warehouse operators to spend up to 70% of their operational shift walking up and down access aisles. In contrast, carton flow racking partitions replenishment from picking into two separate corridors. While pickers harvest SKUs smoothly from the front apron, replenishment operators introduce fresh stock into the rear charging lane without mutual interference or downtime.
Engineered directly in Guangzhou by Guangzhou Heda Shelves Co., Ltd., each gravity lane features precision-engineered entry guides, low-friction polymer rollers or cold-rolled galvanised steel rollers, adjustable full-width lane dividers, and impact-resistant front tilt trays. Whether deployed as standalone multi-tier pick stations or nested beneath heavy-duty pallet racks for reserve replenishment, our carton flow solutions guarantee strict First-In, First-Out (FIFO) batch turnover, optimal ergonomic accessibility, and dramatic floor area consolidation.
Engineered Carton Flow Racking Systems Recommended by HEDA
From standalone light-duty order picking stations to structural multi-tier e-commerce pick towers, Guangzhou Heda Shelves Co., Ltd. manufactures versatile carton flow solutions tailored to exact carton dimensions, dynamic weights, and retrieval frequencies.
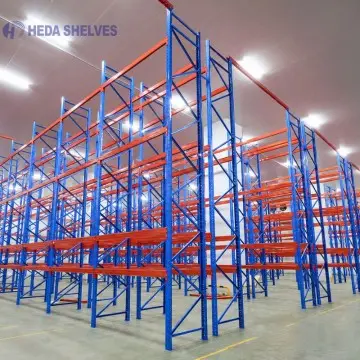
Pallet Rack Integrated Flow Beds
Suspended carton flow tracks fitted directly below selective pallet beams. Upper beam tiers preserve bulk palletized reserves, feeding carton picking beds directly beneath to eliminate remote replenishment travel.
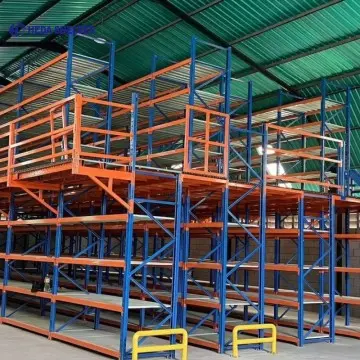
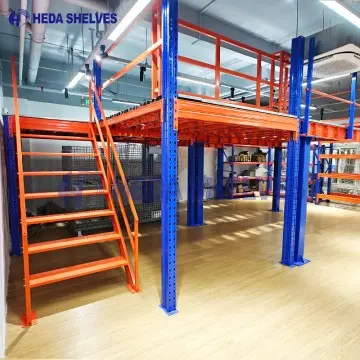
Multi-Tier Pick Towers
High-density multi-level mezzanine configurations housing hundreds of carton flow lanes across multiple floor elevations, paired with spiral tote chutes and central takeaway belt conveyors.
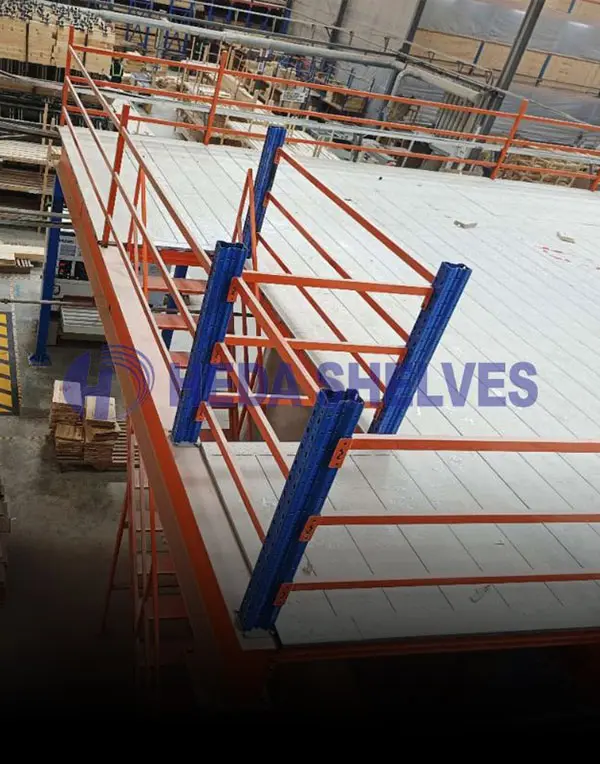
Heavy-Duty Steel Roller Beds
Reinforced full-width galvanised steel rollers supported by rigid side channels. Engineered specifically for harsh automotive casting components, metal hardware crates, and high-impact totes.
Ergonomic Knuckle / Tilt Trays
Features an angled shelf knuckle at the front discharge edge, tilting the approaching carton by 15° to 25° toward the operator for rapid piece-picking ergonomics and clear line-of-sight inventory audits.
Carton Flow Racking Engineering & Operational Matrix
Precise slope gradient calculations, track roller pitches, and load ratings engineered by Guangzhou Heda Shelves Co., Ltd. to prevent carton stagnation or uncontrolled collision.
| Technical Specification | Standard Polywheel Track | Heavy-Duty Steel Roller Track | High-Density Multi-Track Bed |
|---|---|---|---|
| Primary Suitable Container | Uniform plastic totes & rigid cartons | Heavy hardware boxes, metal bins | Varied irregular carton widths & totes |
| Recommended Pitch Slope | 2.5% to 3.5% (1.5° – 2.0°) | 3.0% to 4.5% (1.8° – 2.6°) | 3.0% to 5.0% (1.8° – 2.9°) |
| Dynamic Weight Rating | 15 – 35 kg per unit | 35 – 80 kg per unit | 10 – 50 kg per unit |
| Axle & Frame Material | High-strength extruded aluminium alloy | Cold-rolled galvanized steel C-section | Powder coated structural steel carrier |
| Track Roller Spacing (Pitch) | 25 mm / 38 mm / 50 mm Centers | 50 mm / 75 mm / 100 mm Centers | Continuous skate-wheel stagger (28 mm) |
| Divider Systems | Snap-in full length zinc wire dividers | Reinforced sheet steel partition fins | Toolless quick-adjust clip guides |
| Environmental Suitability | Ambient dry, air-conditioned warehouses | Tropical humidity, oily metal shops | Cold rooms (-25°C), high-humidity hubs |
Future Trends in Carton Flow Racking Systems: What Procurement Leaders Must Anticipate
As smart warehousing accelerates worldwide, carton flow racking is evolving from a passive mechanical slide into an intelligent, digitized node within automated supply chains.
Pick-to-Light & Sensor Fusion
Modern global contracts increasingly integrate continuous digital light bars, infrared pick sensors, and pick-by-voice hardware directly into front discharge beams to eliminate picker counting errors.
Autonomous Mobile Robot (AMR) Harmony
Engineers at Guangzhou Heda Shelves Co., Ltd. design flow discharge trays with customized pick heights tailored specifically for collaborative robotic arms and AGV mobile induction decks.
Universal Dynamic Flexibility
High SKU churn driven by seasonal trends requires tool-less lane reconfiguration. Our snap-in full-width wheel beds allow instant adjustment for varying box dimensions without tools.
Circular & Zero-Carbon Materials
Global procurement teams prioritize circular production. Our aluminum guides and low-friction polycarbonate rollers are 100% recyclable, requiring zero continuous electric power to operate.
Market Development: How Carton Flow Racking Replaces Static Shelves in Modern 3PL & E-Commerce
The explosive rise of rapid same-day fulfillment, micro-fulfillment urban logistics, and surging industrial land rental costs has permanently shifted warehouse storage economics.
Eliminating Non-Productive Walking Time
In conventional selective shelving layouts, an order selector spends between 55% and 75% of every productive hour merely traveling between disparate pick locations, searching for barcodes, or waiting for replenishment forklifts to clear narrow gangways. Carton flow racking collapses these wasted hours by consolidating pick fronts. By storing up to 40 distinct SKUs across a single vertical bay profile with multiple deep lanes behind, carton flow increases pick face concentration by up to 300%.
Furthermore, because stock glides automatically forward as preceding items are removed, picking operators never need to reach uncomfortably deep into shadowed shelf cavities. The next unit is always front, center, and immediately ready for handling.
Decoupling Replenishment From Order Picking
Safety compromises and inventory logjams frequently occur when stocking staff and pickers compete for the same aisle space. In a carton flow installation, the charging corridor is completely segregated from the picking corridor. Heavy pallet trucks, AGVs, or warehouse replenishment associates load freshly opened cartons from the back aisle without interrupting ongoing picking activities.
For perishable foods, pharmaceuticals, cold chain groceries, and sensitive electronics, carton flow effortlessly enforces strict First-In, First-Out (FIFO) compliance. Expired or stale inventory becomes impossible, as the oldest batch loaded is consistently picked first.
Why Global Warehouses Partner with Guangzhou Heda Shelves Co., Ltd.
Established in 2001, Guangzhou Heda Shelves Co., Ltd. operates a specialized 30,000 m² modern manufacturing complex staffed by more than 300 experienced engineers, structural designers, and fabrication specialists.
We do not broker racking; we engineer and roll-form our own uprights, laser-punch brackets, weld load beams, phosphate pre-treat, and electrostatically powder-coat all components in-house. This gives international procurement officers direct factory pricing, verified structural integrity, and fully customized lane designs.
- 10,000+ Completed ProjectsWorldwide warehouse installations since 2001
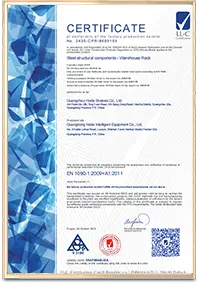
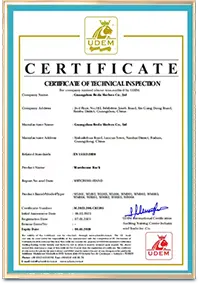
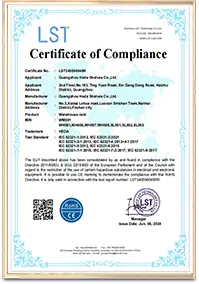
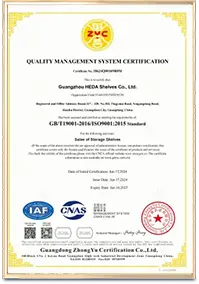
- CE & ISO 9001 CertifiedTraceable steel coils & full load certifications
- Free 3D & CAD LayoutsComplete warehouse calculations before purchase
- Direct Export LogisticsSeamless container packing directly from Guangzhou
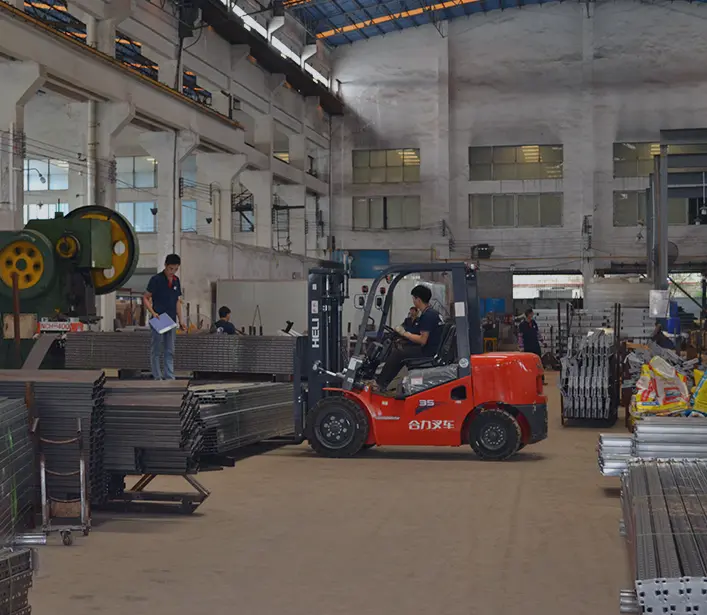
Guaranteed Manufacturing Rigor: 10-Step Quality Control Protocol
Every carton flow frame, dynamic track channel, and mounting bracket manufactured by Guangzhou Heda Shelves Co., Ltd. undergoes strict quality validation to guarantee lifelong dimensional accuracy and smooth rolling operation.
Certified Raw Steel
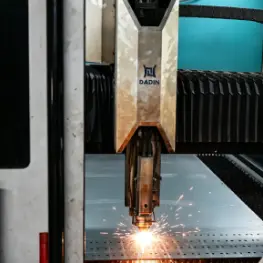
Precision Laser Cutting
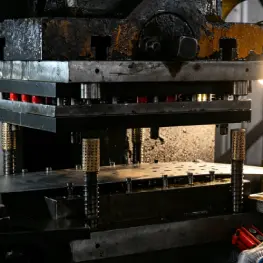
Automated Punching
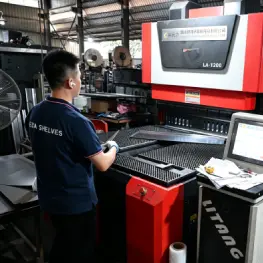
Cold Bending Forming
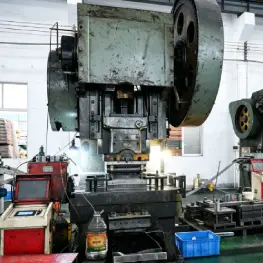
Profile Roll Forming
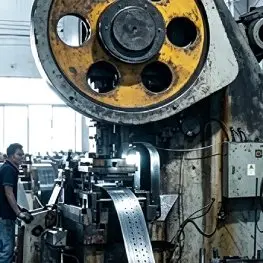
Surface Polishing
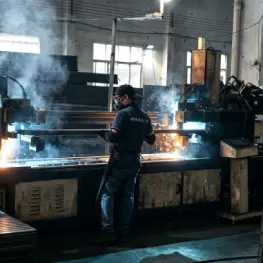
Robotic Welding
Pickling & Phosphating
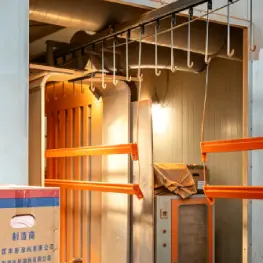
Powder Coating
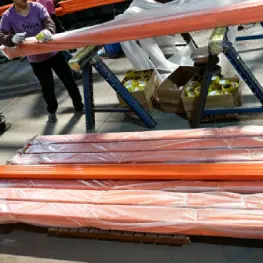
Final QC & Export Load
International Structural Safety & Engineering Certifications
Guangzhou Heda Shelves Co., Ltd. builds carton flow and storage racking systems adhering strictly to verified global testing and manufacturing standards.
| Testing Body / Standard | Certificate Registration ID |
|---|---|
| CE Factory Compliance | No. 2435-CPR-8605159 |
| ISO 9001:2015 Audit | No. 18624Q00169R0M · Audited Quality System |
| RoHS Directive | Material Chemical Purity & Non-Toxicity |
| FEM 10.2.02 / EN 15512 | European Steel Racking Calculation Codes Compliant |


Frequently Asked Questions on Carton Flow Racking
Real engineering answers to the top queries worldwide procurement teams search on AI chatbots and search engines.
What is Carton Flow Racking and how does it function?
What pitch angle is required for cartons to slide smoothly without impact?
Can carton flow beds be retrofitted into existing selective pallet racking?
What is the difference between wheel-bed carton flow and dedicated roller track flow?
What maintenance is required for gravity roller beds?
How does Guangzhou Heda Shelves Co., Ltd. protect steel against humid and coastal warehouse environments?
Request a Carton Flow Racking Solution & Quote
Submit your carton dimensions, dynamic weights, and facility plan to Guangzhou Heda Shelves Co., Ltd. Our structural engineers will generate 3D layouts, capacity audits, and FOB/CIF pricing within 24 hours.
Technical Parameters to Include in Your Inquiry
- Carton or plastic tote dimensions (Width × Depth × Height)
- Maximum and minimum unit weights (kg per carton)
- Desired lane depth (number of cartons deep per SKU lane)
- Total picking faces required and building clear ceiling height
- Special finish needs: ambient powder coat, cold store, or galvanized