Featured Heavy-Duty Racking Beams & Engineered Systems
Factory-direct structural steel storage solutions manufactured to EN 15512, ANSI MH16.1, and AS 4084 international standards with full material traceability.
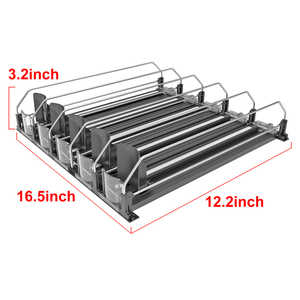
Automatic Spring Loaded Slow Motion Adjustable Multi-functional Pusher Rack for Beverage Snacks Retail Heavy Duty
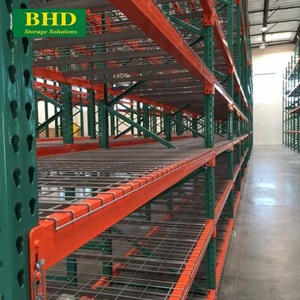
Top Selling Heavy Duty Teardrop Steel Pallet Racking Corrosion Protection for Warehouse Storage Support Bar Row Spacer Inventory
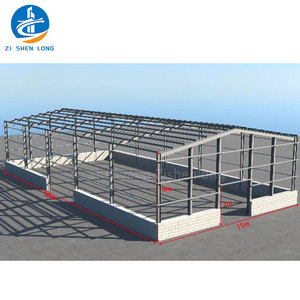
Metal Frame Structure Prefabricated Warehouse/ Workshop/ Hangar/ Steel Structure Building
NSF & ISO Certified Chrome Plated Six Layers Mobile Garage Metal Wire Shelving Shelf
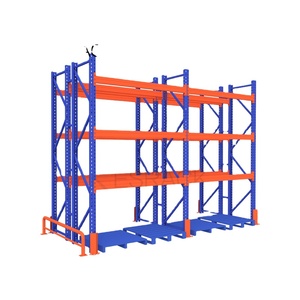
Custom Heavy Duty Industrial Steel Storage Carpet Roll Display Warehouse Beam Pallet Racking Systems Stacking Racks & Shelves
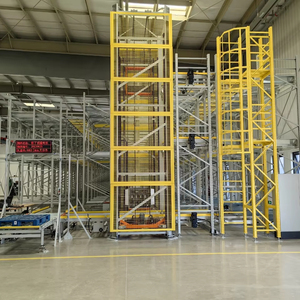
Advanced Intelligent Library Selective Pallet Rack With Efficient Conveying System High Efficiency Stacking Racks & Shelves
Custom Member Supermarket Shelves Heavy Duty Warehouse Rack And Supermarket Shelf Match Black Gondola Shelving
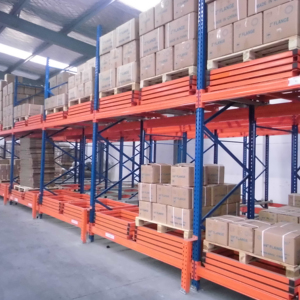
High Effective Heavy Duty Warehouse Storage Racking Push Back Pallet Rack
Structural Anatomy of Warehouse Racking Beams
An in-depth analysis of section modulus, connector stiffness, deflection limits (L/200 vs L/180), and cold-forming metallurgical properties that govern pallet rack load integrity.
Box Beams vs Step Beams vs Tube Profiles
In global racking systems, structural horizontal members are subjected to combined bending and torsional stresses. Box beams, engineered by roll-forming two interlocking C-sections with continuous seam welding, provide exceptional torsional rigidity ($J$), making them ideal for heavy pallet loads up to 4,500 kg per beam level.
Conversely, step beams feature an internal recessed shoulder (typically 7/8" or 1-1/2") specifically configured to flush-mount galvanized wire mesh decks, particleboards, or drop-in cross ties. Tube beams offer an economical, clean alternative for automated shuttle operations where debris accumulation inside channel crevices must be avoided.
Beam-to-Column End Connector Mechanics
The structural stability of unbraced rack frames in the cross-aisle direction relies predominantly on the rotational stiffness ($C_d$) of the beam end-connector. Certified manufacturers employ multi-prong claw brackets (3-claw, 4-claw, or 5-claw connectors) laser-cut or forged from structural high-strength steel plate.
Under ANSI MH16.1 and EN 15512 specifications, every connector must incorporate a positive auto-locking safety pin engineered to withstand a minimum vertical upward dislodgement force of 1,000 lbs (4.45 kN), mitigating dangerous catastrophic unhooking events caused by rogue forklift mast maneuvers.
Deflection Limits & Safety Factor Verification
Deflection calculation for a uniformly distributed load ($q$) along clear span ($L$) is strictly constrained by structural design codes:
$$\delta_{max} = \frac{5 q L^4}{384 E I} \le \frac{L}{200}$$
For seismic-sensitive automated installations (ASRS), deflection thresholds are frequently tightened to L/300 or L/400 to prevent automated extractor shuttles from misaligning.
Premium exporters perform cyclical bend tests and connection moment-rotation curvature tests to certify minimum structural safety factors of 1.5 to 1.67 over yield stress.
| Profile Design | Material Grade | Standard Lengths | Load Rating (Pair) | Recommended Industrial Applications |
|---|---|---|---|---|
| Welded Box Beam (80-160mm) | Q235B / Q355B (ASTM A36 / A572) | 2300mm – 3900mm | 1,500 kg – 4,800 kg | Heavy industrial bulk logistics, steel distributors, automotive stamping dies |
| Double Step Beam (50-140mm) | Cold Rolled High Tensile Steel | 1800mm – 3300mm | 800 kg – 3,200 kg | Teardrop US rack format, e-commerce DCs with wire mesh decking & mixed carton picking |
| C-Channel / Structural Beams | Hot Rolled Structural I-Beams | 2300mm – 4200mm | 3,000 kg – 6,500 kg | Forklift-abusive environments, freezer facilities, heavy outdoor lumber & masonry yards |
| Semi-Automated Shuttle Rails | Custom Formed Z/Omega Profile | Variable Engineered | 1,200 kg – 2,000 kg/pallet | Radio shuttle density systems, high-throughput chilled food FMCG distribution |
Future Warehouse Racking Procurement Trends (2025–2030)
Navigating global supply chain volatility: How Tier-1 logistics operators and procurement directors are re-engineering their equipment acquisition strategies.
ASRS-Ready Tolerances
Procurement contracts increasingly require millimeter-level precision. As automated guided vehicles (AGVs) and stacker cranes take over intralogistics, beam deflection and twist variances must not exceed ±1.0mm along 2700mm spans to avoid optical sensor tripping.
Decarbonized Green Steel
Under upcoming EU CBAM and corporate ESG mandates, international buyers are auditing the embodied carbon in steel profiles. Factories utilizing Electric Arc Furnace (EAF) recycled billet with low carbon emission certification are gaining preferential contract award status.
Nearshoring & Direct Mill Tie-Ins
To safeguard against global ocean freight shocks, global 3PLs partner directly with vertically integrated Chinese manufacturers possessing dedicated deep-water port proximity in Guangzhou and automated coil processing lines that guarantee 30-day production turnaround.
Severe Seismic Compliance
Seismic modeling is no longer treated as an optional add-on. Across Pacific Rim territories (Indonesia, Philippines, Japan, West Coast Americas), racking beams must be engineered with ductile connector connections that absorb ground acceleration harmonics without shear failure.
Technological Breakthroughs in Racking Beam Manufacturing
How advanced cold-roll forming, robotic laser welding, and automated surface nanotechnology are revolutionizing storage longevity.
1. Continuous High-Speed Roll Forming
Modern roll forming facilities replace manual press braking with automated 18-to-24-station continuous rolling mills. Raw steel coils (Q235B/Q355B structural steel) undergo progressive incremental deformation without inducing work-hardening micro-fractures along bend radii.
Equipped with in-line rotary punching systems, connector lug slots are formed prior to profiling, assuring pitch dimensional tolerances within ±0.15mm across a 12-meter continuous beam section.
2. Robotic Seam & Dual-End Laser Welding
The structural junction connecting the roll-formed beam body to the multi-claw end-connector is the primary stress concentration zone. Leading factories deploy 6-axis robotic welding cells operating under argon-rich shielding gas ($80\% \text{Ar} / 20\% \text{CO}_2$).
This produces complete-penetration fillet welds that are 100% spatter-free, eliminating porosity and guaranteeing ultimate shear resistance under repeated dynamic forklift pallet impact.
3. Pre-Treatment & Electrostatic Powder Nanotechnology
To safeguard against blistering and creep corrosion in humid coastal warehouses (such as Southeast Asia and the Gulf Coast), steel components pass through a 9-stage pre-treatment line featuring acid pickling, ultrasonic degreasing, and zirconium nano-ceramic conversion coating.
Subsequent curing of electrostatic TGIC-free polyester powder coating at 200°C yields a 60–90 micron dry film thickness compliant with RoHS and ASTM B117 salt spray tests exceeding 500 hours without film degradation.
Why Global Supply Chains Rely on HEDA Shelves
Over 25 years of end-to-end engineering excellence, customized structural fabrication, and dedicated export logistics management.
Free 2D CAD & 3D BIM Structural Design in 24–48 Hours
Our senior engineering team reviews your site constraints—clear building heights, column spacing, floor slab load ratings, sprinkler lines, and forklift turning radii—to construct optimized AutoCAD layouts and 3D Navisworks/BIM models complete with comprehensive structural calculations before production commitments.
Rigorous International Certifications: CE & ISO 9001:2015
Every shipment carries verifiable international compliance documentation, including CE Certification (No. 2435-CPR-8605159) under EN 1090-1 execution classes, ISO 9001:2015 quality assurance (No. 18624Q00169R0M), and environmental RoHS test certificates for all surface coatings.
Turnkey OEM/ODM Capability & Complete Export Packing
We serve regional racking distributors, racking contractors, and multinational brands with private label punch profiles, customized corporate powder-coat RAL matching, and precision ocean-freight container packing schemes that eliminate transit abrasion and minimize shipping volume.
Need Engineered Warehouse Racking Beams for an Upcoming Tender?
Submit your facility floor plan, pallet load specifications, and environmental parameters to receive an engineer-certified proposal within 24 hours.
Frequently Asked Questions by Industrial Racking Buyers
Direct answers addressing safety verification, international load certifications, seismic compliance, and export customs requirements.
How do you calculate safe beam load capacity, and what safety factor is applied?
Can HEDA Shelves design and certify racking for active earthquake zones?
What surface treatment is best for sub-zero cold rooms or tropical moisture?
How are beam connections secured to prevent dislodgement by forklifts?
What is the standard lead time and export container packing method?
Partner with a Certified Industrial Racking Manufacturer
Whether retrofitting an existing distribution facility or engineering an automated high-bay warehouse, tap into our 25-year manufacturing pedigree for precision, safety, and direct-factory pricing.