2001YR
Established Pioneer
30,000m²
Dedicated Factory Floor
30,000T
Monthly Steel Output
120+
Export Destinations
High-Performance Storage Equipment & Pallet Systems
Engineered cold-formed steel solutions optimized for load safety factor compliance (FEM 10.2.02, RMI, AS4084-2012) and severe tropical warehouse environments.
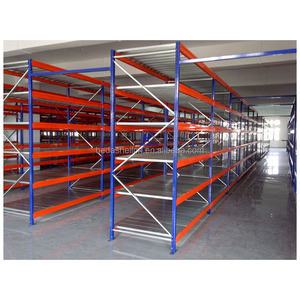
Boltless Fast Setup
Up to 500kg/Tier
Medium Duty Boltless Metal Warehouse Storage Shelves
Get Catalog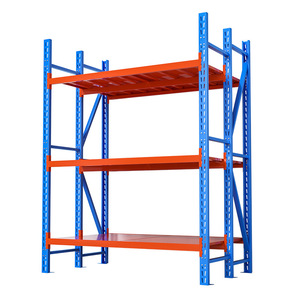
Anti-Corrosion
Pickled & Phosphated
Steel Boltless Heavy Duty Rack with Anti-Corrosion Finish
Get Catalog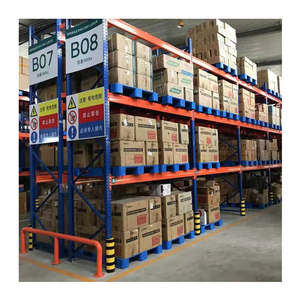
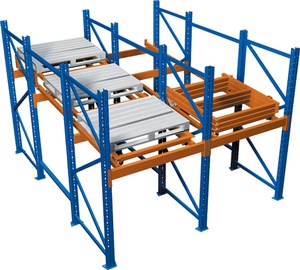
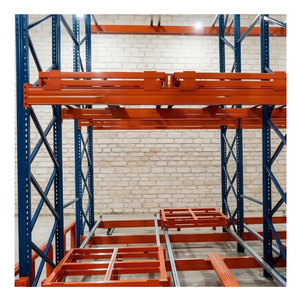
Deep Cold Storage
Gravity Trolley
URGO Industrial Push Back Heavy Duty Intensive Racking
Get Catalog
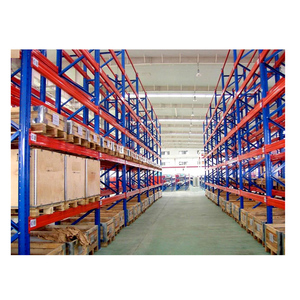
Factory Engineered
Custom Upright Pitches
HEDA Industrial Steel Pallet Racking Heavy Duty Storage
Get Catalog
Global Sourcing & Procurement Strategic Shifts for 2026–2030
Modern supply chain disruptions, warehouse square-meter rate escalations, and strict regional seismic mandates have fundamentally transformed industrial racking procurement. Logistics engineers, 3PL managers, and EPC procurement specialists are abandoning generic catalog specifications. Sourcing decisions now center on structural FEA (Finite Element Analysis) load modeling, anti-corrosion chemical formulations, and total-cost-of-ownership (TCO) life cycles.
In high-density industrial hubs across Southeast Asia (such as Singapore, Bangkok, and Jakarta), GCC regions, and North American distribution centers, operational footprint optimization is imperative. Sourcing teams prioritize modularity, vertical cube utilization, and seamless automation interfaces over raw tonnage quotes. Direct procurement from vertically integrated original equipment manufacturers (OEMs) provides verified steel mill traceability, batch-tested yield strengths, and tailored structural engineering compliance.
Q235B & Q355B Metallurgical Integrity
Strict mill certifications guarantee high-tensile hot and cold-rolled coil profiles. High yield strength ensures resistance against plastic deformation under maximum designed capacity (UDL).
Multi-Axis Automated Punching
Continuous CNC roll-forming lines maintain precision pitch adjustments (typically 50mm or 75mm), guaranteeing micro-millimeter tolerance interlocking between upright post holes and welded connector hooks.
Pre-Treatment & Powder Adhesion
A rigorous industrial 10-step pickling, degreasing, and phosphating sequence prevents sub-surface rusting before automatic electrostatic powder deposition and high-temperature curing oven polymerization.
Engineering Evolution: Structural Integration & Automated Logistics
Industrial storage infrastructure is evolving from passive static steel structures into highly responsive, dynamic operational assets. As robotic materials handling systems become ubiquitous, racking factories must meet stringent deflection tolerances under high cyclic stress and acceleration forces.
ASRS & Shuttle Readiness
Tight profile tolerances designed for autonomous 4-way radio shuttles and automated stacker cranes with sensor-accurate guide rails.
Dynamic Seismic Mitigation
Reinforced back-to-back bracing, thickened seismic base plates, and epoxy anchor embeds compliant with regional building codes.
Sub-Zero Cold Chain Design
Specialized low-temperature impact-resistant alloys preventing cryogenic embrittlement down to -30°C in food and biomedical facilities.
Multi-Tier Spatial Stacking
Rack-supported mezzanine frameworks multiplying usable warehouse volume by 200–300% without acquiring additional real estate.
Factory-Direct Capabilities: Guangzhou HEDA Shelves Co., Ltd.
Operating since 2001, Guangzhou Heda Shelves Co., Ltd. is an established manufacturer and exporter of heavy-duty pallet racking, industrial shelving, and multi-tier mezzanines. Our facility features automated CNC roll-forming lines, robotic welding stations, pre-treatment wash systems, and electrostatic powder coating lines.
Certified Structural Compliance
We supply verified documentation, structural loading calculations, and mill certs required by international import bodies, municipal permitting offices, and structural inspection engineers.
- CE Certification No. 2435-CPR-8605159: Factory production control compliant with European structural steel execution requirements.
- ISO 9001:2015 Registered (No. 18624Q00169R0M): Verified continuous quality management protocol from raw coil to final container dispatch.
- RoHS Surface Finish Compliance: Heavy-metal-free, non-toxic thermoset powder polymers suited for food-grade, retail, and pharma hubs.
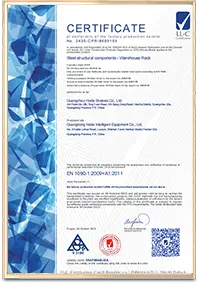 CE Direct Certification
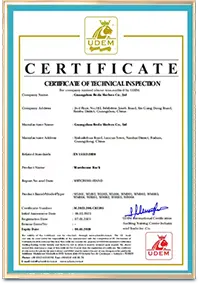 ISO 9001 Quality Control
Integrated 10-Step Quality Control Workflow
01
Raw Steel Test
02
Laser Precision
03
CNC Punching
04
Roll Cold-Form
05
Profile Forming
06
Polishing Clean
07
Robotic Welding
08
Phosphating
09
Powder Coating
10
QC & Packing
Technical FAQ: Procurement & Structural Engineering
How do engineering calculations verify seismic compliance for installations in Asia and the Pacific Rim?
Our engineering team conducts project-specific structural simulations based on local codes (such as Eurocode 3, AS4084, and US RMI guidelines). In seismic regions like the Philippines, Indonesia, and Japan, we model dynamic ground acceleration, enhance upright cross-sectional steel gauges, utilize oversized ductile anchor base plates, and integrate reinforced transverse and vertical X-bracing networks. Calculation reports can be supplied for local permit applications.
What are the primary structural differences between Q235B and Q355B steel in heavy-duty racking applications?
Q235B has a minimum yield point of 235 MPa, making it suitable for standard medium-duty and general pallet racking. Q355B is a low-alloy, high-strength structural steel with a yield threshold of 355 MPa. Using Q355B allows for higher upright column capacities in tall high-bay installations (over 10 meters) and dense automated shuttle systems, resisting axial buckling and seismic sway while optimizing dead load weight.
How does the 10-step surface treatment prevent corrosion in humid or coastal environments?
Untreated steel rapidly forms mill scale and micro-oxidation, which degrades typical coatings. Our automated pre-treatment includes immersion pickling in acid baths to remove mill scale, degreasing, and a zinc-iron phosphating step that creates a crystalline anti-corrosion barrier. Electrostatic powder coating then applies a durable 60–90 micron thermosetting polymer layer. For coastal warehouses, open yards, or cold storage conditions, hot-dip galvanization is also available.
What parameters are required to generate an accurate 2D/3D CAD layout and structural load assessment?
To provide an engineered proposal within 24–48 hours, our team requires: (1) Warehouse architectural drawings showing column locations, overhead truss clearances, floor expansion joints, and fire door clearances; (2) Pallet specifications including overall dimensions (W×D×H) and maximum gross weight; (3) Materials handling equipment (MHE) specs, such as forklift turning radius, mast height, and reach; (4) Total inventory SKU count and daily throughput velocity.
How are export shipments packaged to prevent transit damage and container stuffing losses?
All upright frames and beams are bundled using non-marking PET strapping, separated by shock-absorbing corrugated buffer blocks, and wrapped with waterproof stretch film. Small parts, footplates, safety pins, and anchoring bolts are packed into reinforced, labeled wooden crates. We generate a 3D container loading simulation for every 20GP/40HQ container, ensuring weight distribution meets port limits and optimizing cubic fill to minimize ocean freight costs per pallet location.
Plan Your Next Warehouse Optimization Project
Consult with our engineering team for free 2D/3D CAD design proposals, structural load evaluations, and direct container export pricing from our Guangzhou production facility.
Get Catalog