Export Portfolio: Heavy-Duty Dynamic & Static Racks
Explore our factory-direct industrial storage series manufactured under ISO 9001:2015 and CE standards. From gravity carton flow and high-density pallet flow to heavy fabric stacking and agricultural grow systems, each solution is fully tailored to structural load and material handling profiles.
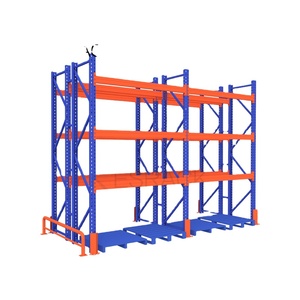
Custom Heavy Duty Industrial Steel Carpet Roll Display Racking
- Deep cantilever & cradle design
- 1,000–3,000 kg capacity/level
- High-yield Q235B cold-rolled steel
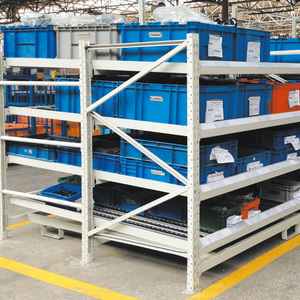
High Density Heavy Duty Pallet Gravity Flow Racking
- Strict FIFO automatic replenishment
- Centrifugal speed controller rollers
- Separator mechanisms at pick faces
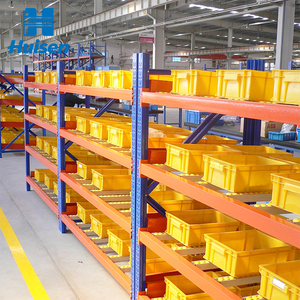
Customized Heavy Duty Industrial Carton Gravity Flow Racks
- Aluminum alloy / sheet metal roller track
- Pick-to-light (PTL) brackets ready
- Ergonomic tilted discharge trays
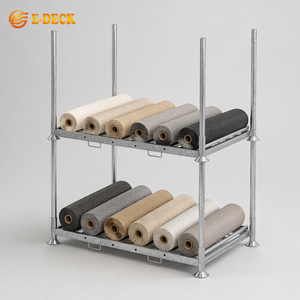
Detachable Industrial Fabric Roll Galvanized Stacking Pallet Racks
- Demountable post configuration
- 4-tier stacking with anti-sway cups
- Hot-dip galvanized anti-corrosion
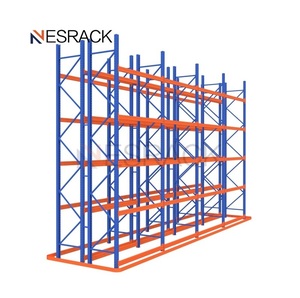
High Bay Selective Pallet Racks with VNA Floor Guide Rails
- Heights up to 15m structural uprights
- 100% direct access to individual SKUs
- Heavy welded baseplates & expansion bolts
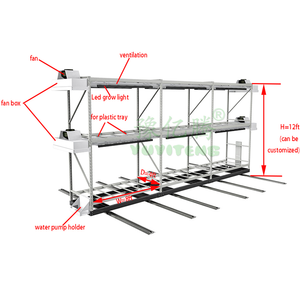
Multi-Tier Hydroponics Vertical Grow Rack for Indoor Agriculture
- 4ft x 8ft standardized bay geometry
- Integrated drainage & LED channels
- Anti-bacterial humidity resistant coating
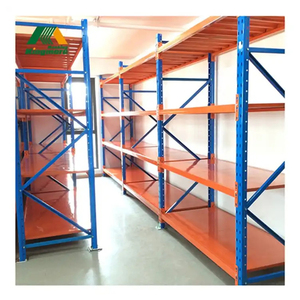
CE Certified Heavy Duty Bolted Industrial Selective Pallet Racks
- EN 15512 & CE No. 2435-CPR compliant
- Pitch 50mm/75mm adjustable connector claws
- Safe working loads up to 4,500 kg/tier
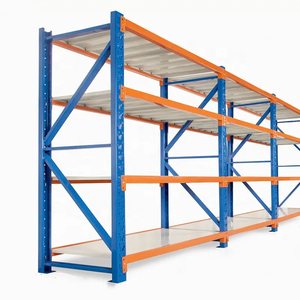
Stacking Long Span Metal Storage Shelving & Picking Racks
- Fast boltless assembly interlocking lugs
- Steel panel / wire mesh / chipboard decking
- 300–800 kg per shelf distributed capacity
Technical Deep-Dive: Carton Flow Racking Architecture
Carton flow systems (also referred to as gravity flow shelving) convert warehouse square footage into high-velocity, high-density fulfillment zones. By utilizing inclined gravity roller beds, carton flow separates stocking activities from picking zones, ensuring an uninterrupted First-In, First-Out (FIFO) material progression.
Gravity Wheel Beds vs. Full-Width Rollers
Modern carton flow utilizes either high-impact polycarbonate skate wheels mounted in staggered patterns or full-width galvanized steel roller tracks. While skate-wheel beds accommodate irregular carton footprints and variable carton widths without re-tracking, full-width steel rollers offer superior durability for heavy plastic containers (totes) weighing up to 50 kg per unit.
Pitch Angle & Centrifugal Braking
Optimal lane inclination typically ranges between 2.5° and 4.5° (approximately 40mm to 65mm pitch drop per linear meter). For extended lane runs surpassing 6 meters, HEDA incorporates polyurethane brake wheels and entry impact plates to prevent carton acceleration, load crush, and rebound bouncing at the pick face.
Ergonomic Tray & Pick-to-Light Synergy
Discharge points are configured with 5° to 15° knuckle trays (drop tilt shelves) presenting carton contents directly into the picker's field of vision. Pre-drilled beam profiles accommodate plug-and-play bracket integration for digital pick-to-light (PTL) sensor arrays, cutting travel distance by up to 75% compared to static long-span shelves.
| Carton Flow Component | Material Specification | Load / Functional Rating | Operational Advantage |
|---|---|---|---|
| Track Side Channels | 1.2mm–1.5mm Cold-Rolled Galvanized Steel | Torsional rigidity up to 250 kg/m span | Resists lateral warping under sudden impacts |
| Skate Wheels / Rollers | Virgin High-Impact Polyethylene / ABS / Steel | 10–35 kg dynamic load per wheel | Low-friction starting resistance (<0.05 coefficient) |
| Upright Frames | Q235B High-Tensile Steel, 50mm Pitch Punch | Up to 15,000 kg frame capacity | Accommodates multi-tier picking mezzanines |
| Lane Dividers | Extruded Aluminum / Galvanized Sheet Wire | Full depth tool-free snap-in adjustment | Prevents lane migration and cross-line jam |
| Pick Trays (Knuckle) | 2.0mm Electrostatic Powder-Coated Steel | Adjustable tilt (0°, 5°, 10°, 15°) | Eliminates picker wrist strain and lumbar fatigue |
Future Procurement Trends for Carton Flow Systems (2025–2030)
Procuring carton flow systems is shifting from simple catalog ordering to total system integration. Procurement directors in North America, Europe, Southeast Asia, and the Middle East are evaluating manufacturers based on modularity, hybrid automation compatibility, and life-cycle sustainability.
1. Hybrid AMR & AGV Integration
Carton flow racks are no longer standalone manual racking blocks. Tier-1 exporters now pre-engineer discharge faces with specialized docking heights for Autonomous Mobile Robots (AMRs) and automatic tote loaders. Gravity lanes act as zero-energy buffer stations connecting automated case-handling bots with human pickers.
2. Rapid Retooling & Micro-Fulfillment
E-commerce SKU churn demands rapid lane adjustments without shut-down windows. Tool-less drop-in track clips, magnetic SKU status flags, and modular lane partitions allow warehouse crews to reconfigure a 40-lane bay in less than 30 minutes to match promotional sales spikes and seasonal catalog swaps.
3. Circular Steel Sourcing & Low-Carbon Coating
International environmental mandates (including EU CBAM and RoHS) demand transparent carbon metrics in cold-formed structural steel. Exporters are shifting to phosphate-free silane pretreatment and lead-free thermoset powder coatings that yield ultra-low VOC emissions while maintaining salt-spray corrosion resistance up to 500 hours.
Industrial & Technological Trends Shaping Dynamic Storage
Dynamic carton flow storage is evolving from a passive mechanical system into an intelligent, data-driven node within modern distribution centers. Consider these primary technical advancements changing warehouse footprints globally.
Integrated IoT Weight Sensors
Pressure transducers embedded into roller tracks detect carton presence and calculate remaining stock weight in real time. This triggers automated ERP restock alerts before a channel completely starves.
Multi-Tier Mezzanine Integration
By nesting carton flow shelves directly beneath high-bay pallet racking or incorporating them inside 3-to-4-tier rack-supported mezzanines, facilities double or triple pick-face density without increasing floor footprint.
Seismic-Resistant Beam Locking
Advanced Chinese exporters now employ cold-stamped 4-claw and 5-claw beam connectors coupled with high-shear safety pins, meeting stringent EN 15512 and seismic codes for earthquake-prone zones across the Pacific Rim.
Cold Chain Thermal Polycarbonate
Specialized low-temperature roller compounds prevent cracking and brittle fracture in blast freezers and refrigerated distribution centers down to -30°C, maintaining silent carton glide without lubricant freeze.
Why Choose Guangzhou Heda Shelves Co., Ltd.?
Founded in 2001, Guangzhou Heda Shelves Co., Ltd. operates a state-of-the-art 30,000 m² manufacturing plant equipped with automated roll-forming lines, robotic CNC beam welding, and a continuous pickling-phosphating powder coating line. We supply factory-direct industrial storage solutions to contractors, system integrators, and distributors in over 120 countries.
25+ Years Manufacturing Heritage
Over two decades of dedication to warehouse racking, industrial shelving, and multi-tier mezzanine engineering with more than 10,000 turnkey projects delivered worldwide.
Certified International Quality
Full compliance with European CE Certification (No. 2435-CPR-8605159), ISO 9001:2015 Quality Management (No. 18624Q00169R0M), and lead-free RoHS surface finish standards.
Rapid 24–48h 2D & 3D Engineering
Our dedicated engineering department delivers custom 2D AutoCAD layouts, high-resolution 3D operational renders, and structural load calculations within 24 to 48 hours free of charge.
Pickling & Phosphating Pre-Treatment
Unlike budget workshops that spray over mill scale, our 10-step surface finishing features acid pickling and immersion phosphating, guaranteeing maximum powder adhesion and anti-rust durability.
Container Optimization & Global Port Access
Direct proximity to South China shipping hubs (Guangzhou, Shenzhen, Hong Kong) allows streamlined sea freight routing, precise 3D container packing layouts, and significant logistics cost reduction.
OEM & ODM Private Label Supply
Full support for overseas distributors and system integrators, including custom upright color matching (RAL codes), proprietary connector hole stamping, and customized packaging.
Frequently Asked Questions (FAQ) for B2B Importers
Find factual, engineering-backed answers addressing the most common design, compliance, shipping, and installation concerns encountered when sourcing carton flow racks from China.