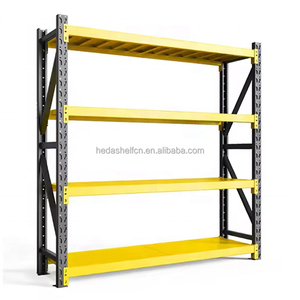
Wholesale Price Industrial Boltless Storage Rack 4 Tier Shelving
Modular boltless interlocking design engineered for rapid warehouse maintenance and medium-to-heavy manual loading profiles up to 800kg/tier.
Get a QuoteExplore our CE-certified heavy-duty industrial racking configurations. Each rack unit is precision roll-formed from premium certified structural steel coil, phosphated, and powder-coated to deliver optimal operational throughput.
Modular boltless interlocking design engineered for rapid warehouse maintenance and medium-to-heavy manual loading profiles up to 800kg/tier.
Get a Quote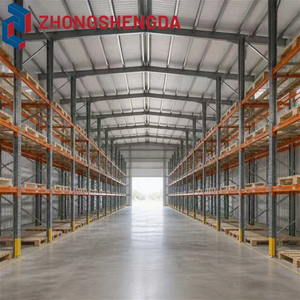
Designed for 3PL central fulfillment centers with structural steel galvanized uprights ensuring complete structural resilience and seismic protection.
Get a Quote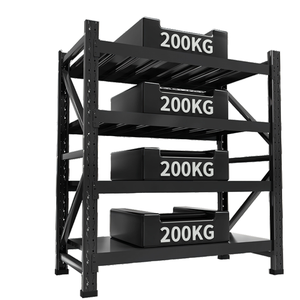
Versatile long-span layout engineered for retail staging, archive operations, and micro-fulfillment hubs requiring reconfigurable vertical levels.
Get a Quote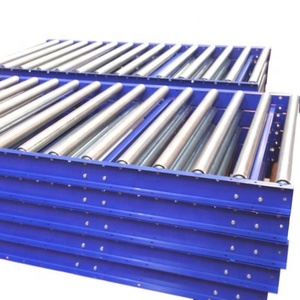
First-In-First-Out (FIFO) gravity roller racking with precision speed controllers, engineered for cold chains and fast-moving consumer goods.
Get a Quote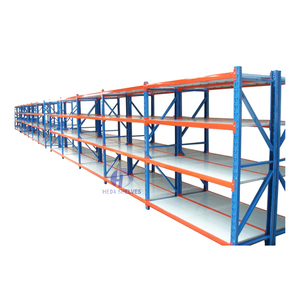
Modular industrial steel storage unit featuring double-slotted uprights and high-tensile connection hooks for flexible bulk consolidation.
Get a Quote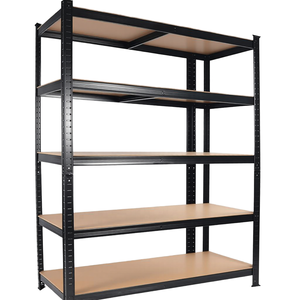
Equipped with pallet support bars and rigid guide channels, offering extreme vertical stack stability for variable heavy warehouse inventory.
Get a Quote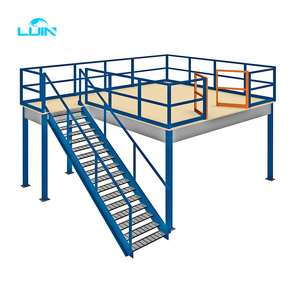
Engineered structural steel platform doubling floor surface area, designed to carry up to 1,000kg/m² with integrated staircases and pallet gates.
Get a Quote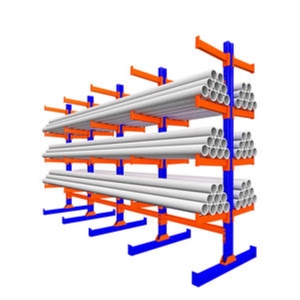
Freestanding multi-layer heavy load cantilever system optimized for non-standard, long profile inventory including steel pipes, rebar, and timber.
Get a QuoteGlobal supply chains are migrating toward lean capital deployment, certified structural integrity, and long-term space utilization. Modern procurement teams prioritize these key considerations before issuing tenders.
Procurement directors are shifting away from cheap, thin-gauge racking. Factoring in deflection ratings, floor anchor integrity, upright damage resistance, and cold-formed profile longevity demonstrates that certified, high-grade steel structures reduce replacement downtime by over 62% across a ten-year operational life cycle.
Industrial real estate rents have risen sharply across global supply hubs. Modern facilities are retrofitting standard selective racks with Drive-In, Push-Back, and Shuttle systems to push floor utilization rates from 40% up to an industry-leading 80%, substantially reducing the chilled footprint required per cubic meter stored.
Independent third-party validation is non-negotiable for Tier-1 supply operations. Verified mill certificates, CE machinery & construction credentials (EN 1090 / 2435-CPR-8605159), ISO 9001:2015 tracking, and seismic simulation models guarantee project approvals from regulatory bodies and insurers.
From robotic welding lines to intelligent sensor retrofits and semi-automated shuttle conversions, drive-in systems are evolving to match next-generation material handling requirements.
Traditional drive-in racking required manual forklift operators to enter narrow lanes, creating risk of structural collisions. Advanced systems now incorporate structural floor guide tracks and laser-guided automated guided vehicle (AGV) docking channels, eliminating human error while accelerating pallet transit speeds.
Rapid thermal cycles inside sub-zero (-30°C) automated cold rooms degrade conventional coatings. Contemporary engineering employs specialized pickling, phosphating, and electrostatic epoxy coating formulations—alongside fully hot-dip galvanized upright alternatives—to prevent embrittlement and micro-fissuring.
Forward-thinking warehouse operators specify drive-in upright frame patterns that readily convert to semi-automated Radio Shuttle operations. By installing universal pallet runner profiles, businesses can transition from manual lift truck entries to shuttle automation with zero beam replacement.
Key engineering, structural, and logistics details answered by our industrial design team to streamline your project evaluation.
CE certification (Certificate No. 2435-CPR-8605159) confirms that structural calculations, raw steel tensile tolerances, and manufacturing weld integrity meet European EN 15512 and EN 1090 standards. This guarantees stated load ratings under maximum capacity, operational sway resistance, and full compliance for municipal safety audits and insurance coverage.
Standard selective racking requires a working forklift aisle for every two rows of pallets, sacrificing up to 60% of floor area purely to vehicle circulation. Drive-In racking consolidates pallets on continuous cantilevered rails, eliminating interior aisles to double or triple pallet density for homogeneous SKUs.
Because forklifts enter the rack channels, robust safety additions are essential. We engineer reinforced wrap-around column protectors, floor-anchored steel guide rails (chamfered at entrance points), and heavy-duty portal top bracing to distribute kinetic forces away from upright columns.
Yes. Our engineering department uses Finite Element Analysis (FEA) to model project-specific seismic spectra (PGA) for active zones such as the Pacific Rim and Middle Eastern fault regions. Upright profiles, gauge thicknesses, baseplate footprints, and mechanical anchor embedments are custom calculated to prevent catastrophic failure.
We require the clear internal warehouse height, column spacing grid, architectural layout (CAD or dimensioned drawing), detailed pallet dimensions (including overhang and load weight), forklift model specifications (turning radius, mast collapsed height, lift height), and target SKU batch profiles.
Components pass through an automated 10-stage preparation sequence featuring intensive acid pickling and zinc-iron phosphating prior to electrostatic powder coating. This prevents oxidation creeping beneath the paint. For coastal or sub-zero facilities, full hot-dip galvanization is available.
Over 25 years of specialized storage manufacturing, operating from our 30,000m² plant in Guangzhou to deliver reliable turn-key warehousing worldwide.
All operations are managed in-house—precision roll-forming, automated multi-point punching, robotic welding, pre-treatment washing, and electrostatic coating. Maintaining production under one roof delivers exact dimensional accuracy and uniform structural performance.
Certified to CE standard (No. 2435-CPR-8605159), ISO 9001:2015 quality standards (No. 18624Q00169R0M), and RoHS environmental standards. Complete material mill test reports and structural calculations accompany project shipments for seamless local code compliance.
With more than 10,000 completed facilities in over 120 countries, our multilingual engineering team prepares CAD plans and 3D renderings within 24 to 48 hours. Our export logistics team optimizes container cube utilization to lower ocean freight costs per pallet position.
Connect with our senior engineering team to receive a free, comprehensive CAD layout, 3D structural model, and custom load verification tailored to your warehouse dimensions.
Get a Quote