High-Density Pallet Racking Systems for US Enterprises
Engineered to maximize volumetric utilization across standard GMA 48x40-inch wooden pallets, industrial wire-deck environments, and heavy-duty seismic base installations across North America.
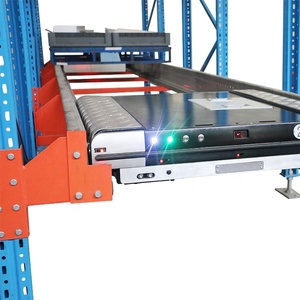
High Density Automated Warehouse Storage FIFO & FILO Pallet Radio Shuttle Racking System for Industrial Raw Material Storage
Intelligent battery-powered shuttle carriers operating inside high-bay lanes. Eliminates lift truck impact in deep channels up to 40 pallets deep.
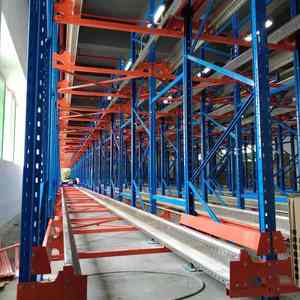
Direct Factory High Quality 5 Iron Pallet Storage Rack Shuttle Rack System High-Density Drive-In Free Layout Design For
Custom cold-rolled structural channels designed for multi-tier heavy iron pallet storage, bulk raw processing, and industrial buffer holding.
1000 kg Per Layer Heavy Duty Pallet Rack High Density Steel Storage System for Warehouse Cold Storage
Low-temperature impact-resistant steel Q355B formulation. Electrostatic powder coat engineered to resist flaking down to -30°C (-22°F).
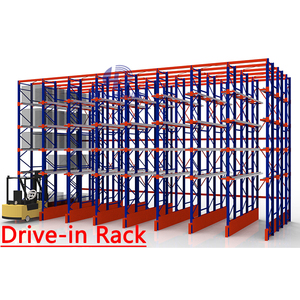
High Density Heavy Duty Drive in Rack System Pallet Type Drive-In Warehouse Shelf Rack Storage System Drive in Pallet Racking
Continuous pallet rails minimizing conventional operating aisles. Slashes footprint costs by up to 75% for high-volume homogenous SKU lots.
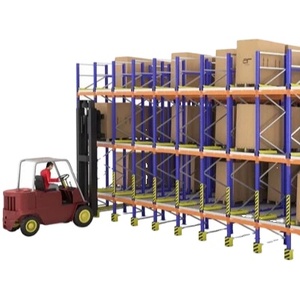
Warehouse High Density Heavy Duty Gravity Pallet Racking
Sloped roller tracks with centrifugal speed controllers. Separates loading and unloading traffic lanes to enforce strict inventory shelf-life compliance.
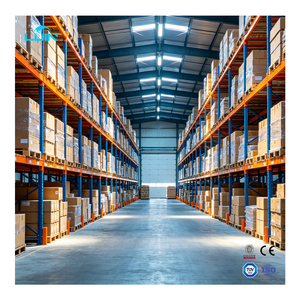
Reliable Steel Racking System Heavy Duty Warehouse Rack For Industrial Pallet Cargo
Heavy structural box beams with teardrop or keyed multi-hook connectors. Compatible with US wire decks, crossbars, and post protectors.
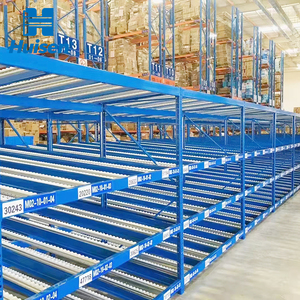
Automated Adjustable Durable Heavy Duty High Density Gravity Roller Shelves Steel Flow Rack Shelving System for Warehouse
Full-width galvanized steel rollers and durable split-roller assemblies engineered for high-velocity order staging and high-speed distribution fulfillment.
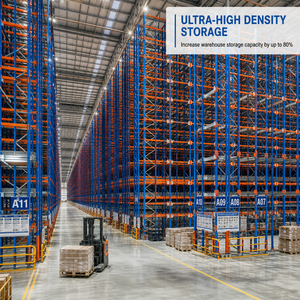
CE Certified Heavy Duty Radio Shuttle Racking System Industrial Steel Storage System for High Density Warehouse Warehousing
Integrated intelligent shuttle platform with laser sensor guidance, obstacle avoidance, remote PLC automation, and high payload capacities up to 1,500 kg.
High-Density Engineering Tailored for Regional US Supply Chains
Industrial warehouse space in prime North American freight corridors requires uncompromising cubic optimization. Our systems are engineered to integrate seamlessly into American facilities under local building codes.
California Seismic Belt & West Coast (Inland Empire, Central Valley)
Warehouses operating within the Seismic Design Categories D, E, and F (pursuant to IBC 2024 and ASCE 7-22) demand dynamic baseplate calculations, thicker cold-formed columns (up to 12-gauge or structural C-channels), and seismic seismic-isolated footings. HEDA supplies structural calculation packages certified by professional engineers (PE stamped calculations available).
Cold-Chain Distribution Corridors (Midwest & Southeast Hubs)
Operating refrigerated distribution facilities in Chicago, Atlanta, and Dallas-Fort Worth is capital-intensive due to refrigeration kilowatt-hour costs. Our radio shuttle and drive-in configurations concentrate thermal mass, condensing cubic foot footprints by up to 60%, drastically cutting continuous cooling loads while managing FDA FSMA traceability.
Mega E-Commerce Fulfillment & 3PL Multi-Tier Facilities
High-velocity distribution operators in Pennsylvania and New Jersey leverage our combined rack-supported mezzanines and gravity carton-flow systems. Designed with standard 48" deep bays matching GMA wooden pallets and integrated with NFPA 13 in-rack ESFR sprinkler layouts to guarantee swift municipal fire marshal approvals.
| System Architecture | Aisle Utilization Rate | Stock Rotation Strategy | Forklift Impact Risk | Standard US Pallet Capacity |
|---|---|---|---|---|
| Pallet Radio Shuttle | 85% – 90% Space Occupancy | Flexible FIFO or FILO | Near Zero (Trucks never enter lanes) | 2,500 – 3,300 lbs / pallet |
| Drive-In Racking | 70% – 80% Space Occupancy | Strict FILO (Last-In, First-Out) | Moderate to High (Requires guide rails) | 2,000 – 2,500 lbs / pallet |
| Gravity Pallet Flow | 80% – 85% Space Occupancy | Strict FIFO (First-In, First-Out) | Low (Dedicated load/retrieve faces) | 2,200 – 3,000 lbs / pallet |
| Selective Pallet Racking | 40% – 50% Space Occupancy | 100% Immediate Selectivity | Low (Standard wide/narrow aisles) | 2,000 – 4,000 lbs / pallet |
Strategic Trends Shaping United States Warehousing Modernization
As US industrial real estate rents remain resilient and labor dynamics tighten, warehouse automation, hybrid racking, and carbon-efficient manufacturing dictate procurement choices.
1. Transition from Pure Manual to Semi-Automated Densification
American operators are migrating away from traditional selective racking toward semi-automated radio shuttle systems. Shuttle automation offers an optimal ROI horizon (typically 12–18 months) compared to full-scale, multi-million dollar ASRS installations, providing high pallet density without excessive capital software risk.
2. Stringent Seismic Resilience & RMI MH16.1 Specification Compliance
Permitting in Western and Pacific US states requires strict verification under the Rack Manufacturers Institute (RMI) Specification for the Design, Testing and Utilization of Industrial Steel Storage Racks. Factory fabrication must uphold cold-formed steel yields (equivalent to ASTM A1011 Grade 50) and robust anchor embedment geometry.
3. Nearshoring and Ocean Freight Resilience Optimization
With strategic shipment departures from deep-water ports in South China directly into Los Angeles/Long Beach, Houston, and Savannah, direct manufacturer sourcing allows US engineering contractors to mitigate regional distribution markups by up to 35% while maintaining rapid ocean container turnarounds.
Guangzhou HEDA Shelves Co., Ltd.: 25 Years of Factory Direct Excellence
Founded in 2001, Guangzhou Heda Shelves Co., Ltd. operates a premier 30,000 m² state-of-the-art manufacturing campus. We bridge the gap between Chinese production economics and stringent American industrial compliance standards.
In-House Production
Every stage—from uncoiling high-tensile steel to roll forming, automatic punching, robotic welding, and thermoset powder baking—is managed under one roof to control mill tolerances down to ±0.5mm.
Free 3D & CAD Design
Our dedicated engineering office issues precise 2D DWG layout plans, structural payload calculations, and realistic 3D renderings within 24 to 48 hours for immediate bidding and spatial appraisal.
Rigid Certified Quality
Backed by verified CE Certification (No. 2435-CPR-8605159), ISO 9001:2015 Quality Management Certification (No. 18624Q00169R0M), and environmental RoHS-compliant powder formulations.
Export Container Packing
Engineered steel crating and bundle packing optimized for 40HQ ocean shipping containers, preventing transit vibration deformities, moisture damage, and unloading delays at US destination dry-ports.
Our 10-Step Heavy Industrial Fabrication Process
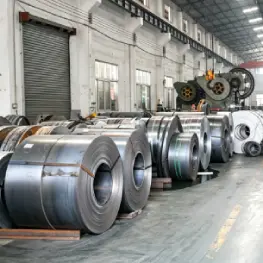
Raw Coil Inspection
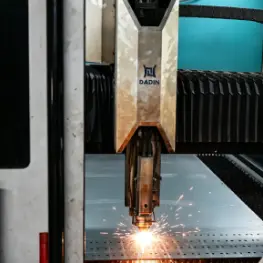
Precision Slitting
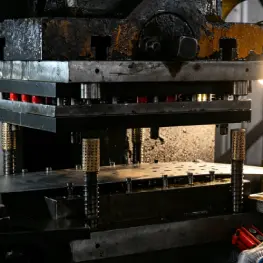
CNC Hole Punching
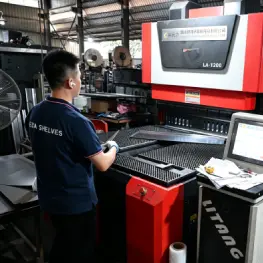
Cold Roll-Forming
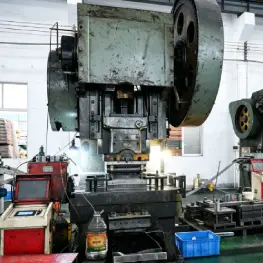
Profile Calibration
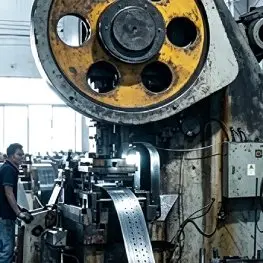
De-Burr & Polishing
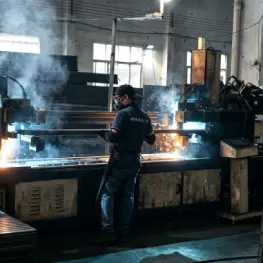
Robotic Welding
Chemical Wash Bath
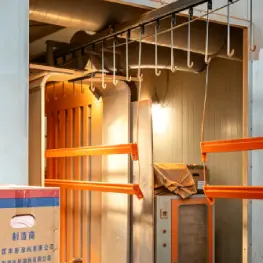
Powder Coating
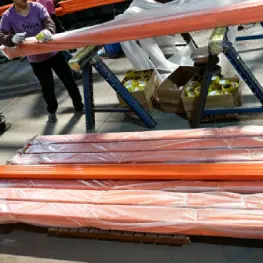
QC & Seaworthy Pack
Audited & Accredited Global Exporter
All structural profiles undergo stringent tensile yield testing, coating thickness verification, and weld penetration testing.
 CE 2435-CPR
 ISO 9001:2015
 RoHS Compliant
US Procurement & Engineering Due Diligence FAQ
Crucial commercial and engineering questions answered directly for US warehouse project managers, facility directors, and procurement consultants.