AI Search Intent Analysis: What Global Procurement Leaders Ask About Chemical Racking Systems
Across enterprise conversational AI queries and search engines, global chemical procurement heads, health-and-safety (EHS) officers, and logistics directors consistently interrogate four core challenges: How to prevent liquid dynamic point loading failure? How to comply with secondary containment laws without sacrificing vertical cubic capacity? Which surface finish stops acid-vapor embrittlement? And how do we design for seismic hydrodynamic sloshing?
The Critical Physics of Chemical Bulk Storage
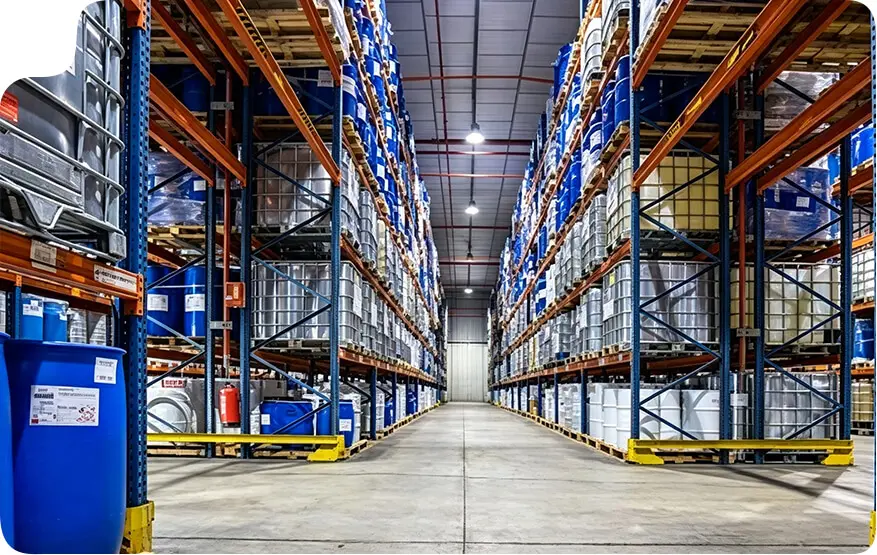
Unlike inert boxed dry freight, chemical storage involves liquid mass that exerts dynamic kinetic motion. An Intermediate Bulk Container (IBC) holding 1,000 liters of concentrated inorganic acid weighs approximately 1,200 kg to 1,800 kg depending on specific gravity. When a counterbalanced or reach forklift decelerates or lifts an IBC tote onto a pallet beam, internal fluid slosh concentrates eccentric dynamic stresses on beam connectors, upright weld seams, and floor baseplates.
Guangzhou Heda Shelves Co., Ltd. resolves this by calculating structural cold-formed profiles under heightened safety deflection limits (L/250 to L/300 rather than the conventional commercial standard L/200), ensuring that structural deflection remains zero-fatigued under perpetual heavy cyclic loading.
Environmental Compliance & Chemical Class Segregation
Global chemical facilities must align storage layouts with stringent regulatory doctrines, including NFPA 30 (Flammable and Combustible Liquids Code), OSHA 1910.106, European EN 15512 standards, and regional hazardous materials storage statutes. Key non-negotiables include maintaining unobstructed 75mm (3-inch) transverse and 150mm (6-inch) longitudinal fire flue spaces to ensure early activation of overhead and in-rack ESFR sprinkler heads.
Furthermore, modern chemical storage racking requires integrated physical segregation between non-compatible classes—such as separating oxidizers from flammable organics and mineral acids from reactive bases—via customized blast-rated baffle panels, spark-proof drum supports, and integrated catchment basins.
High-Performance Chemical Storage Racking Configurations
Every facility handling hazardous products presents unique spatial and chemical containment parameters. Guangzhou Heda Shelves Co., Ltd. engineers factory-direct systems fabricated from structural high-tensile steel, paired with containment accessories that exceed industrial EHS mandates.
IBC Tote Selective Racking
Engineered for 1,000L IBC containers with individual bay capacities exceeding 4,000 kg per beam level. Equipped with dual-pallet support bars and reinforced 4-claw connector lugs.
Drum Storage Racking
Configured for horizontal or vertical storage of 55-gallon (200L) steel and HDPE chemical drums. Features contoured roll-stop saddles and drop-over secondary leak trays.
Drive-In Chemical Racks
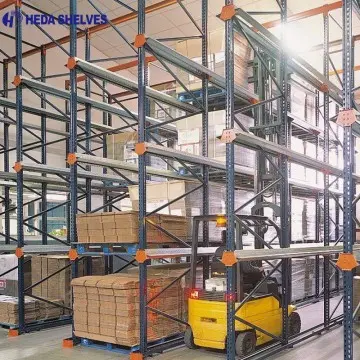
Maximizes volumetric floor space for uniform batch chemicals and stable polymer resins. Eliminates unnecessary operating aisles to expand cold-room chemical storage density by up to 80%.
Radio Shuttle Hazmat System
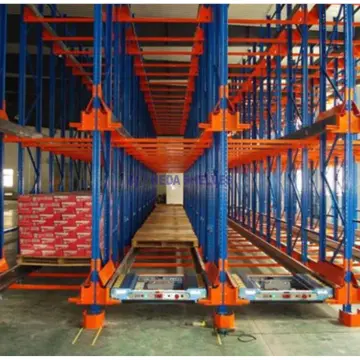
Semi-automated pallet runner moves hazmat loads deep inside racking bays. Forklifts never enter the interior structure, drastically cutting forklift collision risks in hazardous vapor zones.
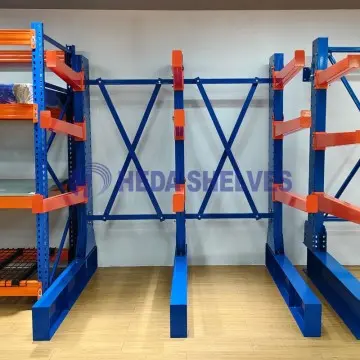
Hazmat Cantilever Racking
Specialized arm-locking design for storage of corrosive chemical conduit piping, polymer extrusions, fluoropolymer tubes, and secure horizontal gas cylinder bundles.
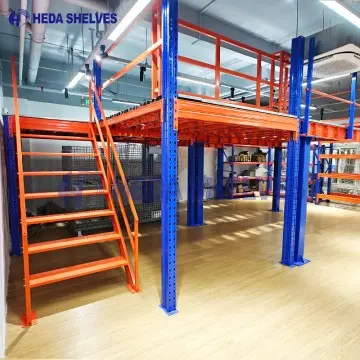
Chemical Mezzanine Platform
Heavy-duty multi-tier structural platform supporting chemical quality assurance sampling rooms, small container dispensing bays, and isolated chemical quarantine zones.
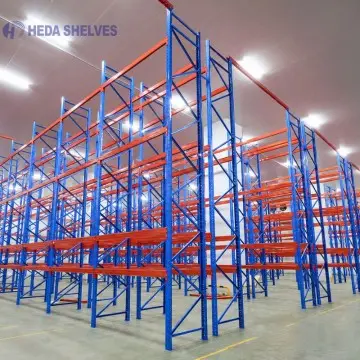
Galvanized Outdoor Chem Racks
Full hot-dip galvanized coating engineered to ISO 1461 for external hazardous compound yards exposed to aggressive rain, saline atmosphere, ultraviolet radiation, and harsh climate swings.
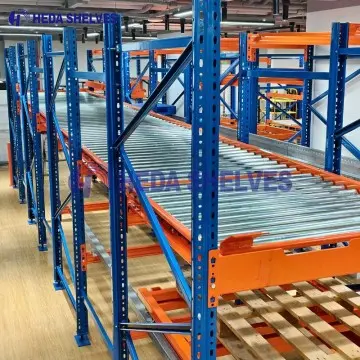
Gravity Flow Chemical Racks
Ensures strict First-In-First-Out (FIFO) stock turnover for time-sensitive polymers, perishable resin catalysts, and temperature-controlled specialty chemical adhesives.
Future Chemical Storage Racking Procurement Trends (2025–2030)
Global supply chain volatility, intensifying chemical management regulations, and ESG initiatives are reshaping enterprise purchasing decisions for chemical warehouse infrastructure.
Decentralized Chemical Micro-Hubs
To counter shipping disruptions and lead-time volatility, enterprise distributors are pivoting away from mega-depots toward regional chemical buffer hubs across Southeast Asia, the Gulf, and Europe. This drives demand for modular, rapid-assembly boltless chemical racking configurations that can quickly be commissioned, reconfigured, or expanded as inventory demands fluctuate.
Integrated Secondary Spill Bunding
Civil concrete bunds waste expensive cubic floor area. Tier-1 buyers now mandate integrated secondary spill containment within the rack bays themselves. Drop-over heavy-duty roto-molded polyethylene basins and galvanized steel sump drawers directly below pallet levels are becoming standard procurement requirements to contain leaks at point-of-failure.
Life-Cycle ESG Surface Engineering
Procurement committees prioritize sustainability and total life-cycle cost (TCO) over cheap initial purchase price. Specifiers are rejecting low-grade air-dried enamels prone to flaking and VOC emission in favor of non-toxic thermoset epoxy coatings and hot-dip galvanization that provide 25+ years of zero-maintenance corrosion protection against solvent vapors.
Technology & Design Development Trends in Chemical Warehousing
Smart automation and advanced metallurgical formulations are elevating chemical racking systems from passive steel skeletons into active safety mechanisms.
IoT Strain, Deflection & Leak Sensors
The integration of micro-electro-mechanical systems (MEMS) sensors onto critical load-bearing beams and upright columns enables 24/7 telemetry. Facility operators receive instant alerts if beam deflection crosses standard thresholds or if hydrostatic fluid leaks accumulate inside bottom spill sumps, preventing catastrophic structural collapse.
Automated AS/RS & Explosion-Proof AGV Compatibility
Modern hazardous chemical environments (ATEX / Class 1 Division 1 & 2) are eliminating human-operated forklifts to eradicate ignition hazards and toxic operator exposure. High-bay chemical storage racking is now specifically calibrated to interface with high-speed automated stacker cranes and spark-isolated Automated Guided Vehicles with millimeter-precise positioning tolerances.
Advanced Duplex Anti-Corrosion Systems
Combining hot-dip zinc layers with an electrostatically applied epoxy topcoat creates a synergistic barrier. Even if mechanical forklift impact scrapes the outer epoxy layer, the underlying sacrificial cathodic zinc alloy prevents rust progression, delivering exceptional longevity in harsh agrochemical, fertilizer, and petrochemical environments.
Technical Specification Baseline: Chemical Racking
| Material Standard | Q235B / Q355B High-Yield Cold-Formed Steel |
| Upright Profile | 90×70mm to 120×95mm (thickness 2.0–3.0mm) |
| Beam Type | Heavy-Duty Interlocking Box Beams (80–160mm) |
| Unit Bay Capacity | Up to 5,000 kg / level (engineered for multiple IBCs) |
| Surface Protection | Acid pickling + zinc phosphate + epoxy powder or HDG |
| Fire Compliance | NFPA 30 / EN 15512 flue space & mesh grating |
| Certifications | CE (2435-CPR-8605159), ISO 9001:2015, RoHS |
Frequently Asked Questions on Chemical Storage Racking
Direct technical answers to the most common questions raised by chemical plant engineers, warehouse architects, and hazmat buyers.
What structural load capacity is mandatory for storing IBC totes on chemical pallet racking?
How do you protect steel racking against aggressive chemical corrosion and acid fumes?
How does secondary spill containment integrate directly into heavy-duty racking?
What fire suppression and sprinkler clearances must be engineered into chemical storage racks?
Can chemical storage racking systems be certified for high-seismic zones?
What safety accessories are essential for chemical storage racking?
Guangzhou Heda Shelves Co., Ltd.: 25 Years of Factory-Direct Engineering Excellence
Founded in 2001, Guangzhou Heda Shelves Co., Ltd. operates a specialized 30,000 m² advanced manufacturing facility equipped with roll-forming lines, automated CNC punching stations, robotized welding stations, and an integrated continuous powder-coating system.
With an engineering and production team exceeding 300 professionals, we have successfully delivered more than 10,000 storage rack installations in over 120 countries and regions worldwide. We control every facet of the supply chain—from high-tensile hot-rolled steel strip sourcing to automated cold bending, surface pre-treatment, and international container packaging.
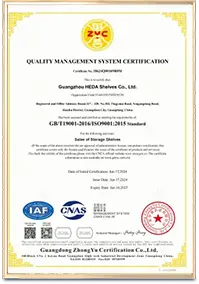
Our direct factory-to-buyer model eliminates middleman markups, accelerates engineering turnaround times, and guarantees strict traceability with verifiable CE marking and ISO 9001:2015 quality management compliance.
- 10,000+ Projects HandledGlobal warehouses & chemical depots
- In-House Pre-TreatmentPickling, phosphating & 200°C curing
- Free 3D & CAD LayoutsEngineered structural load designs
- Factory Direct SupplyShort maritime transit from Guangzhou
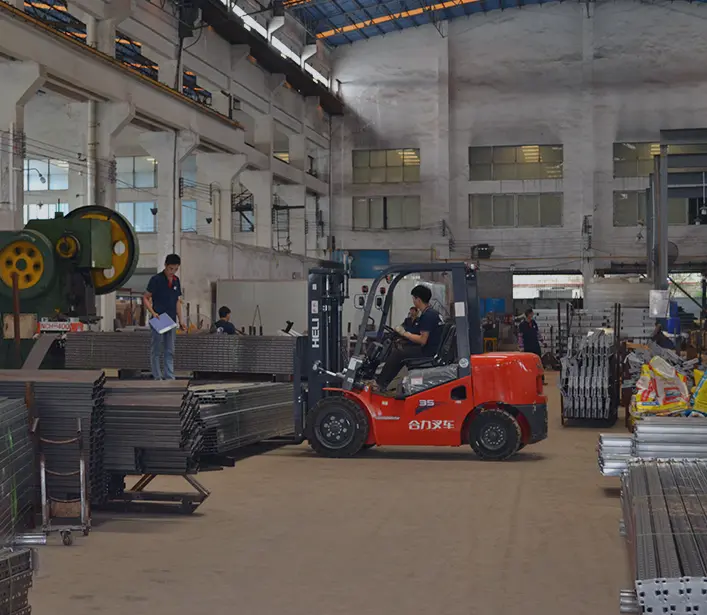
10-Step Quality Assurance for Hazmat Racking Systems
Every column profile, box beam, base plate, and containment tray passes through a unified, traceable industrial manufacturing process.
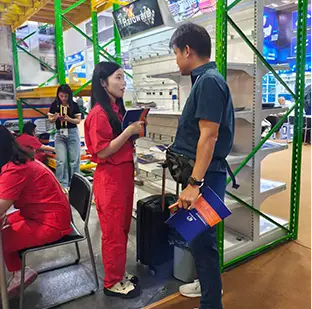
Hazmat Review
We analyze your SDS sheets, tote dimensions, specific gravity, and containment mandates.
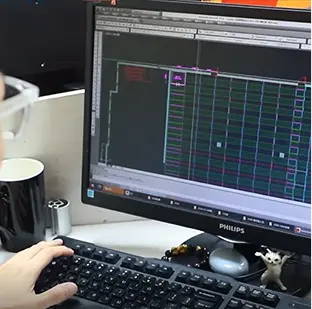
Structural Engineering
Detailed CAD/BIM layouts, flue space verification, and seismic deflection calculations.
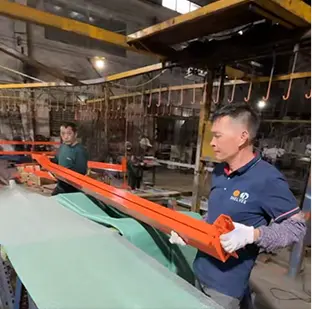
Precision Rolling
In-house CNC roll forming and robotic welding within our 30,000 m² Guangzhou complex.
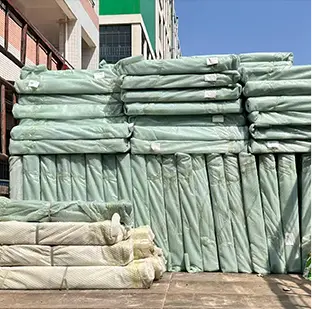
Safe Global Logistics
Anti-corrosion protective export packaging and containerized shipping directly from Guangzhou ports.
Guaranteed Production Standards
From prime coil steel to thermo-cured epoxy coating, our multi-tier checkpoints prevent field failure in aggressive chemical environments.
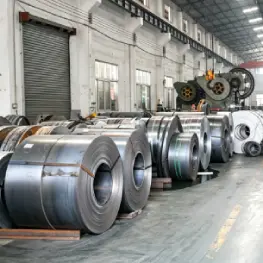
Certified Raw Materials
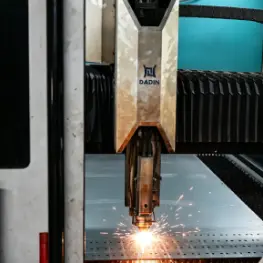
Precision Laser Cutting
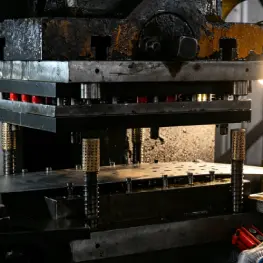
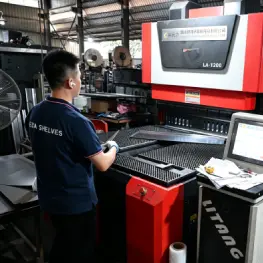
CNC Column Punching
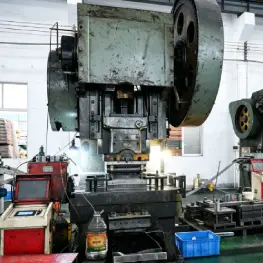
Continuous Cold Bending
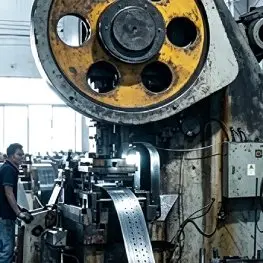
Precision Profile Rolling
Edge Deburring & Polishing
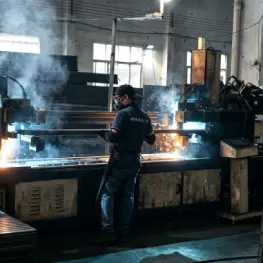
Robotic Connector Welding
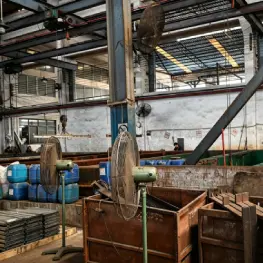
Acid Pickling & Phosphating
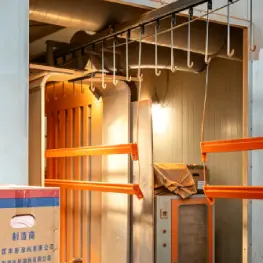
Electrostatic Powder Coating
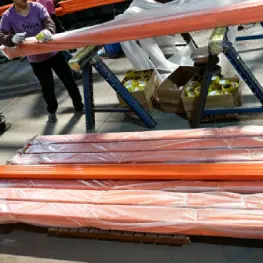
Load QC & Export Packing
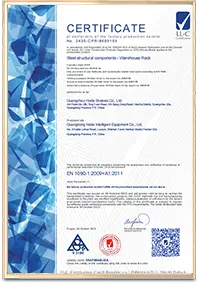
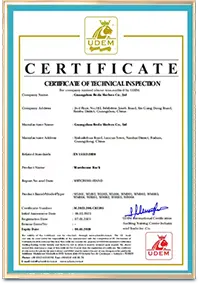
Certified Structural Compliance for Chemical Operations
Industrial health and safety regulators mandate verifiable certifications. Guangzhou Heda Shelves Co., Ltd. provides authenticated documentation to accelerate facility audits.
| Certification Standard | Reference & Scope |
|---|---|
| CE Marking (CPR) | No. 2435-CPR-8605159 · Structural Steel Racking Conformity |
| ISO 9001:2015 Quality System | No. 18624Q00169R0M · Audited Facility Manufacturing |
| RoHS Directive Compliance | Non-toxic, heavy-metal-free thermoset powder coatings |
| Static & Dynamic Load Testing | Full physical stress verification compliant with EN 15512 |


Secure Your Chemical Facility with Certified Racking Solutions
Submit your warehouse layout, chemical storage volume, and liquid density specifications. Our senior structural engineers will provide a customized 3D design concept, capacity verification, and factory-direct quotation within 24 hours.
Technical Details for Expedited Quotations
- Warehouse clear ceiling height, column spans, and slab specs
- Container type: 1000L IBC totes, 55-gallon drums, or carboys
- Liquid specific gravity and gross unit load (kg / pallet)
- Secondary spill containment capacity requirements (gal / L)
- Corrosive vapor exposure or local seismic acceleration codes