Engineered Heavy-Duty Racking Systems
High-yield Q235B/Q355B structural steel storage configurations precision-manufactured under ISO 9001:2015 and CE EN15512 specifications. Optimized for harsh operational duty cycles, cold environments, and high-density industrial storage.
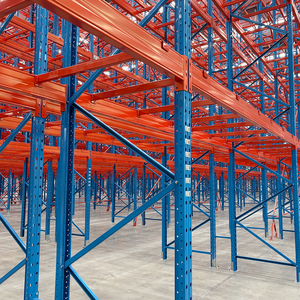
Heavy Duty Cold Room Modular Pallet Racking System
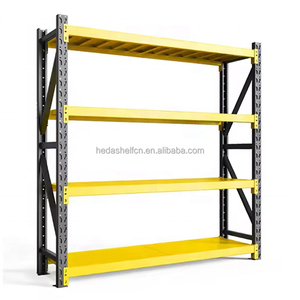
Industrial 4-Tier Boltless Heavy Duty Steel Stacking Shelves
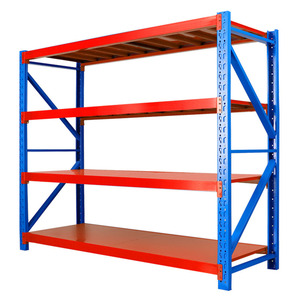
Industrial Multi-Tier Powder-Coated Cargo Stacking Storage Racks
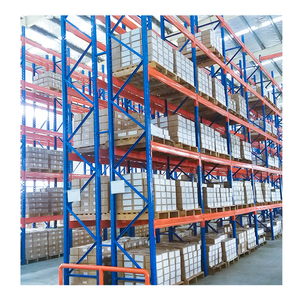
Heavy Duty Selective Steel Beam Pallet Racking System
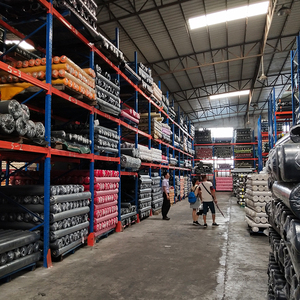
Engineered Heavy Duty Storage Rack (1000kg to 3000kg Capacity)
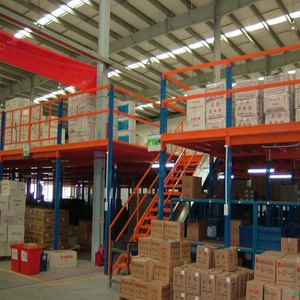
Modular Structural Steel Mezzanine Platform & Multi-Level Racking
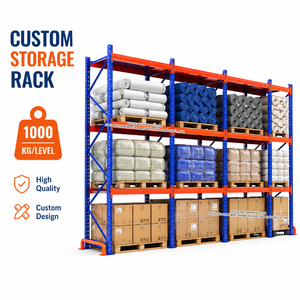
Standard 1000KG Industrial Adjustable Pallet Racking Bay
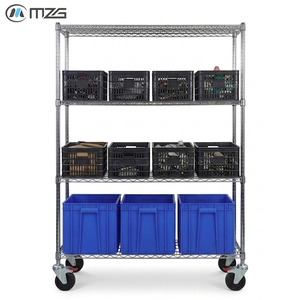
Industrial Mobile Heavy Duty Wire Shelving Units with Castors
Structural Integrity, Volumetric Economics, and Seismic Safety in Modern Factory Intralogistics
For modern manufacturing plants, fabrication facilities, and industrial distribution hubs, warehouse racking is no longer a passive utility; it represents a primary structural asset that directly dictates manufacturing throughput, crane and forklift cycle times, inventory carrying velocity, and employee life safety. Selecting the correct racking topology transforms unused clear vertical headroom into valuable cubic storage, avoiding costly land acquisitions and facility expansions.
Structural reliability requires adherence to global cold-formed structural steel standards, notably the Rack Manufacturers Institute (RMI MH16.1), the European Committee for Standardization (EN 15512 / EN 15620), and local building codes for seismic forces. Steel grade selection (e.g., high-tensile Q235B vs. Q355B with verified yield points of 235 MPa and 355 MPa respectively), upright punch profiles, beam-to-column connector lock mechanics, and baseplate anchorage depth must be mathematically calculated against both static live loads and dynamic impacts.
This whitepaper details the definitive top 10 warehouse racking systems engineered specifically for heavy industrial manufacturing, raw material warehousing, WIP staging, and high-turnover finished goods inventory.
Warehouse Space Optimization Benchmark
Analysis based on converting a 5,000 m² factory warehouse with 10.5m clear ceiling height from conventional floor block stacking to engineered pallet racking topologies:
Top 10 Industrial Warehouse Racking Configurations
A granular breakdown of each structural system, operational mechanics, load dynamics, and application fit for industrial manufacturing environments.
Standard Selective Pallet Racking
The global benchmark for manufacturing raw materials and multi-SKU component depots. Features single-deep horizontal beams linking upright portal trusses. Provides 100% direct selectivity to any pallet location without moving adjacent loads. Compatible with counterbalance, reach, and articulated forklifts.
Double Deep Pallet Racking
Engineered by pairing two back-to-back rows of selective racking. Requires specialized pantograph reach trucks with telescopic forks. Reduces aisle requirements by 50% across two consecutive racks, increasing cubic utilization by up to 30% compared to standard selective setups, suited for batch manufacturing runs.
Drive-In & Drive-Through Racking
Continuous tunnel design where forklifts drive directly into structural storage lanes along horizontal cantilever support rails. Eliminates interior operating aisles, creating ultra-dense pallet blocks. Ideal for seasonal raw materials, batch manufacturing output, and temperature-controlled cold rooms.
Radio Shuttle Semi-Automated Racking
Combines deep structural channels with independent, self-powered motorized robotic shuttles controlled via Wi-Fi tablets. Lift trucks deposit pallets at the bay face; the shuttle retrieves and stows pallets up to 40 meters deep. Dramatically minimizes forklift travel, bay impact hazards, and operator labor overhead.
Very Narrow Aisle (VNA) High-Bay Racking
Optimizes vertical volume by compressing operating aisles down to 1.6m - 1.9m and scaling upright heights up to 16+ meters. Operated by wire-guided or rail-guided turret trucks. Provides 100% individual pallet selectivity combined with ultra-dense footprints for land-constrained manufacturing plants.
Heavy-Duty Cantilever Racking
Engineered without front vertical columns, using central vertical structural masts and rigidly bolted, load-bearing horizontal arms. Built explicitly for non-standard, linear, and unpalletized materials including structural steel beams, extruded PVC/aluminum pipes, engineered timber, sheet metal packs, and bar stock.
Push Back Cart Racking (2 to 6 Deep)
Incorporates an inclined structural rail system housing nested wheeled structural carts. Loading a subsequent pallet pushes the preceding cart up the slight incline. Gravity advances pallets forward during retrieval. Provides high-density multi-lane storage while retaining individual lane SKU independence.
Pallet Flow (Gravity Flow) Racking
True FIFO dynamic rolling beds utilizing zinc-plated steel roller tracks set at a 3%-4% slope with mechanical speed governors and split entry safety separators. Pallets fed from the replenishment face coast safely to the picking face. Widely deployed in pharmaceutical, food processing, and fast-expiry industrial goods.
Rack-Supported & Structural Mezzanines
Transforms high ceiling voids into multi-level productive floors. Can be fully structural using heavy universal columns and beams, or rack-supported utilizing standard upright columns as load-bearing structural pilasters. Multiplying ground floor square meterage by 200% to 300% for assembly cells, offices, or carton picking.
Automated Storage & Retrieval Systems (ASRS)
High-bay steel structural matrices exceeding 30 meters, fully integrated with computerized automated stacker cranes, conveyor loops, and Warehouse Control Systems (WCS). Delivers continuous 24/7 dark-warehouse operation with zero operator damage, millimeter-level positioning, and real-time inventory reconciliation.
Industrial Racking Engineering Decision Matrix
Cross-evaluate structural systems across core logistical parameters: volumetric footprint, capital intensity, access selectivity, and specialized handling machinery requirements.
| Racking Topology | Floor Space Efficiency | Pallet Selectivity | Typical Load / Level | Aisle Width (Clearance) | CAPEX Index | Primary Industrial Fit |
|---|---|---|---|---|---|---|
| Selective Pallet Racking | 40% - 50% | 100% Direct | 1,000kg - 4,500kg | 3.2m - 3.8m | Low | General Assembly, Spare Parts, Engineering Tooling |
| Double Deep Racking | 60% - 65% | 50% Direct | 1,000kg - 3,000kg | 3.2m - 3.5m | Moderate | Batch Manufacturing, Staged Raw Materials |
| Drive-In Storage | 75% - 85% | 10% - 20% (LIFO) | 1,000kg - 2,000kg | Forklift Chassis Specific | Moderate | Cold Storage, Beverage Packaging, Plastics |
| Radio Shuttle Automation | 85% - 92% | Lane Dependent (FIFO/LIFO) | 500kg - 2,500kg | Transfer Aisle Only | High | Chemical Processing, Food Logistics, High Tonnage |
| Very Narrow Aisle (VNA) | 70% - 80% | 100% Direct | 1,000kg - 3,500kg | 1.65m - 1.85m | Moderate-High | Electronics, High-Density Distribution Hubs |
| Cantilever Systems | Varies by Material | 100% Direct | 500kg - 5,000kg/Arm | Material Length Dependent | Moderate | Pipes, Steel Rods, Sheet Timber, Aluminum Profiles |
| Push Back Racking | 65% - 75% | By Lane Face (LIFO) | 1,000kg - 2,000kg | 3.0m - 3.4m | Moderate-High | Buffer Storage, Staging Zones, Auto Component Depots |
| Pallet Flow (Gravity) | 80% - 90% | Strict FIFO | 800kg - 1,800kg | Separate Infeed & Pick Faces | High | Fast FMCG, Expiry Controlled Raw Ingredients |
| Rack-Supported Mezzanine | 150% - 300% (Usable Floor) | Multi-Level Access | 300kg - 1,500kg/m² | Variable Internal Aisles | Moderate | Light Assembly, Maintenance Stores, Packing Lines |
| High-Bay ASRS | 90% - 98% | 100% Computerized | 500kg - 3,000kg | Crane Mast Profile (~1.4m) | Ultra-High | Tier-1 Automotive, Mega-Distribution, Cleanroom Plants |
Procurement & Technological Trends in Industrial Storage
Forward-looking manufacturing enterprises are transitioning from commoditized racking purchases to comprehensive, technologically resilient intralogistics ecosystems.
Autonomous Mobile Robot (AMR) & Cobot Synergy
Procurement specifications now frequently mandate hybrid racking designs that seamlessly integrate ground-level automated mobile robot under-passages, automated guided vehicle (AGV) docking interfaces, and robotic tote shuttles. Standard floor beams are increasingly modified with integrated fiber-optic and magnetic navigation tracks to accommodate collaborative human-robot picking workflows.
High-Ductility Seismic Performance Engineering
With major manufacturing expansions across seismically active zones in Southeast Asia, Japan, and the Americas, buyers require verified Finite Element Analysis (FEA) reports under dynamic earthquake loadings. Next-generation uprights incorporate engineered seismic base isolation dampening and enlarged high-tensile anchor footprints conforming to stringent Eurocode 8 and AS 4084 compliance.
Advanced Anti-Corrosion & Tropicalized Finishes
High humidity, chemical vapor emissions, and sub-zero cold room environments degrade standard paint finishes rapidly. Contemporary procurement demands automated multi-stage pre-treatment (acid pickling, zinc phosphating, and deionized water cascading) followed by thermo-cured epoxy-polyester electrostatic powder coating (>70-90 microns) or continuous ISO 1461 hot-dip galvanizing.
Guangzhou Heda Shelves Co., Ltd.
Headquartered in Guangzhou, China, HEDA Shelves has been a premier direct designer, structural fabricator, and exporter of certified industrial heavy-duty racking, mezzanine systems, and automated storage architectures since 2001.
Complete Vertical Manufacturing
Zero subcontracting. Precision uncoiling, automatic CNC roll-forming, continuous punching lines, robotic welding stations, and fully automated Swiss Gema electrostatic powder-coating lines are centralized under one accountable roof in Guangzhou.
Rapid Engineering (24-48h 3D CAD)
Our dedicated structural engineering team develops full 2D layout schematics, 3D realistic visualizations, and structural load deflection calculations within 24 to 48 hours of receiving your warehouse architectural floor plans.
International Certification Compliance
Fully compliant with CE Marking (Certificate No. 2435-CPR-8605159), ISO 9001:2015 Quality Management Systems (Certificate No. 18624Q00169R0M), and RoHS environmentally compliant surface finishing.
Frequently Asked Questions by Industrial Buyers
Authoritative answers to critical engineering, safety certification, and commercial inquiries encountered during factory racking procurement.
What specific structural engineering calculations are required before installing heavy-duty pallet racks on a concrete floor slab?
How is beam deflection calculated and what are allowable deflection tolerances under full load?
Can standard powder-coated pallet racking be utilized in sub-zero cold room environments?
What information must a factory provide to receive a full 3D CAD layout and structural quotation?
What are the key safety distinctions between roll-formed and structural steel racking systems?
How does HEDA Shelves manage container consolidation and international transit damage prevention?
Obtain Your Tailored Industrial Storage Whitepaper & CAD Layout
Consult with our senior structural engineers today. We supply complete 2D/3D warehouse designs, finite element calculations, and direct manufacturer price schedules tailored to your precise industrial payload profile.