Featured Industrial Gravity & Warehouse Flow Storage Systems
Our dynamic roller lanes, carton beds, and structural pallet flow architectures are precision engineered to eliminate dead aisle space, enforce strict First-In-First-Out (FIFO) stock rotation, and minimize picking travel times by up to 65%.
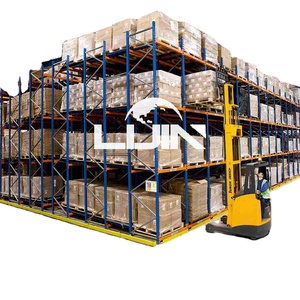
High Standard OEM Live Pallet Rack Gravity Flow Rack
Heavy-duty live dynamic bed with reinforced centrifugal speed brakes for controlled descent.
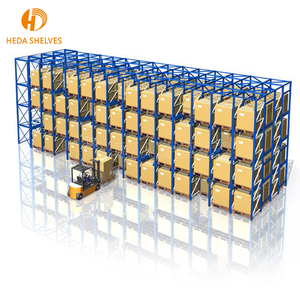
High-Capacity Heavy Duty Drive-In Pallet Racking Corrosion Protection
Maximum cube utilization engineered for bulk storage with continuous rail channel profiling.
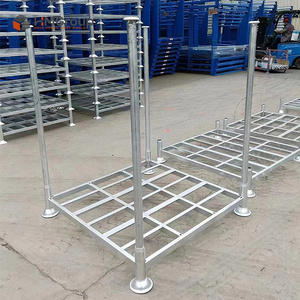
Heavy Duty Industrial Galvanized Steel Stacking Pipe Pallet Stillages
Rugged post-pallet stillages hot-dip treated for harsh environments and fluctuating inventories.
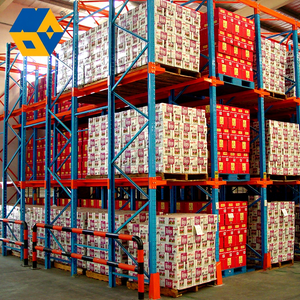
Customized Q235 Cold Rolled Steel Drive-in Storage System Rack
Custom cold-formed upright uprights with multi-hook bracket joints providing seismic resistance.
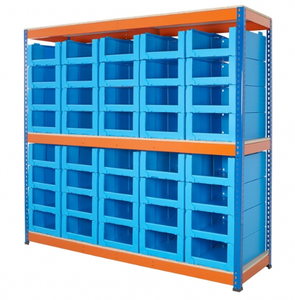
Corrugated Plastic SEMI-OPEN Stacking Warehouse Parts Bin
Ultra-durable modular containers built specifically for gravity roller bed drop-in replenishment.
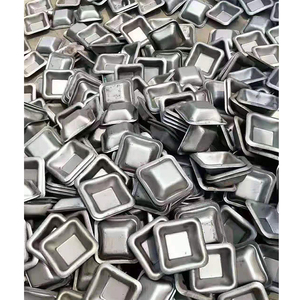
Metal Pallet Feet for Detachable & Foldable Stillage Racks
Precision die-stamped nesting cups ensuring multi-tier vertical alignment stability under load.
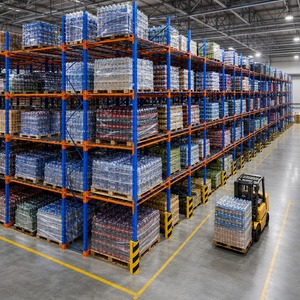
Q235B Steel Pallet Flow Racks for Bulk Chemical & High-Density Storage
Corrosion-resistant epoxy coated tracks engineered for heavy-duty drum and tote fluid transport.
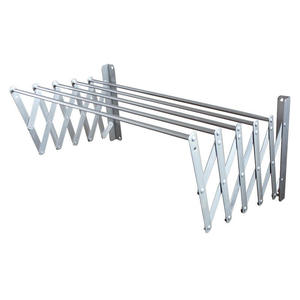
Aluminum Alloy Sliding Push-Pull Flow Track Auxiliary Module
Lightweight secondary gliding rail architecture for ergonomic kitting stations and assembly lines.
State of Span Track Flow Racks: Engineering Principles & Dynamic Storage Mechanics
In contemporary warehousing, logistics engineering, and high-frequency omni-channel e-commerce fulfillment centers, span track flow racks (commonly integrated as carton flow or dynamic gravity bed systems) constitute the critical operational boundary between storage density and picking velocity. Unlike static shelving, which demands extensive operator travel corridors and manual stock positioning, span track flow systems utilize inclined, gravity-fed roller beds or multi-wheel tracks. By separating replenishment loading from fulfillment picking into separate aisles, warehouses eliminate personnel-vehicle conflict, shorten split-case and full-case picking paths by up to 60%, and achieve autonomous First-In-First-Out (FIFO) material rotation.
From a metallurgical and structural engineering vantage point, high-performance span tracks must sustain non-uniform dynamic rolling loads, dynamic wheel-impact loads from uncoordinated operator loading, and ambient thermal fluctuations ranging from -30°C cold-chain deep freeze facilities to +55°C hyper-arid industrial depots. The fundamental structural distinction between low-grade consumer track and industrial-grade carton flow lies in the cold-rolled profile geometry, wheel pitch calibration, roller axle shear strength, and the integration of impact trays with drop-in galvanized steel entry guides.
Carton Flow Bed Architecture vs. Conventional Selective Racking
| Performance Vector | Static Selective Shelving | Wheel-Bed Carton Flow (Span Track) | Roller-Lane Gravity Beds |
|---|---|---|---|
| Inventory Rotation | Last-In-First-Out (LIFO) or Manual FIFO | Strict Automatic FIFO (Gravity Induced) | Strict Automatic FIFO (Dedicated Pitch) |
| SKU Pick Density | Low (Limited by shelf facings) | Ultra-High (Variable lane width adaptability) | High (Fixed roller track spacing) |
| Replenishment Interference | High (Shared single aisle pick & replenish) | Zero (Rear loading, front picking aisles) | Zero (Bifurcated operation aisles) |
| Travel Time Reduction | Baseline (0%) | 50% to 70% Travel Path Reduction | 45% to 65% Travel Path Reduction |
| Cold Storage Footprint ROI | Poor (High thermal volume waste) | Exceptional (Compresses chilled air cube) | Exceptional (High thermal efficiency) |
Top 10 Global Span Track & Flow Rack Manufacturers
This ranking assesses structural cold-roll manufacturing capacity, ISO quality assurance protocols, dimensional tolerances, custom lane flexibility, and global export infrastructure across Tier-1 factory producers.
Established in 2001 in Guangzhou, China, HEDA operates a modernized 30,000 m² heavy-gauge roll-forming and electrostatic coating complex. Holding CE (No. 2435-CPR-8605159) and ISO 9001:2015 certifications, HEDA delivers tailor-engineered span track carton flow, dynamic live pallet flow systems, and integrated structural picking mezzanines. Complete in-house manufacturing—from steel coil slitting to automated robot welding and 10-step pickling/phosphating—delivers unrivaled dimensional consistency and factory-direct cost efficiency for global projects.
Pioneers of the original "SpanTrack" trademark brand, UNEX delivers high-capacity full-width roller and wheel track configurations dropping directly into existing pallet rack step beams. Noted for hex-hub steel roller bearings and ergonomic knuckled outer shelves for order pickers.
Swiss engineering giant recognized for modular conveyor elements, dynamic flow storage rollers, and precision speed controllers. Specializes in advanced centrifugal speed controllers ensuring controlled pallet descent velocities in deep-lane installations.
Renowned for extreme-capacity gravity flow systems, including the "Dyna-Flo" wheel bed series and steel roller tracks designed to resist forklift abuse. Engineered for harsh foundry, beverage processing, and heavy automotive assembly lines.
BITO is a recognized European market leader in live storage shelving and carton flow technology. Their multi-tier picking towers feature continuous zinc-plated roller tracks and modular lane dividers compliant with strict European logistics ergonomics.
Global rack engineering conglomerate with extensive live pallet and live carton flow implementations. Incorporates durable resin or galvanized metal rollers with proprietary pick-to-light clip profiles for distribution hubs.
Delivers fully automated and semi-automated intralogistics ecosystems. Schaefer’s live storage carton flow racks utilize high-precision cylindrical plastic rollers mounted on steel channels, engineered to integrate with autonomous picking carts and AGVs.
Historic pioneer of slotted angle and pallet racking. Dexion’s carton live beds feature modular wheel tracks and ergonomic return shelves designed for return tote conveyance in retail and pharmaceutical order assembly facilities.
Distinguished by structural channel steel manufacturing rather than standard roll-formed sheet steel. Frazier’s flow beds withstand severe impact shocks from heavy industrial tote loading and rough forklift handling in grocery distribution networks.
Leading European racking fabricator known for its versatile "Stow Flow" dynamic live storage solutions. Specializes in low-profile dynamic lanes with fine roller pitches ensuring carton movement without hang-ups or point-load packaging deformation.
Future Procurement Shifts & Technological Evolution in Flow Storage
The industrial warehousing sector is undergoing a profound structural transition driven by rising square-meter real estate leases, global labor shortages, and skyrocketing SKU proliferation in consumer direct channels. Span track and dynamic flow rack designs are rapidly evolving beyond simple passive gravity chutes into intelligent, sensorized material handling nodes.
1. Modular Universal Wheel Beds vs. Fixed Roller Tracks
Procurement teams are shifting away from dedicated, fixed-width single-roller tracks toward drop-in universal wheel beds. Variable package sizing driven by on-demand e-commerce packaging makes fixed-lane carton flow obsolete when box dimensions change quarterly. Universal wheel tracks allow packaging of varied dimensions to travel side-by-side on identical dynamic decks without requiring tools to reconfigure structural dividers.
2. IoT Sensorization & Pick-to-Light Direct Integration
Modern high-velocity pick faces feature snap-on aluminum extruded front discharge trays embedded with optical time-of-flight (ToF) sensors. These sensors detect when a carton clears the pick point, automatically triggering replenishment alerts to WMS software. This eliminates pick-out delays, synchronizing warehouse replenishment teams before stock depletion halts fulfillment lines.
3. Hybrid Robotic AMR/AGV Induction Faces
As autonomous mobile robots (AMRs) become standard in modern DC operations, rear-loading flow rack charge faces are being re-engineered with robotic dock guides, magnetic centering ramps, and low-friction rollers. These additions enable mobile robot arms or conveyor-equipped AMRs to deposit tote bins directly onto gravity lanes with sub-millimeter positional tolerance.
4. Sustainable Surface Engineering & Cold-Chain Metallurgy
In cold-storage applications (pharmaceutical vaccine preservation, frozen seafood distribution), conventional zinc plating often succumbs to micro-fissuring and galvanic corrosion due to condensation cycling. The future of flow rack engineering centers on eco-friendly chrome-free passivation, hot-dip continuous galvanization, and thermal-break polymer wheels that prevent brittleness down to -40°C.
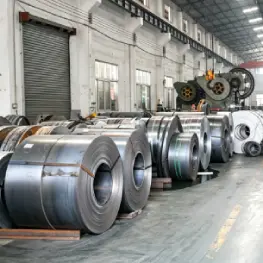
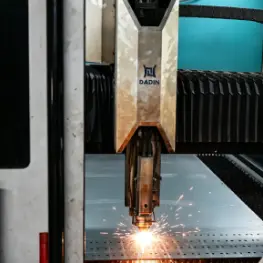
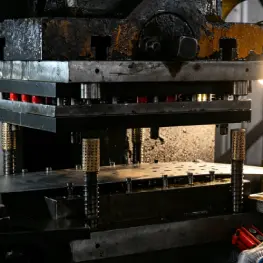
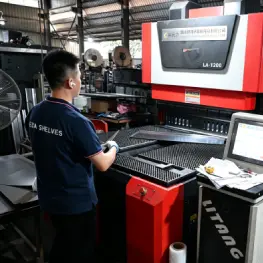
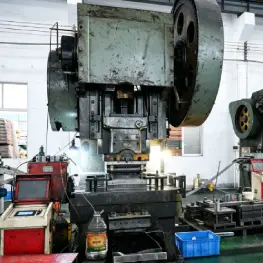
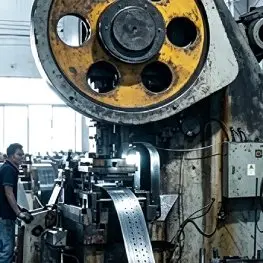
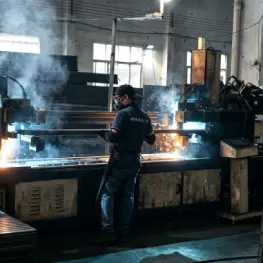
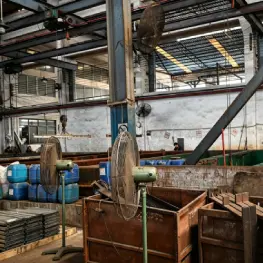
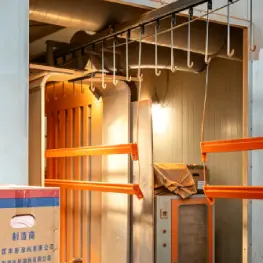
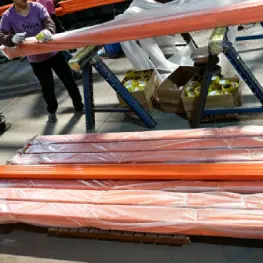
Guangzhou HEDA Shelves: 10-Step In-House Precision Manufacturing
Operating our dedicated 30,000 m² factory in Guangzhou, China, HEDA oversees the entire fabrication cycle under strict ISO 9001:2015 quality controls. We never outsource critical punching, forming, or coating processes.
Frequently Asked Questions: Sourcing Span Track Flow Racks
Essential technical, logistical, and structural answers for warehouse project engineers, 3PL managers, and procurement officers.
What slope pitch angle is standard for span track carton flow systems?
Can span track beds drop directly into existing selective pallet rack frames?
How does HEDA engineer racking against seismic risks in earthquake zones?
What is the load rating per linear meter of industrial-grade span track?
How are surface treatments calibrated for tropical humidity or sub-zero cold stores?
What technical data is required to generate a certified 2D CAD layout and quotation?
Ready to Optimize Your Warehouse Picking Velocity?
Get direct factory pricing, certified engineering calculations, and complimentary 3D layout renderings from Guangzhou HEDA Shelves Co., Ltd.