25+
Years Manufacturing (Since 2001)
30,000
Metric Tons Monthly Capacity
10,000+
Global Turnkey Projects
120+
Direct Export Destinations
Featured Industrial Storage & Pallet Handling Equipment
Discover precision-engineered dynamic and static storage configurations designed for variable load conditions, rigorous seismic tolerances, and seamless automation compatibility across modern distribution hubs.
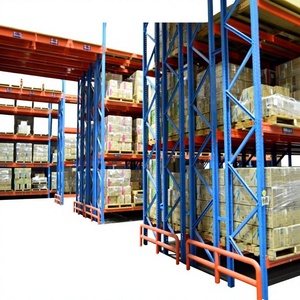
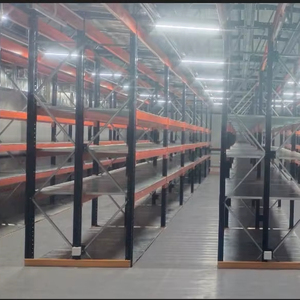
Top 10 Pallet Shuttle Racking Suppliers & Exporters Worldwide
Global supply chain directors and structural engineering consultants evaluate automated pallet shuttle racking manufacturers using five essential benchmarks: load bearing calculations, telemetry stability, cold-environment endurance, lead time predictability, and compliance with EN 15512 / RMI safety standards.
1. HEDA Shelves (Guangzhou, China)
Competitive Advantage: Established in 2001, Guangzhou Heda Shelves Co., Ltd. operates a vertically integrated 30,000 m² facility delivering full turnkey engineering from cold-roll profiling to sub-zero radio shuttle integration. Recognized for free 48-hour 3D/CAD structural simulation, seismic-resistant engineering for the Pacific Rim, and complete CE (No. 2435-CPR-8605159) and ISO 9001:2015 traceability.
2. Mecalux (Spain)
Competitive Advantage: A dominant European player with sophisticated proprietary Warehouse Management Software (Easy WMS). Mecalux provides robust semi-automated radio shuttles adapted for multi-depth channels with strong European market service networks, catering to pharmaceutical and dry food FMCG facilities requiring high ERP interoperability.
3. SSI Schaefer (Germany)
Competitive Advantage: Renowned for high-precision German mechatronics and heavy-duty structural durability. Their automated channel shuttles are engineered for 24/7 continuous cycles within multi-tier logistics hubs, offering long lifecycle performance and integrated automated guided vehicle (AGV) handoff interfaces.
4. Stow Group (Belgium)
Competitive Advantage: Pioneers of the Stow Atlas 2D and pallet shuttle system, focusing on modularity, ease of commissioning, and standardized parts supply across Europe and North America. Excellent mechanical tolerances reduce friction-induced motor wear on high-throughput deep-lane bays.
5. Dexion (Constructor Group, UK)
Competitive Advantage: Extensive historical expertise in industrial storage architecture. Dexion delivers specialized dynamic shuttle solutions that adhere to British Standard EN codes, providing bespoke safety railings, seismic anchors, and collision-avoidance sensor suites.
6. Bito Storage Systems (Germany)
Competitive Advantage: Focuses heavily on compact storage optimization and fast deployment times. Bito's pallet shuttle rails utilize high-precision cold-formed profiles that prevent shuttle deviation and reduce wheel elastomer degradation during continuous shifts.
7. Daifuku (Japan)
Competitive Advantage: The global standard for ultra-reliable automation and mission-critical intralogistics. Daifuku excels in multi-directional automated pallet shuttle carriers integrated with high-rise crane systems and seismic isolation platforms tailored for earthquake-vulnerable zones.
8. Interlake Mecalux (USA)
Competitive Advantage: Leading the North American warehousing market with comprehensive RMI (Rack Manufacturers Institute) compliant manufacturing. Known for heavy gauge upright structural steel and rapid delivery across the Americas, ideal for high-impact pallet turnover.
9. Jungheinrich AG (Germany)
Competitive Advantage: Seamless integration between electric lift trucks and under-pallet shuttle carriers. Jungheinrich provides industry-standard Li-ion rapid-charging battery packs that guarantee uninterrupted shuttle operation across three shifts in controlled-atmosphere distribution facilities.
10. Frazier Industrial (USA)
Competitive Advantage: Specializes in 100% hot-rolled structural steel construction. Frazier's shuttle racking systems offer extreme resistance to forklift impacts in heavy manufacturing, beverage distribution, and demanding cold-storage facilities across the Americas.
Future Procurement Trends for Pallet Shuttle Systems (2025–2030)
Procurement executives are shifting from purely CAPEX-driven evaluations to Life-Cycle Cost Analysis (LCCA). When sourcing pallet shuttle racking systems, procurement teams should plan around three structural shifts:
1. High-Density Cold Chain Standardization
With real estate and refrigeration energy costs rising across Southeast Asia, the Middle East, and Latin America, cold storage facilities are moving from traditional drive-in racks to automated radio shuttles. Procurement criteria now demand specialized lubricants rated down to -30°C, corrosion-resistant galvanized steel, and condensation-sealed IP65 electrical enclosures.
2. WMS/WCS Agnostic Architecture
Proprietary closed-loop shuttle controls are giving way to open API communications via standard Industrial Ethernet and Wi-Fi 6. Buyers require shuttle carrier firmware that interfaces smoothly with third-party software like SAP EWM, Manhattan Associates, and bespoke warehouse management systems without expensive vendor lock-in fees.
3. Circular Economy & Certified Steel Sourcing
Corporate ESG mandates and building safety codes require verified material test reports (MTR). Procurement teams increasingly specify high-tensile Q235B/Q355B or European S355 steel, coupled with low-VOC electrostatic powder coatings that meet international RoHS environmental standards.
Key Technological Developments in Pallet Shuttle Engineering
Continuous R&D across mechanical and software disciplines is transforming pallet shuttles from semi-automated lane carriers into fully autonomous intralogistics assets:
Transition from 1D to Multi-Directional 4-Way Shuttles
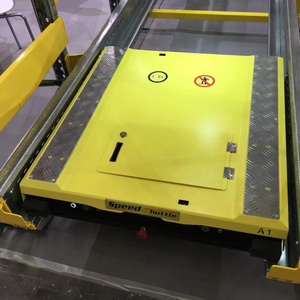
Traditional shuttle cars run longitudinally along a single rail channel. Emerging systems use 4-way direction-shifting mechanisms, enabling the shuttle to traverse lateral transfer aisles and vertical lifts. This eliminates internal forklift travel and opens the door to high-throughput, dark-warehouse operations.
Ultra-Capacitor and Super-Fast LiFePO4 Power
Lead-acid batteries with 8-hour charge cycles are obsolete. Modern industrial shuttles utilize Lithium Iron Phosphate (LiFePO4) or integrated supercapacitors. These power cells reach 80% charge in just 20 minutes through opportunity charging stations built directly into the rail ends.
LiDAR Mapping and Onboard Anti-Collision Telemetry
Modern radio shuttles feature intelligent optical distance measurement, non-contact obstacle detection, and pallet overhang sensors. These systems prevent high-speed collisions with warped wooden pallets or misaligned loads, protecting structural integrity and cutting unscheduled maintenance downtime.
Why Partner with HEDA Shelves for International Engineering Projects
Operating since 2001, Guangzhou Heda Shelves Co., Ltd. combines advanced manufacturing facilities with an experienced structural engineering team to solve challenging layout, load, and logistics demands worldwide.
In-House Manufacturing Control
Our 30,000 m² Guangzhou production facility oversees all 10 essential stages in-house: automated coil slitting, cold roll-forming, computerized upright punching, robotic beam welding, pickling, phosphating, and electrostatic powder coating. This end-to-end control ensures structural precision and consistent batch delivery.
Free 3D & CAD Layout Verification
Before production begins, HEDA structural engineers review your warehouse floor plan, clear height, floor slab load limits, and lift truck specifications. We provide complete 2D CAD layout prints, dynamic 3D structural views, and accurate pallet capacity counts within 24 to 48 hours at no additional charge.
Seismic & Climate Adaptation
Engineered for challenging environments, our racking incorporates customized upright profiles, reinforced bracing, heavy-gauge baseplates, and chemical anchors designed for seismic regions like the Philippines, Indonesia, and Japan. For high-humidity or cold-chain setups, we offer hot-dip galvanizing and sub-zero powder formulations.
International Certification & Export Packaging
Our manufacturing follows strict quality guidelines backed by CE (Certificate No. 2435-CPR-8605159), ISO 9001:2015, and RoHS compliance. Materials are bundled with protective steel strapping, corner protectors, and clear packing lists designed for fast container offloading and smooth local assembly.
Frequently Asked Questions: Pallet Shuttle Racking Systems
Essential technical, structural, and commercial details to guide your warehouse design and equipment procurement.
What is the difference between Pallet Shuttle Racking and Drive-In Racking?
Drive-in racking requires forklifts to enter structural storage bays, creating collision risks, slowing pallet turnover, and limiting lane depth to typically 6–8 pallets. In contrast, pallet shuttle systems use a remote-controlled shuttle carrier running along precision rails inside the lane. Forklifts only work at the front face. This cuts loading cycles by 40–50%, eliminates structural impact damage from trucks, supports lane depths over 40 pallets, and flexibly accommodates both FIFO (First-In, First-Out) and LIFO (Last-In, First-Out) picking strategies.
What warehouse parameters are required to generate an accurate 3D CAD design?
To prepare a structural calculation report and CAD plan, our engineering department needs: (1) A warehouse layout showing column positions, building clear height, and overhead utility lines; (2) Pallet dimensions (width, depth, height including load) and maximum weight per pallet; (3) Pallet bottom design (e.g., Euro, GMA, full-perimeter, or 3-skid); (4) Lift truck model, maximum mast height, and turning radius; (5) Required daily pallet turnover rates; and (6) Temperature conditions (ambient, cold room, or blast freezer).
Can HEDA Shelves pallet shuttle systems be used in sub-zero cold storage?
Yes. Our cold-chain shuttle units are built for stable operation in ambient temperatures down to -30°C. Cold-chain specifications include low-temperature synthetic lubricants, condensation-sealed internal electronics with conformal coatings, heated sensor lenses, and specialized low-temperature Lithium Iron Phosphate (LiFePO4) battery packs with built-in thermal management. Racking structures for cold storage can also be specified with hot-dip galvanized finishes to resist condensation corrosion.
How are structural components protected against rust in tropical and coastal ports?
Every steel component goes through an 8-stage surface pre-treatment process, including chemical degreasing, acid pickling, rust removal, and zinc phosphating. This is followed by an electrostatic powder coating cured at 180°C–200°C to create a smooth, impact-resistant finish. For coastal areas, chemical manufacturing plants, and high-humidity environments, we supply hot-dip galvanized uprights, rails, and baseplates conforming to ISO 1461 standards, ensuring lasting salt-spray resistance.
What certifications and design codes are used for seismic verification?
HEDA Shelves products carry CE certification (No. 2435-CPR-8605159) and ISO 9001:2015 quality assurance. Our structural engineers design systems according to European standards EN 15512, EN 15620, and EN 15629, as well as American RMI standards. For seismic zones across the Pacific Rim, upright profile gauges, anchor diameters, and cross-bracing layouts are calibrated using structural calculations to ensure compliance with local building permit codes.
How is installation and technical commissioning handled for export markets?
Each container export includes a detailed component list, load capacity plaques, color-coded CAD installation prints, and step-by-step assembly diagrams. Components are pre-punched and precision cut for fast bolt-together field installation without on-site welding. For major distribution hubs, HEDA Shelves can deploy site-supervision engineers to oversee erection, level rails, calibrate radio shuttle units, and train local forklift operators.
Design Your High-Density Pallet Storage System
Speak directly with our technical team in Guangzhou to request a tailored CAD floor plan, 3D structural simulation, and project quote based on your pallet profile and throughput requirements.
Contact Us