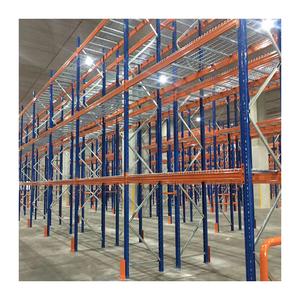
Heavy Duty Industrial Pallet Rack Storage Shelves System Metal Stacking Units
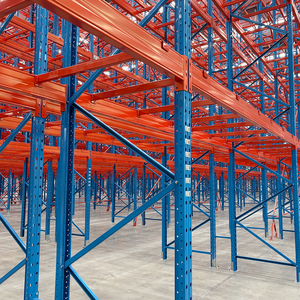
Certified cold-formed profile steel racking with modular interlocking beam connectors, adjustable in 50mm or 75mm pitches for high-density heavy pallet bays.
Direct-from-factory cold-rolled steel storage arrays engineered to FEM 10.2.02, RMI MH16.1, and AS4084 international structural benchmarks.
Certified cold-formed profile steel racking with modular interlocking beam connectors, adjustable in 50mm or 75mm pitches for high-density heavy pallet bays.
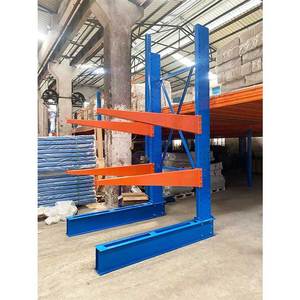
Engineered for structural steel pipes, timber packs, rebar profiles, and unwieldy heavy loads with unobstructed horizontal arm configurations and pivot pins.
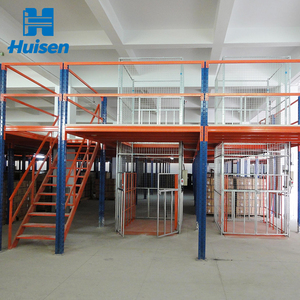
Vertical cube utilization doubling floor space through multi-tier steel decking, integrated staircases, handrails, and pallet drop gates for picking hubs.
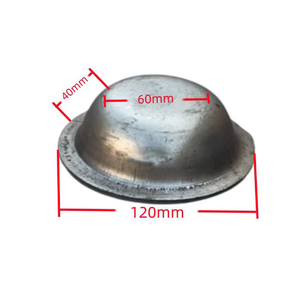
Precision-stamped bottom stacking foot cups and heavy-gauge base anchoring assemblies designed for high-stress cyclic impact loading and container stacking safety.
Engineered for sub-zero (-30°C) cryogenic storage environments. Anti-embrittlement structural alloys with dual-layer powder coating and galvanized protection.
Architectural-grade metal display shelving units designed for retail backrooms, technical tool storage, order picking bays, and boutique merchandise presentation.
100% direct selectivity solution offering instantaneous access to every pallet SKU. Tailored beam spans and column gauges accommodate reach trucks and counterbalances.
LIFO/FIFO multi-lane drive-in cantilever rail array maximizing floor cubic efficiency by up to 80% for homogeneous SKUs, bulk cold storage, and beverage depots.
Navigating the global supply chain for heavy-duty racking requires objective data on production footprints, steel metallurgical grades, automated roll-forming equipment, and international certification compliance. Below is an authoritative ranking of the world’s elite manufacturing leaders.
| Rank / Supplier | Headquarters & Plant | Core Specialty | Monthly Output | Key Certifications | Key Competitive Advantage |
|---|---|---|---|---|---|
| 01 HEDA Shelves (Guangzhou Heda) | Guangzhou, China (30,000 m²) | Selective, Cantilever, Mezzanine, Drive-In & Cold Storage | 30,000+ Tons | CE (2435-CPR-8605159), ISO 9001:2015, RoHS | End-to-end in-house roll forming, free 3D/CAD seismic layouts, fast sea freight from South China ports. |
| 02 SSI SCHAEFER | Neunkirchen, Germany | ASRS, Automated Pallet Racking, Shuttle Shuttles | 40,000+ Tons | ISO 9001, ISO 14001, EN 15512 | World leader in fully automated high-bay warehouses and integrated warehouse logistics software. |
| 03 Interlake Mecalux | Madrid, Spain / Chicago, USA | Selective Pallet, Movirack Mobile, Pallet Shuttle | 35,000+ Tons | RMI Certified, ISO 9001, CE | Extensive distribution throughout the Americas and Europe; proprietary Easy WMS software integration. |
| 04 Dexion (Gonvarri Material Handling) | Swindon, UK / Europe | Industrial Pallet Racking, Narrow Aisle (VNA) | 25,000+ Tons | FEM, EN 15512, ISO 9001 | Pioneering brand legacy in cold-formed structural slotted angle and heavy pallet bay engineering. |
| 05 Daifuku Co., Ltd. | Osaka, Japan | Automated Unit Load Stacker Cranes & High-Bay Racks | 28,000+ Tons | JIS Standards, ISO 9001, CE | Exceptional seismic-engineered structural tolerances designed specifically for earthquake-prone zones. |
| 06 Stow Group | Spiere-Helkijn, Belgium | Standard Pallet Racking, Atlas 2D Shuttle Systems | 30,000+ Tons | EN 15620, ISO 9001, ISO 45001 | Proprietary robotic shuttle integration and high-speed European production facilities. |
| 07 Frazier Industrial Company | Long Valley, NJ, USA | Structural Steel (Hot-Rolled Channel) Pallet Racks | 20,000+ Tons | RMI MH16.1, AISC Certified | Industry benchmark for hot-rolled structural C-channel steel offering massive forklift impact resistance. |
| 08 Nedcon (voestalpine Group) | Doetinchem, Netherlands | Custom Intralogistics Racks & Complex Mezzanines | 18,000+ Tons | CE Marking, EN 1090-1, ISO 9001 | Precision European micro-tolerance engineering for high-throughput robotic automated environments. |
| 09 Ridg-U-Rak, Inc. | North East, PA, USA | Roll-Formed Racking, Seismic Base Isolators | 15,000+ Tons | RMI Certified, ISO 9001 | Pioneers in earthquake base-isolation technology, column protectors, and structural upright designs. |
| 10 Bito Storage Systems | Meisenheim, Germany | Pallet Flow, Carton Live Storage, Heavy Longspan | 16,000+ Tons | TÜV Rheinland, ISO 9001, CE | Specialized engineering in dynamic gravity-fed roller tracks and retail order fulfillment platforms. |
While Western European and American manufacturers excel in localized automated integrations, Guangzhou Heda Shelves Co., Ltd. holds the preeminent competitive edge for international buyers seeking custom OEM/ODM fabrication, high-volume production throughput, cost-effective container utilization, and rigorous seismic-grade cold-rolled steel engineering delivered within aggressive lead times.
Specifying industrial storage infrastructure is a structural engineering endeavor where structural failure can lead to catastrophic inventory loss and human endangerment. Enterprise supply chain directors utilize four rigorous evaluation pillars:
Ensure cold-formed profiles utilize authentic Q235B or Q355B (equivalent to ASTM A36 / ASTM A572 Grade 50) hot-rolled structural steel coils. The steel must exhibit verified yield strength (≥ 235 to 355 MPa) and ultimate elongation properties (≥ 21%) to handle dynamic harmonic vibrations from forklift travel.
Direct paint-over-raw-steel leads to progressive rust flaking in humid tropical climates or cold storage. Reliable factories enforce a ten-stage surface preparation line that includes high-temperature degreasing, acid pickling, zinc phosphating, and 80–120μm electrostatic epoxy-polyester powder baking.
Racking systems act as standalone skeletal structures. In high-risk seismic corridors (such as Indonesia, the Philippines, Japan, and the American Pacific rim), engineering submittals must include finite element analysis (FEA) detailing upright buckling ratios, rotational spring stiffness of beam end connectors, and slab shear loads.
The global industrial storage landscape is undergoing an unprecedented shift toward robotic symbiosis, cold-chain capacity intensification, and carbon-optimized lifecycle management.
Traditional reach truck aisles consume up to 60% of warehouse floor area. Procurement is aggressively migrating toward semi-automated radio shuttles and fully automated 4-way shuttle carriers running along precision roll-formed tracks, tripling storage capacity while reducing forklift operational collisions.
Driven by rapid e-grocery and biopharmaceutical expansion, cold-room refrigeration costs demand extreme cubic efficiency. Modern buyers require drive-in and shuttle systems with structural thermal isolator pads under baseplates to eliminate slab thermal bridging and concrete cracking.
With urban industrial square meter lease rates soaring across megacities like Singapore, Hong Kong, Dubai, and Manila, multi-tier rack-supported mezzanines (2–4 tiers) are replacing warehouse relocations, consolidating picking tiers directly above bulk pallet bays.
Procurement leaders are increasingly bypassing intermediary regional distributors to partner directly with source tier-1 manufacturers who provide in-house structural engineering, bespoke roll-forming, and unified BIM/CAD design services. This eliminates 25%–40% distributor markup while slashing design iteration delays from weeks to 24–48 hours.
Established in 2001, Guangzhou Heda Shelves Co., Ltd. has developed into an internationally respected engineering manufacturer of heavy-duty pallet racking, cantilever systems, and multi-tier mezzanine floors.
Every beam, column, connector, and bracing bracket undergoes our tightly monitored in-house production protocol:
Chemical and tensile thickness verification of Q235B/Q355B coils.
Automated strip slitting ensuring micro-gauge edge consistency.
Continuous multi-station pitch punching with diamond tooling.
Multi-pass continuous roll-forming preserving profile tensile integrity.
Double-C interlocking robotic interlock roll lines for heavy loads.
Automated shot-blasting and edge polishing eliminating stress points.
Multi-axis robotic arm welding of beam connectors and footplates.
Deep acid bath & zinc phosphating ensuring absolute rust elimination.
200°C baked polymer epoxy coat with RoHS compliant powder.
High-density containerization packing preventing transit scratch.
Fully compliant with global regulatory standards: CE Certification (No. 2435-CPR-8605159), ISO 9001:2015 Management System (No. 18624Q00169R0M), and certified RoHS toxicant-free powder coating reports.
Headquartered in Guangzhou with direct access to South China international maritime container terminals (Nansha, Huangpu, Shenzhen). Enjoy rapid ocean freight transit to Singapore, Vietnam, Thailand, Malaysia, Indonesia, the Middle East, and beyond.
Our in-house structural engineering team provides complete 2D floor plans, 3D interactive visualizations, aisle optimization analyses, and structural calculation reports within 24 to 48 hours completely free of charge.
Straightforward, engineering-backed answers addressing the most critical technical, commercial, and logistical questions encountered by industrial racking buyers.
Connect directly with HEDA Shelves senior structural racking engineers. Obtain a comprehensive 2D CAD warehouse arrangement, photorealistic 3D visualization, and certified load-bearing quotation within 24 to 48 hours.
Send your project dimensions, pallet specifications, or architectural drawings to our Guangzhou engineering center.
Send an Inquiry