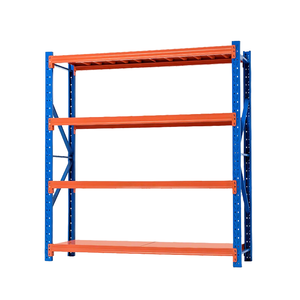
Industrial 4-Layer Boltless Steel Storage Rack
Designed for high-density carton handling, manual pick modules, and secondary sorting zones. Features rivet interlock uprights requiring zero hardware for lightning-fast site erection.
Explore heavy-duty, certified cold-formed steel racking systems engineered directly in our Guangzhou manufacturing plant for global third-party logistics (3PL), automotive facilities, cold storage, and heavy industrial distribution centers.
Designed for high-density carton handling, manual pick modules, and secondary sorting zones. Features rivet interlock uprights requiring zero hardware for lightning-fast site erection.
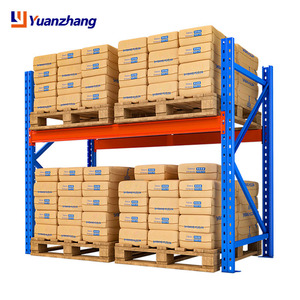
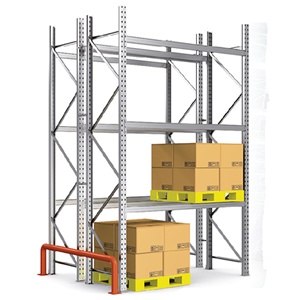
Roll-formed heavy gauge steel framework offering 100% pallet selectivity or double deep configurations. Fitted with high-safety locking pins and reinforced teardrop connectors.
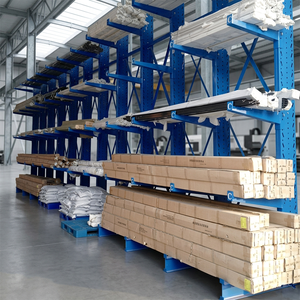
Engineered for long-span bar stock, structural tubes, PVC piping, and timber. Modular cantilever arms with pivot joints absorb accidental forklift shock without permanent structural damage.
Specially braced box-beam geometry engineered with 3-claw high-tensile connection tabs. Minimizes horizontal deflection and prevents beam roll under point-concentrated pallet loads.
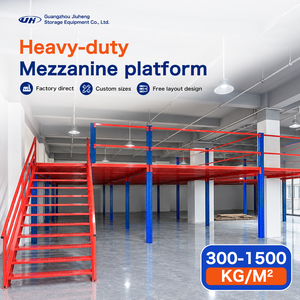
Doubles or triples usable facility square meters without building extensions. Integrates staircase systems, pallet drop gates, guardrails, and heavy-duty steel grating walkways.
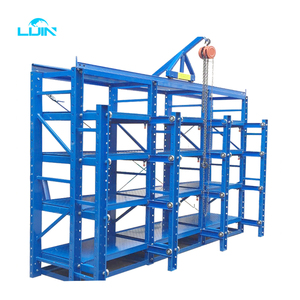
Heavy sliding drawer mechanism designed for injection molds, stamping dies, and heavy CNC fixtures. Incorporates automatic safety mechanical interlocks to allow only one drawer out at a time.
Mandatory NFPA and EN building safety compliance component ensuring constant longitudinal separation between back-to-back rack runs for vertical sprinkler penetration and structural tying.
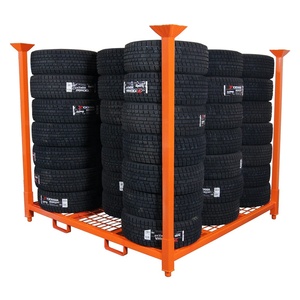
Modular post-pallet tire storage rack that stacks up to 4–5 units high under full loading. Demountable structural corner uprights minimize empty return freight by up to 80%.
An objective, technical side-by-side analysis of the world's premier drive-in pallet racking manufacturers. Evaluated on cold-formed steel tensile integrity, continuous rail beam deflection thresholds, seismic bracing certifications, and direct-factory procurement economics.
Established in 2001, Guangzhou HEDA Shelves stands out as the definitive global powerhouse for direct-factory high-density drive-in pallet racking systems. Operating a massive 30,000 m² automated facility in Haizhu District, Guangzhou, HEDA integrates high-speed roll forming lines, robotic robotic portal welding, in-house pickling and phosphating lines, and computerized dual-stage electrostatic powder coating booths. HEDA’s drive-in racking is engineered specifically to eliminate wasted forklift aisles, achieving up to 80% warehouse volumetric cubic efficiency compared to standard selective setups.
Unlike trading intermediaries, HEDA provides end-to-end structural FEA (Finite Element Analysis) calculation packages, complimentary 2D CAD engineering plans, and photorealistic 3D warehouse simulations delivered within 24 to 48 hours. Holding strict European CE certification (No. 2435-CPR-8605159), ISO 9001:2015 quality accreditation, and RoHS non-toxic coating compliance, HEDA is the direct manufacturer of choice for global cold storage facilities, beverage bottling plants, and heavy manufacturing giants across Southeast Asia, South Asia, the Middle East, and North America.
A European titan in high-density drive-in systems, Mecalux provides exceptional automated and conventional drive-in pallet racking systems. Their structural designs feature flared entrance guides and heavy floor-anchored steel ground rails that protect upright columns from mast impact. Widely utilized across European distribution networks and third-party logistics warehouses.
Recognized worldwide for high-precision German engineering, SSI Schaefer manufactures drive-in and drive-through racks engineered with cold-rolled boltless frames and custom load rails. Their systems are frequently specified for turnkey mega-distribution centers requiring tight integration with complex materials handling infrastructure.
Stow specializes in industrial pallet storage solutions with high-capacity continuous rail drive-in racking. Their proprietary continuous pallet support profile provides outstanding torsional stiffness and maximum horizontal stability even under extreme heavy-pallet point concentrations in cold storage logistics.
With historical roots dating back to slotted angle iron pioneers, Dexion delivers drive-in systems across the UK, Australia, and the Middle East. Their drive-in racking emphasizes heavy-duty wrap-around column protectors, specialized top tie-beams, and robust diagonal rear portal bracing frames.
Frazier is North America's leading structural steel racking producer. Unlike roll-formed manufacturers, Frazier utilizes hot-rolled structural steel C-channels for their drive-in racking columns and load rails. Highly impact resistant and practically impervious to heavy forklift channel strikes in sub-zero freezers.
Jungheinrich delivers complete integrated warehouse solutions encompassing both forklift trucks and drive-in racking frameworks. Because they design the reach trucks and stackers alongside the steel racks, their lane tolerances, entry flare profiles, and mast clearance safety clearances are matched with micrometer accuracy.
BITO manufactures high-density storage solutions featuring specialized galvanized pallet support rails designed to minimize friction while maximizing stability during insertion. Their boltless bracket assembly system allows quick on-site adjustment of rail elevations to accommodate seasonal pallet height fluctuations.
A key player under the KION Group umbrella, Dematic provides drive-in and radio shuttle racking frameworks as part of large-scale automated and semi-automated distribution centers. Their drive-in racking frameworks feature heavy top portal tie beams engineered to handle seismic sway in seismically active warehouse clusters.
While renowned for dynamic gravity flow solutions, Interroll designs heavy drive-in and hybrid flow systems engineered around premium steel profiles. Their hybrid drive-in systems allow quick conversion into deep-lane roller flow lanes, offering forward-looking supply chains maximum flexibility between FIFO and LIFO batching.
Drive-in racking eliminates traditional pallet beam spans in favor of continuous cantilevered side support rails. Because forklift trucks drive directly inside the structural lane tunnels, structural sway calculations, baseplate anchoring, and vertical flue spaces require meticulous structural engineering.
| Structural Sub-System | Material Specification | Design Function & Failure Mode Prevention | Safety Compliance Code |
|---|---|---|---|
| Continuous Load Rail | Q235B / Q355B High-Yield Cold-Formed Steel (2.0–3.0mm) | Carries bottom pallet timber skids; prevents point deflection and pallet slippage under high dynamic loading. | EN 15512:2020 / RMI MH16.1 |
| Cantilever Support Arm | Heavy Gauge Die-Stamped Welded Steel Bracket (3.5–4.5mm) | Transfers continuous rail loads directly into upright columns; resists downward shear and lateral torsion. | FEM 10.2.02 Standards |
| Upright Column Profile | Omega Profile Cold-Roll Formed (80/90/100/120mm Width) | Supports vertical compressive axial loads; multiple return bends provide high radius of gyration against Euler buckling. | CE No. 2435-CPR-8605159 |
| Top Tie & Portal Bracing | Rectangular Hollow Section (RHS) & C-Channel Structural Bracing | Ties parallel drive-in rows together horizontally; eliminates torsional lane spreading during mast maneuvering. | AS4084-2012 Seismic Rules |
| Ground Guide Rail System | Heavy Inverted Angle Iron (L100x75x6mm) or C-Channel Floor Anchored | Guides forklift steering wheels safely down the center aisle; protects front uprights from direct wheel impacts. | OSHA / SEMA Impact Guidelines |
| Seismic Heavy Baseplates | Laser-Cut Steel Plate (10–16mm) with M16 Anchor Studs | Distributes vertical rack deadweight and seismic overturning moments into reinforced concrete floor slabs. | Eurocode 8 Seismic Engineering |
When procuring high-density drive-in pallet racking, purchasing direct from our certified manufacturing facility in Haizhu District, Guangzhou gives project managers, developers, and 3PL contractors uncompromised engineering accountability, lower freight landed cost, and strict quality control.
Over a quarter century of specialized storage manufacturing in South China. HEDA has engineered and commissioned over 10,000 warehouse projects globally, bringing proven experience to complex warehouse designs, irregular structural column grids, and sub-zero cold room environments.
Never purchase from a catalog blind. Our bilingual engineering design division creates full AutoCAD building layouts, 3D photorealistic renderings, and structural loading calculation packages within 24 to 48 hours completely free of charge before any contract signing.
Backed by international testing body certification including European CE (Certificate No. 2435-CPR-8605159) and ISO 9001:2015 (No. 18624Q00169R0M). Every batch undergoes rigorous raw steel coil tensile testing, weld penetration checks, and dynamic drop testing.
From automated coil decoiling, precision continuous roll-forming, computerized CNC column punching, robotic beam welding, down to chemical pickling, phosphating pre-treatment, and RoHS-compliant electrostatic powder coating, every stage is executed in-house in Guangzhou.
Direct proximity to Guangzhou and Shenzhen deep-water ocean ports allows swift ocean vessel dispatch across ASEAN (Singapore, Malaysia, Thailand, Vietnam, Indonesia), Middle East (UAE, Saudi Arabia), and North America with customized container packing plans that slash freight charges.
We partner with regional warehouse equipment dealers, integrators, and project contractors worldwide, delivering custom punch patterns, bespoke color codes (RAL standards), private branding labels, and on-site or video-based installation engineering supervision.
Industrial warehousing is undergoing rapid structural changes driven by urban land scarcity, soaring industrial square-foot leasing rates, and surging sub-zero cold chain logistics for pharmaceuticals and perishable food chains.
With chilled warehouse energy costs exceeding standard ambient facilities by 400% to 600%, modern cold storage facility procurement teams are systematically transitioning from standard selective racking to drive-in and radio shuttle systems. Drive-in configurations decrease the cubic refrigeration space wasted on access aisles, dropping kilowatt-hour consumption per stored pallet position by up to 35%.
Forward-thinking racking factories now engineer dual-purpose cold-formed rail geometry. Facilities can begin with cost-effective manual drive-in forklift operations and later snap in semi-automated 4-way radio shuttles directly onto the pre-existing continuous rail ledges without tearing down or replacing the primary structural upright columns.
Transition cycles between cold rooms (-25°C) and staging docks frequently induce severe condensation on steel components, sparking rapid micro-pitting corrosion. HEDA Shelves leads this technological response by implementing multi-stage chemical zinc-phosphate immersion pre-treatment followed by thermosetting polyester nanotech powder coating, delivering 1,000+ hours of continuous salt-spray resistance.
In earthquake-prone regions such as Japan, the Philippines, Indonesia, and the US West Coast, municipal building codes enforce stringent non-linear time-history analysis for warehouse racking. Today's drive-in systems incorporate heavy cast steel anchor shoes, baseplates with slotted dampening isolators, and heavy wrap-around polyurethane column armors that absorb dynamic mast impacts without structural buckling.
Detailed, expert-level technical answers addressing the critical structural, economic, and operational questions asked by warehouse engineers, supply chain vice presidents, and international procurement officers before issuing a purchase tender.
Are you planning a new cold chain warehouse, expanding an existing industrial facility, or evaluating high-density storage alternatives? Connect directly with Guangzhou HEDA Shelves' senior structural design engineers. We will analyze your pallet dimensions, forklift lift mast clearances, and building column grid to provide a comprehensive CAD layout and factory quotation.