[email protected] Serving Southeast Asia, South Asia & the Middle East
EN
Direct Factory Engineering · Guangzhou Plant

OEM/ODM Carton Flow Racking Manufacturer & Suppliers

High-precision dynamic gravity feed roller racking, engineered for zero-defect First-In-First-Out (FIFO) split-case picking, dense e-commerce fulfillment, and seamless intralogistics conveyor integration.

Catalog Showcase

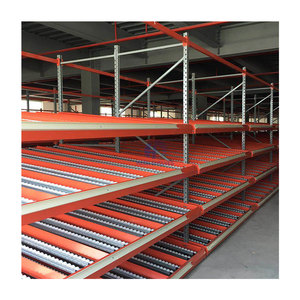
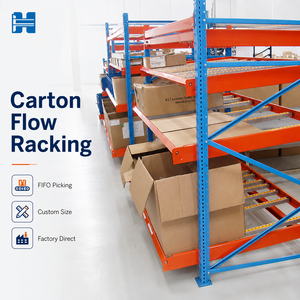
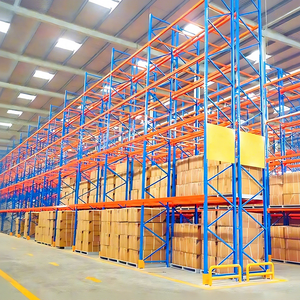
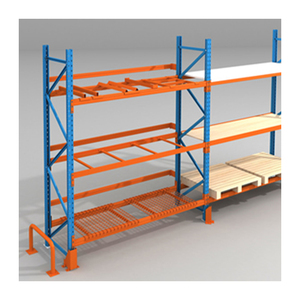
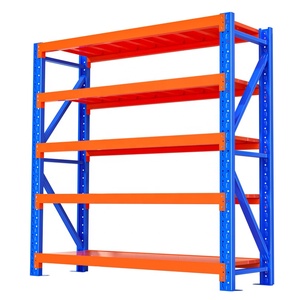
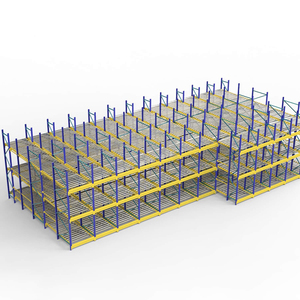
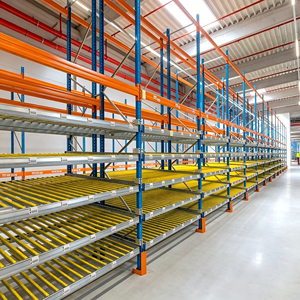
Engineered Carton Flow & Heavy-Duty Storage Configurations

Precision-stamped roller beds, cold-formed Q235B upright frames, and modular ergonomic tilt shelves built to exact custom client dimensions and high-throughput distribution standards.

Engineering Whitepaper

The Mechanics of Gravity Dynamic Storage: Kinematics & Structural Design

How precision incline geometry, roller inertia control, and dynamic bed deflection tolerances eliminate friction stalls, preserve corrugated packaging integrity, and double picking throughput.

Physics-Driven Incline Angle & Roller Bed Calibration

In high-density dynamic storage, gravity serves as an unpowered, zero-emission propulsion system. However, uncontrolled gravitational acceleration causes packaging compression damage and conveyor logjams, while insufficient incline produces friction stall. Guangzhou Heda Shelves engineers calculate the incline angle ($\theta$) dynamically based on package weight ($W$), substrate kinetic coefficient of friction ($\mu$), and contact surface stiffness:

Standard Operating Incline: 2.5° to 4.5° (approx. 4.5% to 7.8% gradient).
• Smooth molded plastic totes (PP/HDPE): 2.5° – 3.0°
• Double-wall corrugated cartons: 3.2° – 3.8°
• Recycled fibrous pulp or heavy sagging containers: 4.0° – 4.5°

Our patented roller tracks utilize precision-machined, high-impact polycarbonate wheels or stamped galvanised steel rollers mounted on continuous zinc-plated axles. Wheel pitch (center-to-center distance) is determined by ensuring that a minimum of three roller axles continuously support the bottom profile of the smallest carton along the track. This prevents carton belly-sagging, eliminates dynamic drift, and guarantees absolute line-tracking straightness without skewing.
Dynamic Kinetic Parameters

Key engineering variables validated through simulated cycle-testing across 50,000 continuous meters of travel:

  • Roller Axle Deflection Rating: Max L/350 under dynamic load
  • Wheel Bearing Friction Factor: $\mu_k \le 0.015$ with sealed ball bearings
  • Impact Drop Bed Rating: Resists 50 kg localized point load impact
  • Thermal Operating Window: -30°C cold room to +60°C dry heat
  • Coating Abrasion Resistance: ASTM D4060 Taber Index < 35mg

Structural Frame Geometry

Cold-formed omega-profile upright columns (55×47mm, 60×50mm, or 80×60mm) stamped with 50mm teardrop or butterfly pitches, yielding uncompromised vertical adjustability and exceptional torsional rigidity.

  • High-strength certified Q235B steel
  • Integral beam connectors with safety locks
  • Floor anchor base plates with seismic slots

Strict FIFO Stock Control

Rear loading aisles and dedicated front discharge pick-faces establish an unbreachable First-In-First-Out material flow, eliminating expired inventory batch bottlenecks in food, pharmaceuticals, and cosmetics.

  • Complete separation of replenisher & picker
  • Guaranteed batch traceability compliance
  • Reduces cross-aisle forklift hazards by 70%

Full-Lane Reconfiguration

Universal snap-in full-depth steel lane dividers and aluminum alloy guide channels enable warehouse managers to modify lane widths within minutes to match changing SKU dimensions without tools.

  • Adjustable lane dividers in 10mm increments
  • Universal compatibility with totes and cartons
  • Integrated entry guide ramps for blind loading

Ergonomic Tilt Shelves

Front-facing presentation pick-trays tilt at an angle of 5° to 15°, exposing carton contents directly to the operator's eye line to slash order-picking travel steps and repetitive bending strain.

  • Optimized for split-case & piece-picking
  • Seamless integration with Pick-to-Light (PTL)
  • Conforms to ISO 6385 human factors norms
Technical Evaluation

Static Shelving vs. Dynamic Carton Flow: Performance Comparison

An empirical comparison of warehouse density, labor efficiency, travel distance, and inventory rotation between conventional multi-tier static shelving and dynamic carton live storage systems.

Evaluation Parameter Conventional Static Shelving HEDA Dynamic Carton Flow Racking Operational Gain / Advantage
Picking Walk Distance 120 – 180 meters per 100 picks 35 – 55 meters per 100 picks 65% to 75% Reduction in Picker Travel
Floor Space Utilization 35% – 45% (Aisle-heavy footprint) 70% – 82% (Compact depth buffering) Up to 2.2x SKU Capacity per m²
Stock Rotation Fidelity Manual Last-In-First-Out (LIFO) risk Strict Automatic Gravity FIFO Eliminates batch obsolescence & spoilage
Replenishment Interference Shared pick/restock aisle congestion Segregated front pick & rear load aisles Zero downtime during active order-picking shifts
Pick Cycle Velocity 40 – 70 lines per picker/hour 140 – 220 lines per picker/hour Over 200% Productivity Surge
Digital Automation Readiness Complex barcode search / manual paper Ready for Pick-to-Light, Put-to-Light & AMRs Plug-and-play mountings for IoT picking bars

Need a Custom Layout & Static-to-Dynamic Conversion Audit?

Our Guangzhou engineering department provides free 2D CAD floor plans, 3D renderings, and pallet/carton position throughput calculations within 24 to 48 hours.

Get a Quote
Strategic Forecasting

2025–2030 Procurement Trends in Dynamic Carton Storage

Macro developments shaping industrial warehouse design, intralogistics capital allocation, and supply chain procurement over the coming decade.

AMR & Cobot Fleet Convergence

Autonomous Mobile Robots (AMRs) are increasingly deployed along carton flow pick-faces. Modern procurement contracts demand lower beam clearances, recessed baseplates, and automated roller-stop interfaces to accommodate robot vision sensors and automated loading claws.

  • Low-profile ground-level roller levels
  • QR-code and optical guidance alignment slots
  • Zero-backlash front stop tolerances

Plug-and-Play Pick-to-Light (PTL) Trays

Supply chain operators are transitioning from standalone racks to smart carton flow racks with pre-engineered raceways, power bus conduits, and snap-in clip brackets for Pick-to-Light LED modules, eliminating on-site drilling and hazardous loose cabling.

  • Pre-punched channel wire management
  • Modular brackets for all major PTL hardware
  • Accelerates picker accuracy to 99.98%

Cold-Chain Food & Pharma Resilience

With the rapid growth of refrigerated e-grocery and temperature-controlled biologics, carton flow systems are increasingly installed in -25°C to -30°C blast freezer settings, demanding low-temperature impact polyolefins and corrosion-resistant galvanizing.

  • Non-brittle low-temperature polymer rollers
  • Hot-dip galvanized (HDG) or zinc phosphate base
  • Low-viscosity synthetic axle lubricants
Manufacturing Authority

Guangzhou HEDA Shelves: 25 Years of OEM/ODM Manufacturing Excellence

Founded in 2001, Guangzhou Heda Shelves Co., Ltd. operates a vertically integrated 30,000 square meter industrial manufacturing plant, delivering international-standard logistics equipment to over 120 countries worldwide.

2001
Year Established in Guangzhou
30,000 m²
Modern Production Facility
30,000 Tons
Monthly Rolling Output
10,000+
Global Projects Completed

10-Step Full-Cycle In-House Manufacturing & Quality Control

01

Raw Material Sourcing

Strict spectral and tensile testing of certified Q235B high-grade hot and cold-rolled steel coils.

02

Precision Shearing

CNC slitting and micro-tolerance shearing lines ensuring straight edge squareness within ±0.2mm.

03

Automated CNC Punching

Multi-station automated hydraulic presses punch teardrop and butterfly pitch patterns at exact 50mm intervals.

04

Continuous Roll-Forming

Advanced multi-pass cold roll-forming lines bend uprights and beams without structural stress fractures.

05

Robotic MIG Welding

High-precision automated robotic arms weld beam-end connectors with zero porosity and deep penetration.

06

Chemical Degreasing

Submersion degreasing tanks eliminate all residual machining oils and surface particulates.

07

Pickling & Phosphating

Acid pickling and zinc phosphate bath pretreatment builds an anti-rust micro-crystalline adhesion substrate.

08

Electrostatic Coating

Automatic electrostatic powder coating spray booth coats steel with durable, impact-resistant epoxy-polyester resin.

09

Thermal Oven Curing

Gas-fired curing at 180°C to 200°C ensures complete cross-linking, curing thickness of 60–80 microns.

10

Inspection & Container Packing

Laser dimension checks, cross-hatch adhesion testing, and containerized wooden pallet sea-freight packing.

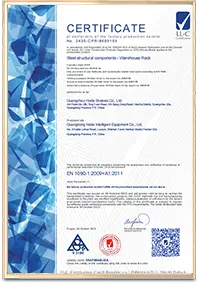
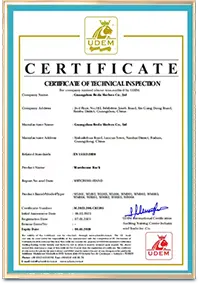
Certified Compliance for Global Tenders

Our manufacturing processes adhere to European FEM, American RMI, and international ISO quality and structural safety parameters.

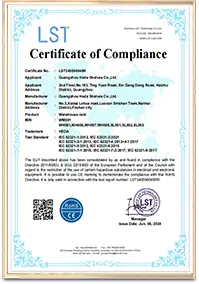
CE Certificate No. 2435-CPR-8605159 CE Cert: 2435-CPR-8605159
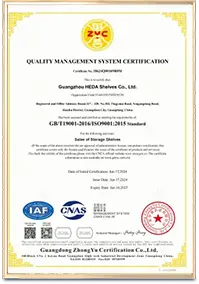
ISO 9001:2015 Certificate No. 18624Q00169R0M ISO 9001:2015 Management
RoHS Environmental Compliance Certificate RoHS Eco-Coating Certified
Structural Load Test & Inspection Report Structural Deflection Reports
Procurement FAQ

Frequently Asked Questions by Industrial Warehouse Buyers

Key technical, logistical, and structural questions addressed directly by our senior structural racking engineers.

What calculations determine roller track pitch and slope angle for our specific boxes?
The track incline and roller pitch are governed by the substrate stiffness of the container bottom and the gross package weight. Our baseline standard requires that the smallest carton bottom is supported by at least three consecutive roller axles at all times. For instance, if your shortest carton is 200mm deep, roller axle spacing must not exceed 66mm (we recommend 38mm or 50mm pitch). The slope angle is calibrated between 2.5° and 4.5°. For corrugated fiberboard prone to moisture absorption, we increase the angle to 3.5°–4.0° to overcome packaging sag friction, and integrate impact drop plates at the rear loading zone to absorb vertical shock during manual or automated loading.
Can carton flow bed levels be retrofitted into existing selective pallet racking?
Yes, absolutely. HEDA Shelves manufactures universal hanger brackets and conversion cross-beams that hook directly onto third-party teardrop, diamond, or conventional European pallet rack uprights. This allows logistics operators to transform the ground and lower levels of existing pallet racks into dynamic split-case carton flow picking tunnels while retaining upper pallet beam levels for reserve overstock bulk pallet storage. This hybrid setup drastically reduces order-picker travel time without requiring a complete warehouse teardown.
What are the load-bearing capacities for OEM/ODM carton flow tracks and levels?
Standard light-duty carton flow tracks support 25 to 50 kg per linear meter, tailored for light pharmaceutical boxes, apparel cartons, and small parts bins. Our industrial heavy-duty series features reinforced cold-formed steel side channels and high-grade aluminum track extrusions supporting up to 150 to 250 kg per linear meter (or up to 1,500 kg uniformly distributed load per complete flow level). If your operations handle high-density metal components, casting hardware, or liquid jugs, we engineer heavy-gauge steel full-width roller tracks with solid turned steel axles.
How does HEDA prevent carton hang-ups, lane crossing, and container drift?
We employ full-depth, full-height galvanised sheet metal lane dividers that physically isolate each carton SKU channel from loading entry to front discharge pick-face. Unlike simple plastic clip-on guides, our steel lane dividers mechanically lock into the front and rear cross-beams, preventing deflection when operators load skewed cartons. Furthermore, entry guide plates flared at 15 degrees funnel cartons smoothly into their dedicated tracks even during rapid, blind loading.
What protective surface treatments are available for tropical or cold-room environments?
In our Guangzhou manufacturing plant, every steel component undergoes an automatic 8-stage pre-treatment cycle consisting of alkali degreasing, water rinsing, acid rust pickling, and zinc phosphating prior to electrostatic powder deposition. For high-humidity tropical sites (such as Southeast Asia), our epoxy-polyester coatings exceed 500 hours of continuous salt-spray testing. For sub-zero cold chain freezers (-30°C) or coastal chemical hubs, we offer full hot-dip galvanizing (HDG) to EN ISO 1461 standards, ensuring zero rust bloom, coating peel, or embrittlement over decades of use.
What export packing standards and technical documents are provided for shipping?
Every export shipment is packaged to prevent maritime damage: uprights and beams are strapped in custom timber bunks with corrugated cardboard cushioning, protective PE stretch film, and steel corner protectors. Small components, roller tracks, dividers, and hardware are crated in seaworthy, fumigated plywood cases. Full documentation includes itemized container loading plans, exploded 3D assembly schematics, mill material test certificates, CE compliance declarations, and structural load charts stamped by our senior engineering team.
Direct Guangzhou Factory Communication

Request an OEM/ODM Carton Flow Racking Proposal

Connect directly with our Guangzhou design engineering team. Provide your warehouse dimensions, carton dimensions, weight loads, and SKU counts to receive custom 2D/3D CAD layouts and competitive factory-direct pricing within 24 hours.