Heavy Storage
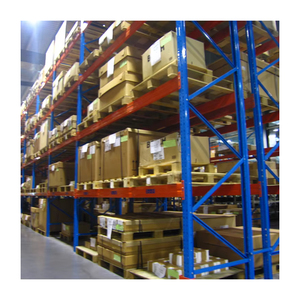
Heavy Duty Rack Steel Warehouse Rack Industrial Pallet Storage Shelf
- Capacity: 1,000 – 4,500 kg / level
- Steel Grade: High Tensile Q235B
- Configuration: Boltless 75mm/50mm Pitch
Explore our precision-fabricated warehouse systems. Each product is custom roll-formed from premium certified structural steel (Q235B / Q355B) and tailored to exact pallet footprints, weight ratings, and material handling clearances.
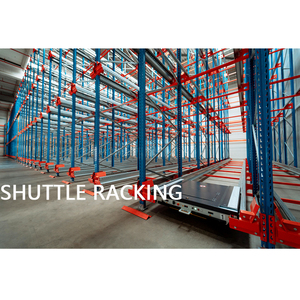
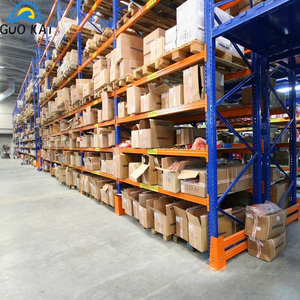
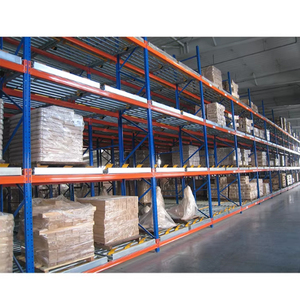
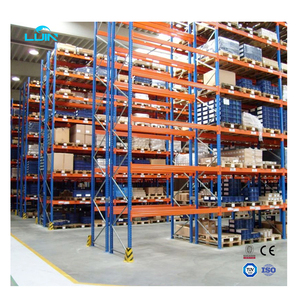
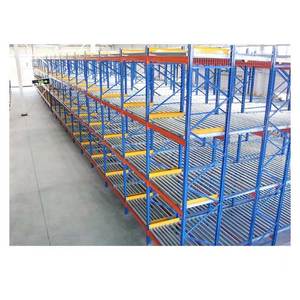
Push back pallet racking is a dynamic accumulator storage solution combining the ultra-high space density of drive-in racking with the operational velocity and single-aisle selectivity of live gravity flow systems. As an OEM and ODM tier-one factory, we configure push back systems that maximize usable cubic volume while protecting sensitive product packaging from forklift mast contact.
Structural Principle of Dynamic Push Back Systems: Pallets sit atop a series of nested rolling carts that glide smoothly along inclined structural steel guide rails. The first pallet is positioned on the top cart by a forklift. When loading the second pallet, the operator pushes the first pallet backward, exposing the underlying second cart. Upon pallet retrieval, the hydraulic/gravitational forces gently glide trailing carts forward to the aisle face at a controlled speed, eliminating the necessity for forklifts to enter storage lanes.
In conventional high-density block storage or drive-in racking, structural damage frequently occurs due to mast impacts inside narrow aisles. Push back systems mitigate 95% of this operational risk because the forklift truck mast remains entirely in the main aisleway. The critical engineering design challenge lies in managing the kinetics of gravity-assisted descent and dynamic rolling resistance.
Our OEM engineering group utilizes precise 1.5% to 2.8% rail gradients (adjusted according to ambient warehouse temperatures, lubricant viscosity, and pallet base material properties). Low profiles ensure vertical clear-height conservation, allowing facilities to incorporate up to 5 or 6 tiers of vertical storage within standard 10-meter ceiling heights. Each nested cart features low-flange steel wheels fitted with sealed, precision-ground dual ball bearings engineered to perform reliably under continuous heavy dynamic loads from -30°C cold chain conditions to +45°C ambient tropical warehousing.
| System Type | Storage Depth | Standard Rail Slope | Max Unit Load / Pallet | Recommended Forklift | Access Methodology |
|---|---|---|---|---|---|
| 2-Deep Nesting | 2 Pallets Deep | 1.50% - 1.75% | 500 - 1,800 kg | Standard Counterbalance / Reach | LIFO (Last-In, First-Out) |
| 3-Deep Multi-Cart | 3 Pallets Deep | 1.75% - 2.00% | 500 - 1,600 kg | Standard Reach Truck | LIFO (Last-In, First-Out) |
| 4-Deep Heavy Lane | 4 Pallets Deep | 2.00% - 2.25% | 500 - 1,500 kg | Heavy-Duty Reach / Counterbalance | LIFO (Last-In, First-Out) |
| 5-Deep High-Density | 5 Pallets Deep | 2.25% - 2.50% | 500 - 1,400 kg | Counterbalance with Precision Mast | LIFO (Last-In, First-Out) |
| 6-Deep Deep-Lane OEM | 6 Pallets Deep | 2.50% - 2.80% | 500 - 1,250 kg | Laser-Guided High Capacity Truck | LIFO (Last-In, First-Out) |
Procuring push-back racking requires evaluating floor square meterage against product turnover velocities. We offer three primary configurations for industrial material handlers:
Designed specifically for brownfield facilities with constrained clear building heights. Low profile nested carts yield up to 150mm additional vertical storage clearance per bay level.
Engineered for -30°C operations. Fabricated with low-temperature impact resistant steels, synthetic cryo-lubricants, and zinc-rich coatings to resist condensation corrosion.
Combines multi-tier push-back upper storage with lower-level carton flow or selective pick tunnels, perfectly serving FMCG operations balancing reserve bulk and unit picking.
Built for structural industrial applications, such as automotive press tooling, cast iron fittings, and dense metal parts with loads exceeding 1,800 kg per pallet position.
The global warehousing landscape is undergoing unprecedented transformation. As industrial land values escalate across major metropolitan supply chain centers in Southeast Asia, the Middle East, Europe, and the Americas, warehouse planners are shifting from standard selective racks to dynamic high-density systems. Below are the key procurement trends dominating industrial requests:
1. Convergence of Pallet Shuttle Automation with Push Back Arrays: Enterprise 3PLs are demanding hybrid storage matrices. While automated 4-way shuttle systems excel in deep-lane bulk replenishment, push-back racking is increasingly integrated along front picking walls to handle fast-moving buffer stock without electrical consumption or software dependencies.
2. Modular Pre-Assembled Track Cassettes: International buyers are transitioning from field-assembled structural angles to factory pre-assembled, welded cassette subassemblies. By manufacturing push back track modules with precision robotic welding fixtures at our Guangzhou plant, container packing is optimized by 35%, and on-site assembly time is slashed by more than half.
3. Rigorous Life-Cycle Fatigue Testing (FEA & Cyclic Impact Testing): Enterprise buyers now mandate finite element stress analyses (FEA) validating dynamic cart impact resistance, anti-derailment interlocks, and pallet centering bevels that accommodate imperfect or warped pallets safely.
4. Decarbonized Steel Sourcing & Eco-Certified Coatings: Procurement standards increasingly require RoHS-compliant polyester coatings with near-zero volatile organic compounds (VOCs) and verified low-carbon steel billets trace-certified from raw melt to cold roll-forming.
Over the past two decades, push back racking technology has evolved from primitive channel-iron frames with sleeve bearings into sophisticated, mathematically optimized material handling machinery. Notable innovations developed in our manufacturing facility include:
Founded in 2001 in Guangzhou, China, Guangzhou Heda Shelves Co., Ltd. has established itself as an authoritative manufacturer of commercial and industrial warehousing systems, maintaining end-to-end control from raw steel sourcing to finished, painted assemblies.
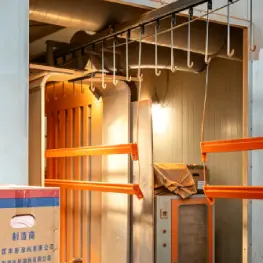
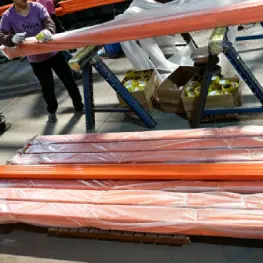
In-house manufacturing guarantees strict dimensional tolerances (±0.5mm on punched upright centerlines) and coating durability capable of passing 500-hour continuous salt spray testing. Our verified manufacturing flow includes:
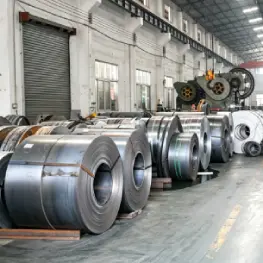
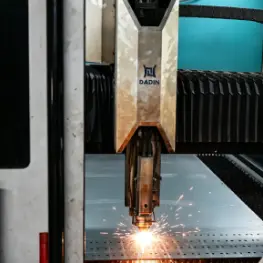
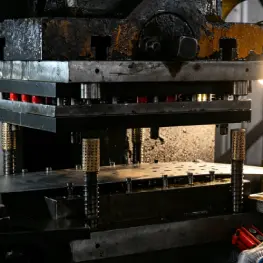
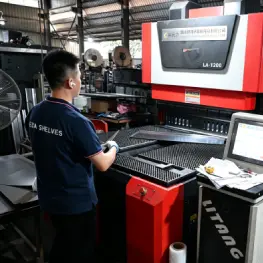
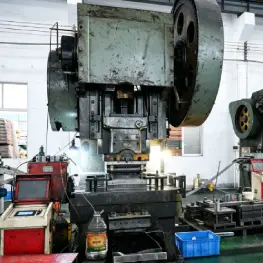
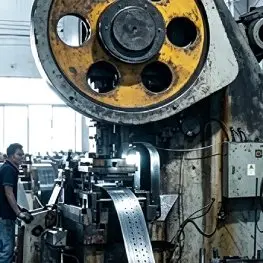
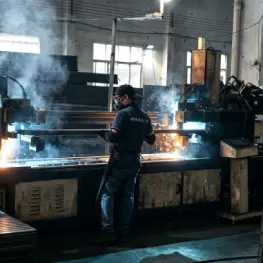
International Quality Certifications & Seismic Design Compliance: All manufactured racking configurations adhere to European Standard EN 15512 and American RMI MH16.1 specifications. Guangzhou Heda Shelves holds CE Certification (No. 2435-CPR-8605159), ISO 9001:2015 Quality Management Certification (No. 18624Q00169R0M), and verified RoHS environmental compliance. For projects located across seismically active regions—including the Philippines, Indonesia, Japan, and the Western United States—our structural engineers calculate regional ground acceleration coefficients (Ss and S1), providing full FEA structural review reports and PE stamping upon request.
Key technical, logistical, and architectural answers compiled directly from our factory engineering desk to guide global procurement managers.
Connect directly with our Guangzhou factory engineering team. Send your warehouse floor plan, ceiling clear heights, and pallet specifications to receive a complimentary 2D CAD layout, 3D visualization, and structural load analysis within 24 to 48 hours.
Instant live chat support for global distributors, logistics operators, and project engineers.
Get a Quote