Engineered Heavy-Duty Pallet Rack Systems
Precision-manufactured from certified Q235B and Q355B structural coil steel. Each configuration accommodates specific material handling equipment (MHE), pallet density ratios, and unit load safety protocols.
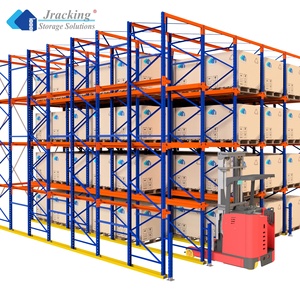
Heavy Duty Industrial Selective Pallet Racking System CE Certified
- Load Capacity: 1,000 - 4,500 kg / level
- Steel Grade: Q235B / Q355B Cold Formed
- Pitch Adjustability: 50mm / 75mm Connector
- Standard Finish: Polyester Powder (60-80μm)
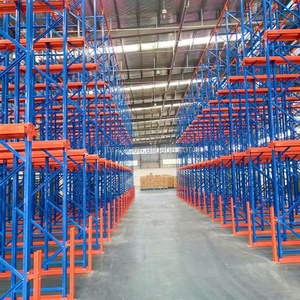
Industrial Drive-In Pallet Racking System for Chemical Warehousing
- Storage Mode: FILO / FIFO High-Density
- Pallet Depth: Up to 12 Pallets Deep
- Support Rails: Formed Structural Steel
- Corrosion Shield: Anti-Chemical Epoxy Coat
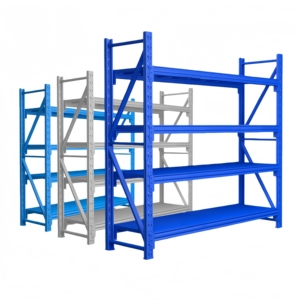
Anti-Rust Adjustable Through-Type Heavy Steel Storage Racks
- Corrosion Rating: C3/C4 Pre-treatment
- Upright Profile: Omega 90/100/120mm
- Application: Commercial Hubs & Yards
- Safety Lock: Integral Spring Lock Pins
1000 kg / Layer Cold Storage Heavy Duty Pallet Rack System
- Temp Tolerance: -35°C to Ambient
- Impact Test: Charpy V-Notch Qualified
- Protection: Heavy Galvanized / Epoxy
- Aisle Width: Reach Forklift Optimized
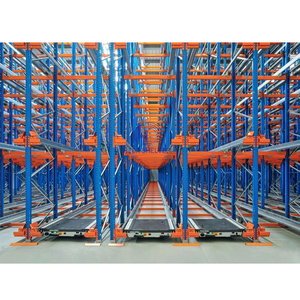
High-Density ASRS 4-Way Radio Shuttle Automated Racking System
- Automation Level: Semi / Full ASRS Interface
- Carrier Speed: 1.0 m/s Loaded, 1.2 m/s Empty
- Track System: Precision CNC Cold-Rolled
- Operation: WCS / WMS RF Control
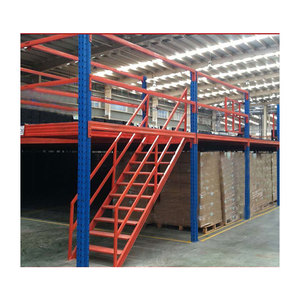
Multi-Tier Heavy Duty Pallet Rack-Supported Mezzanine Platform
- Deck Loading: 300 - 1,200 kg / m²
- Flooring Type: Perforated Steel / B-Deck
- Tier Options: 2, 3, or 4 Levels
- Accessories: Staircases, Kickplates, Gates
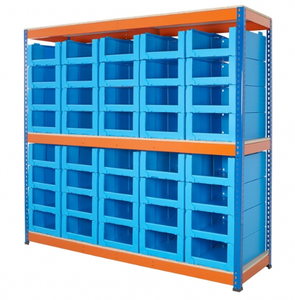
Stackable PP Corrugated Small Parts Pick & Sorting Storage Bins
- Material: 100% Virgin PP Copolymer
- Design: Semi-Open Hopper Front
- Stackability: Self-Locking Modular Ribs
- Resistance: Oils, Solvents & Moisture
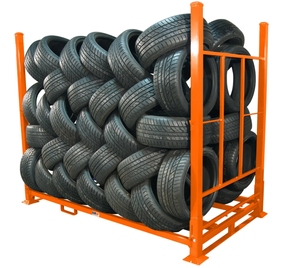
Portable Heavy Duty Steel Warehouse Nestable Stacking Post Racks
- Unit Capacity: 1,000 - 2,000 kg / base
- Tier Stacking: 4 - 6 Units High
- Fork Access: 4-Way Entry Welded Pockets
- Space Saving: Demountable / Nestable
Why Global Supply Chains Engineer with HEDA Shelves
Established in 2001 in Guangzhou, China, Guangzhou Heda Shelves Co., Ltd. controls the complete supply chain loop—from primary steel slitting to robotic profile forming and global freight container optimization.
Fully Integrated Guangzhou Plant
Our 30,000 m² heavy manufacturing facility operates 16 continuous automated roll-forming lines, automated punch presses, and multi-axis welding robots producing over 30,000 tons per month with strict gauge tolerances.
Free 2D CAD & 3D BIM Design
Within 24–48 hours, our structural engineering team delivers comprehensive layout schematics, pallet clearance analysis, and volumetric optimization models aligned with your specific forklift turn radii and building codes.
CE & ISO 9001:2015 Compliance
Third-party verified under CE Certificate No. 2435-CPR-8605159 and ISO 9001:2015 (Certificate No. 18624Q00169R0M). Every structural beam and upright is stamped, batch-traceable, and accompanied by Mill Test Certificates (MTC EN 10204 Type 3.1).
South China Port Proximity
Located in Guangzhou near Nansha and Huangpu ports, we consolidate heavy freight into 40ft HQ containers with custom steel framing. Short transit times directly serve ASEAN, South Asia, the GCC, and European maritime routes.
The 10-Stage Precision Manufacturing & Surface Treatment Protocol
Raw Material Verification
Spectrographic analysis of prime Q235B/Q355B coil steel verifying tensile strength, elongation, and yield points.
CNC Precision Slitting
Automated uncoiling and laser width slitting with ±0.1mm strip tolerances ensuring flawless profile consistency.
Continuous Column Punching
High-tonnage hydraulic multi-die punching maintaining 50mm/75mm diamond or teardrop pitch pitch center precision.
Cold Roll Forming
18 to 24 progressive roll stations cold-form complex omega and box-beam cross-sections with maximum structural rigidity.
Laser Cutting & Trimming
Fiber laser profiling for beam connection hooks, endplates, and safety connector locks ensuring pin-drop fitment.
Robotic CO2 Arc Welding
Panasonic robotic arc welding cells bond beam connectors with full-penetration structural welds tested for shear fatigue.
9-Stage Chemical Pre-Treatment
Full dip immersion: hot alkaline degreasing, acid pickling, rinsing, neutralizing, and nano-ceramic/phosphate conversion.
Electrostatic Powder Coating
GEMA automatic spray booths apply lead-free polyester thermosetting powder with uniform 60–90 μm thickness.
High-Temp Tunnel Curing
200°C convection baking polymerizes the powder into an ultra-tough, impact-resistant, cross-hatch tested anti-corrosive skin.
CMM QA & Export Packaging
Laser dimensional checks, drop impact tests, and air-cushioned steel banding inside export crates to prevent sea-freight abrasion.
Strategic Procurement Trends in Warehouse Racking (2025–2030)
Sourcing industrial storage is evolving rapidly from simple commodity procurement into engineering risk management. Smart operators prioritize automated integration, lifecycle decarbonization, and seismic resilience.
1. Accelerated Automation & Pallet Shuttle Readiness
Procurement teams are shifting capex from wide-aisle static racking to hybrid shuttle-ready rails. Racks manufactured today are specified with tight deflection tolerances (≤ L/250) to allow retrofitting 2D/4D radio shuttles without altering primary upright uprights or slab footings.
2. Seismic Qualification & Finite Element Verification
With massive logistics expansions in earthquake zones across Indonesia, the Philippines, Japan, and the Middle East, structural purchase orders now demand dynamic FEA (Finite Element Analysis) simulation reports confirming seismic response factors according to Eurocode 8 and RMI MH16.1 standards.
3. ESG, Carbon Border Audits & Sustainable Coatings
Multinational 3PLs and Fortune 500 manufacturers demand low-VOC, heavy-metal-free thermoset powder coats meeting RoHS and REACH guidelines. Furthermore, procurement policies require suppliers to provide certified steel sourcing traceability to quantify embedded carbon per pallet position.
4. Total Cost of Ownership (TCO) vs Initial Freight Rate
Savvy global purchasers analyze total landed cost rather than FOB unit weight. Nestable post geometries, high-density nesting column sections, and knock-down bolted frames reduce required shipping containers by up to 25%, offsetting volatile ocean freight rates.
5. High-Yield Metallurgy to Mitigate Building Load
The industry is transitioning from standard Q235B (235 MPa yield) toward advanced micro-alloyed Q355B (355 MPa yield). Higher tensile properties permit thinner gauge steel profiles with equal or superior buckling limits, minimizing dead-weight slab loading on upper mezzanine platforms.
6. Direct-to-Factory Engineering Collaborations
Middlemen are increasingly bypassed in favor of direct collaboration between warehouse systems integrators and primary China manufacturers. Real-time CAD iteration via BIM models accelerates approval times from weeks to hours.
Industrial Pallet Racking Comparative Engineering Matrix
Select the optimal structural configuration based on SKU selectivity requirements, floor space utilization percentages, and material handling capital expenditure.
| Racking System | Direct Selectivity | Floor Utilization | Optimal Handling Equipment | Standard Unit Capacity | Typical Industry Deployment |
|---|---|---|---|---|---|
| Selective Pallet Racking | 100% (Immediate access) | 35% - 40% | Counterbalanced / Reach Truck | 1,000 - 4,500 kg / level | FMCG, 3PL Distribution, General Retail |
| Drive-In / Drive-Through | 15% - 20% (FILO / FIFO) | 65% - 75% | Counterbalanced / Narrow Reach | 1,000 - 2,000 kg / pallet | Cold Storage, Beverage, Seasonal Bulk |
| Radio Shuttle Automation | High by Lane (FILO/FIFO) | 75% - 85% | Standard Forklift + Automated Shuttle | 500 - 2,000 kg / pallet | Food Production, Deep Chill, Pharma |
| Gravity Pallet Flow | 100% per Lane (Strict FIFO) | 60% - 70% | Standard Reach / Counterbalance | 500 - 1,500 kg / pallet | Perishables, High-Throughput Buffers |
| Push-Back Cart System | Medium (2-6 Pallets Deep) | 55% - 65% | Standard Counterbalance | 1,000 - 1,500 kg / pallet | Manufacturing Staging, Buffer Warehouses |
| Rack-Supported Mezzanine | 100% Split Multi-Tier | Up to 200% Floor Gain | Pallet Jacks, VRC, Man-Up Pickers | 300 - 1,000 kg / m² Floor | E-commerce Sorting, Auto Spares, Apparel |
Structural Design Codes & Critical Deflection Limits
In heavy-duty warehouse racking design, deflection criteria under safe working loads (SWL) dictate serviceability limits. European standard EN 15512:2020 and American ANSI/RMI MH16.1 establish that the maximum vertical beam deflection (δ) under full uniform static load must not exceed L / 200, where L is the clear span distance between uprights. For automated ASRS and radio shuttle applications, HEDA Shelves enforces an even tighter standard of L / 300 to L / 350 to prevent sensor misalignment or premature brake carriage wear.
Moreover, column baseplates must distribute vertical loads and overturning moment forces safely into the concrete foundation slab. For high-bay installations exceeding 10 meters, floor flatness must conform to DIN 18202 Table 3 Group 4 or Concrete Society TR34 DM1/DM2 specifications to minimize mast sway during maximum reach extensions.
Technical & Commercial Sourcing FAQ
Direct answers to the most common engineering, compliance, and customs questions asked by warehouse directors and international EPC contractors.
Q: What information is required to engineer an accurate CAD layout and price quote?
We require: (1) Warehouse architectural floor plan (DWG or dimensioned PDF) displaying clear heights, column grids, and dock doors; (2) Pallet specifications (width, depth, height, and gross weight including overhang); (3) Forklift model, turning radius, and maximum lift height; (4) Total SKU inventory counts and required FIFO/FILO rotation; (5) Local seismic zone coefficients.
Q: Which steel grades and international mill certifications do you provide?
We source certified structural hot-rolled and cold-rolled coil steels in Q235B (yield strength ≥ 235 MPa) and high-strength Q355B (yield strength ≥ 355 MPa, equivalent to European S355JR or ASTM A572 Grade 50). Full Mill Test Certificates (MTC EN 10204 3.1) detailing carbon equivalents, yield points, and Charpy impact tests accompany every batch.
Q: How does HEDA Shelves engineer racking systems for earthquake-prone zones?
For high seismic regions (such as the Pacific Rim, Indonesia, Philippines, Japan, and parts of the Middle East), we perform structural modal and static equivalent analyses using finite element software. Upright profiles are stepped up in steel gauge, heavy-duty footplates are specified with M16/M20 chemical wedge anchors, and top-tier horizontal/vertical spine bracing frames are added.
Q: What surface finish options prevent rust in humid monsoon or deep freeze environments?
For high-humidity tropical distribution centers, our standard automated 9-stage degreasing and zinc phosphating pre-treatment ensures 500+ hours of ASTM B117 salt-spray corrosion resistance beneath high-adhesion polyester powder coating. For cold storage (-20°C to -35°C) or outdoor coastal facilities, we supply full Hot-Dip Galvanized (HDG) finishes conforming to ISO 1461 with 60–100 μm zinc coatings.
Q: What are your standard manufacturing lead times and container consolidation practices?
Standard lead times range from 15 to 25 days depending on project tonnage. Uprights, step beams, and bracing are nested, steel-strapped, and buffered with protective corner boards. Our factory software creates 3D container packing layouts that maximize 40ft HQ cubic volume (reaching 95%+ fill rates), dramatically reducing maritime freight costs per pallet location.
Q: Do you provide installation guidance and third-party engineer sign-offs?
Yes. Every shipment includes step-by-step 3D assembly guides, part mark drawings, and anchoring torque tables. For large projects, we dispatch certified installation supervisors on-site or support local engineering contractors with real-time video engineering consultations to ensure safe commissioning.
Request Your Custom 2D/3D Warehouse Layout Proposal
Collaborate directly with our Guangzhou factory engineering department. Submit your warehouse dimensions and unit load parameters to receive structural calculations, complete bill of materials (BOM), and factory-direct wholesale pricing within 24–48 hours.
- Free 2D CAD & 3D Modeling
- CE & ISO 9001:2015 Structural Check
- Direct Export Pricing (FOB / CIF / DDP)
- Container Consolidation Optimization
Guangzhou Heda Shelves Co., Ltd. • Direct Factory Floor Support
Send an Inquiry