1. Engineering Foundations: Mechanical & Electrical Architecture of Movable Pallet Racking
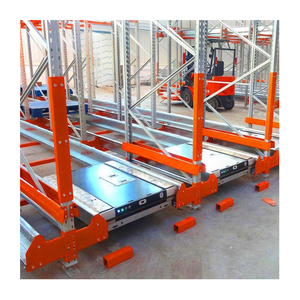
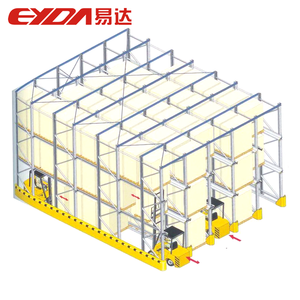
Movable pallet racking systems (often termed Powered Mobile Pallet Racking or MOVO) represent the pinnacle of high-density intralogistics engineering. Unlike conventional static selective racking that requires dedicated access aisles between every storage bay, a movable pallet racking installation mounts industrial superstructure upright frames onto electronically synchronized, motor-driven wheel bogies traveling across recessed guide rails embedded into the concrete slab. This mechanical architecture eliminates static aisles, opening a single floating access aisle on demand via radio frequency (RF), optical sensor activation, or integrated Warehouse Management Systems (WMS). In terms of volume efficiency, mobile pallet racking contracts the total storage footprint by 45% to 50%, or alternatively increases pallet position density within a fixed physical envelope by 80% to 100%.
From an engineering perspective, modern Chinese manufacturing centers such as Guangzhou Heda Shelves Co., Ltd. fabricate heavy-duty mobile carriages utilizing structural steel profiles (Q235B and Q355B cold-formed structural steel) capable of sustaining block loads exceeding 800 metric tons per mobile train. Each movable base incorporates forged steel wheels featuring dual ball-bearing assemblies running on precision-machined, floor-embedded guide and running rails. The mechanical movement is driven by distributed, low-vibration three-phase helical gearmotors with soft-start and soft-stop frequency inverters. This design mitigates dynamic inertia, preventing pallet displacement during rack travel even under maximum design load conditions.
Recessed Guide Rails
Milled flat-head and round-head profile steels anchored with non-shrink high-strength epoxy grouting directly into the structural slab, ensuring smooth forklift crossing without wheel disturbance.
Synchronized PLC Control
Siemens S7-1200 or Schneider centralized controllers communicating across industrial CAN-bus or Profinet protocols to synchronize multi-bogie movement and balance torque load evenly.
SIL-3 Optical Safety
Full-height photoelectric light curtains at aisle entrances, long-range floor-level safety laser bumpers, and manual emergency stop plungers per carriage that halt transit in milliseconds.
2. Global Sourcing Analysis: Why International Buyers Source Movable Racking from China
Procuring heavy industrial movable pallet racking from dedicated Chinese manufacturing plants has evolved from a simple low-cost material sourcing strategy into a comprehensive technical partnership. Global logistics directors, third-party logistics (3PL) providers, and pharmaceutical distribution hubs across Southeast Asia, Europe, South America, and the Middle East prioritize Chinese manufacturers due to integrated supply chain ecosystems, rapid prototype-to-commissioning cadences, and advanced manufacturing automation.
A primary driver is structural steel integration. Facilities such as Guangzhou Heda Shelves Co., Ltd. operate automated cold-roll forming lines linked directly to high-grade domestic hot-rolled steel strip procurement. This vertical synergy shields international buyers from volatile intermediary steel surcharges while enforcing rigorous physical and chemical metallurgy testing. Every steel coil batch undergoes yield strength verification (Q235B ≥ 235 MPa; Q355B ≥ 355 MPa) and elongation testing before slotting into CNC punching lines.
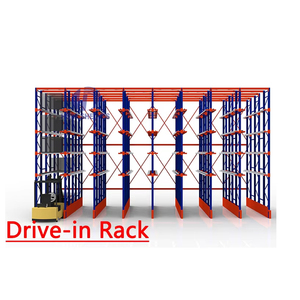
| Evaluation Parameter | Static Selective Pallet Racking | Drive-In Pallet Racking | Movable (Mobile) Pallet Racking | Automated High-Bay AS/RS |
|---|---|---|---|---|
| Warehouse Footprint Utilization | 35% – 40% (Low) | 60% – 65% (Medium-High) | 80% – 85% (Ultra-High) | 85% – 90% (Maximum) |
| Pallet Selectivity / Direct Access | 100% Immediate Access | < 20% (LIFO Honeycomb) | 100% Direct Aisle Access | 100% Automated Retrieval |
| Capital Expenditure (CapEx / Pallet) | Baseline ($35 – $65) | Moderate ($65 – $110) | Competitive ($140 – $220) | Extreme ($600 – $1,200+) |
| Cold Room Energy Efficiency | High Thermal Losses | Moderate Thermal Density | Exceptional (−40% Energy Cost) | Exceptional |
| Forklift Fleet Compatibility | Standard Counterbalance/Reach | Specialized Narrow Reach | Standard Reach Trucks | Captive Automated Cranes |
| Implementation Lead Time | 3 – 5 Weeks | 4 – 7 Weeks | 8 – 12 Weeks (Turnkey) | 9 – 18 Months |
Furthermore, procurement trends in 2026 and beyond emphasize Total Cost of Ownership (TCO). While the initial capital expenditure of powered mobile racking exceeds standard static teardrop or European adjustable pallet racks, the amortization timeline is markedly superior when evaluating land acquisition costs and industrial refrigeration operating expenditures. For temperature-controlled cold chains (−18°C to −28°C), cooling unused cubic air inside empty access aisles represents a massive, non-recoverable operational loss. By clustering pallets into a consolidated, movable block, the required refrigeration cubic volume decreases by up to 40%, generating substantial, measurable electrical cost savings annually.
3. Future Industry Trends: Automation Convergence, IoT Telemetry, and Green Logistics
The movable pallet racking sector is rapidly evolving beyond standalone electromechanical systems into intelligent, data-driven nodes within the broader smart warehouse landscape. Sourcing agents and industrial engineers should evaluate four key developmental vectors currently shaping future factory specifications:
AGV / AMR Fleet Interlocking
Modern mobile racking systems are now natively interfaced with Autonomous Mobile Robots (AMRs) and Automated Guided Reach Forklifts via API/OPC-UA industrial protocols. The warehouse management software automatically opens the designated aisle ahead of the incoming robot's arrival, eliminating waiting latency and achieving lights-out warehouse operations.
Wireless IoT Load Telemetry
Next-generation upright profiles incorporate integrated strain-gauge sensors that transmit continuous load data via wireless mesh networks. If an operator accidentally overloads a beam bay beyond rated design capacity, the system triggers an operational alert and locks the mobile carriage movement to prevent structural buckling.
Regenerative Kinetic Braking
Addressing strict corporate ESG mandates, heavy-duty movable systems are incorporating regenerative variable frequency drives (VFDs). The kinetic deceleration energy produced when halting an 800-ton mobile carriage train is converted into electrical current and routed back into the warehouse power grid rather than dissipated as waste heat.
Additionally, eco-responsible powder coating technology has replaced older solvent-heavy paint finishes. Modern Chinese automated lines utilize solvent-free electrostatic epoxy-polyester powder polymers followed by rigorous gas-fired curing ovens at 200°C. This guarantees salt-spray corrosion resistance exceeding 500 hours (ASTM B117) with zero volatile organic compound (VOC) emissions, complying fully with EU RoHS regulations and global green-building standard credits (LEED v4.1).
4. Enterprise Authority: Guangzhou Heda Shelves Co., Ltd. Manufacturing Advantages
Founded in 2001 and headquartered in the core manufacturing corridor of Haizhu District, Guangzhou, Guangzhou Heda Shelves Co., Ltd. stands as an authoritative leader in high-density storage manufacturing across China and the wider Asia-Pacific region. Over more than two decades of technical evolution, Heda Shelves has grown from a specialized shelving fabricator into an integrated intralogistics system provider with installations operating in over 120 countries worldwide.
Precision In-House Manufacturing Capabilities
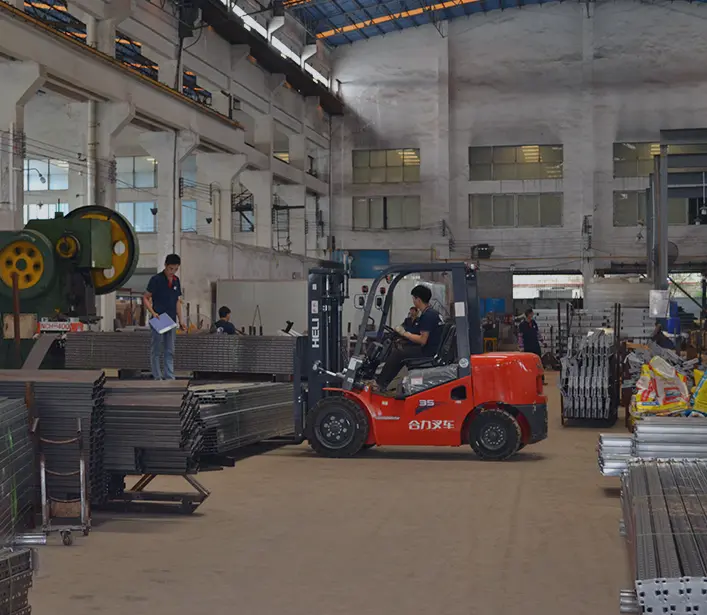
Unlike trading agencies that subcontract fabrication across fragmented workshops, Heda Shelves manages all manufacturing operations within its dedicated 30,000 square meter production facility. The factory houses 14 automated roll-forming lines, computerized continuous punching units, robotic longitudinal beam welding stations, and an environmentally compliant four-stage pre-treatment line (pickling, degreasing, and zinc-phosphating) followed by a Swiss Gema electrostatic powder spray booth.
This end-to-end operational control ensures that cross-section profiles, upright hole pitch consistency (50 mm / 75 mm standard), and connection connector tolerances remain strictly within ±0.3 mm. When configuring massive movable racking bases, this precision prevents structural frame skewing, ensures seamless load distribution across all ground bogies, and drastically reduces on-site erection labor costs.
Seismic-Resilient Engineering & Global Port Logistics
Operating internationally requires strict structural compliance across diverse geological regions. For projects located in high-seismic active belts (including Indonesia, the Philippines, Japan, Taiwan, and coastal South America), Heda Shelves engineers perform static and dynamic finite element analysis (FEA) utilizing SAP2000 and ANSYS software. Our engineering department calculates structural node ductility, dynamic base shear, and second-order P-Delta effects, sizing enlarged heavy-duty base plates, reinforced frame portal bracing, and seismic anti-tip floor interlocks accordingly.
Strategically situated adjacent to Guangzhou, Shenzhen, and Hong Kong deep-water ports, Heda Shelves provides streamlined international container loading (20GP, 40GP, 40HQ, 45HQ, and flat-rack options). Components are bundled into custom steel-cradled transport frames with heavy poly-film wrapping and desiccant arrays to prevent moisture corrosion during ocean transit. Complete container stuffing diagrams and color-coded mark lists accompany all export documentation, simplifying site staging and unpacking for local installation teams.
5. Critical Procurement FAQ: Technical Specifications & Commercial Terms
Sourcing movable pallet racking involves precise mechanical, civil, and electrical criteria. Below are expert engineering responses to the most critical technical questions submitted by corporate procurement directors and facilities managers:
What concrete slab specifications and floor flatness are required for installing movable pallet racking?
Can movable pallet racking systems operate effectively in sub-zero cold storage facilities down to −30°C?
What safety features are integrated to protect operators and forklifts in the dynamic aisle?
What happens in the event of a power outage? Can goods still be accessed?
How do you handle fire sprinkler system integration within mobile racking blocks?
What is the typical production lead time and installation schedule for overseas projects?
What information is required to receive a customized 3D layout and structural proposal?
Optimize Your Facility Volume with Turnkey Mobile Engineering
Partner directly with Guangzhou Heda Shelves Co., Ltd. Eliminate middleman costs, gain verified CE & ISO certified quality, and obtain a free 3D CAD warehouse layout design with structural calculations today.