[email protected] Serving Southeast Asia, South Asia & the Middle East
EN
Direct OEM/ODM Industrial Logistics Engineering

China Wholesale Mobile Shelving System Manufacturer & Factories

High-Density Mobile Base Mechanics, Heavy-Duty Electric Carriage Systems, and Comprehensive Warehouse Space Reclamation Solutions Engineered for Global Importers and Logistics Integrators.

Heavy-Duty & High-Density Racking Inventory

Engineered Mobile & High-Capacity Warehouse Solutions

Every shelving and racking system is fabricated with high-yield cold-rolled steel, tailored to your exact floor slab specs, pallet dimensions, and operational throughput cycles.

Technical Architecture & Spatial Economics

High-Density Mobile Base Mechanics: How Floor Density Reaches 85–90%

Traditional static warehouse pallet racking requires dedicated operating aisles for every two rows of storage. Mobile shelving and mobile racking eliminate non-productive access corridors, mounting entire structural shelving bays onto precision motor-driven kinetic bases.

Elimination of Static Aisles

By securing heavy-duty shelving units atop heavy-gauge steel mobile carriages that travel along flush or recessed ground tracks, multiple static aisles are consolidated into a single floating, dynamically commanded aisle. This instantly recovers 40% to 50% of wasted warehouse cubic volume.

Capital ROI in High-Rent Hubs

In global metropolitan logistics zones such as Singapore, Dubai, Hong Kong, and Los Angeles, square-meter facility leasing represents a primary operating expenditure. Converting to mobile base structures allows operators to double active SKU holding capacity without expanding real estate footprints.

Precision PLC Kinetic Synchronization

Modern electric mobile bases engineered in our Guangzhou manufacturing facility utilize distributed three-phase geared motor drives with variable frequency drives (VFD). This ensures synchronized startup, smooth deceleration, and zero structural shudder even when carrying loads exceeding 30 tons per bay.

Storage Racking System Type Volumetric Density Direct SKU Selectivity Floor Flatness Requirement Cold Storage Thermal Efficiency
Selective Pallet Racking 35% – 45% (Aisle Heavy) 100% (Instant Pick) Standard (DIN 18202 Tab. 3) Low (Cools Massive Void Airspace)
Drive-In Racking 60% – 70% (Dense LIFO) 15% – 20% (Batch Access) Standard / Moderate Medium (Prone to Honeycombing)
Electric Heavy-Duty Mobile Racking 85% – 92% (Maximum) 100% (Dynamic Opening) High Precision (DIN 15185 / FF50) Ultra-High (Cuts Refrigeration 40%)
Multi-Tier Mezzanine Platform 70% – 80% (Vertical Multiplier) 100% (Manual Picking) Standard Column Footing Medium (Requires Dual-Zone HVAC)
Future Procurement Trends (2025–2035)

Technological Convergence in Industrial Mobile Shelving

B2B procurement leaders are no longer sourcing simple steel structures; they are commissioning kinetic storage machinery engineered to integrate with WMS software, autonomous robotic pickers, and environmental energy controls.

IoT & Cloud Telemetry

Next-generation mobile carriages feature integrated micro-controllers reporting carriage operating hours, track motor winding temperatures, cycle counts, and predictive wheel alignment warnings directly to facility maintenance dashboards.

AGV / AMR Aisle Docking

Integration with Autonomous Mobile Robots (AMR) and AGV narrow-aisle forklifts. The warehouse management software automatically triggers aisle opening sequences before an AGV arrives, cutting cycle travel wait times to zero.

Deep-Freeze Refrigeration Drive

Cold chain facilities (-25°C to -35°C) are shifting en masse to mobile racking. Advanced units employ synthetic low-temperature gear oils, heating elements in PLC junction boxes, and stainless-steel guide tracks to prevent condensation embrittlement.

Multi-Zone Optical Envelopes

Triple-redundant safety protocols: floor-level proximity trip bars, vertical photocell safety curtains spanning the full aisle height, and long-range radar sensors that arrest carriage motion within 50ms upon detection of any obstacle.

Manufacturing Prowess & Quality Engineering

Why Tier-1 Global Contractors Source from Our Guangzhou Factory

Guangzhou Heda Shelves Co., Ltd. has stood at the forefront of heavy structural steel racking and high-density mobile shelving manufacturing since 2001. Operating a vertically integrated 30,000 square meter industrial plant, we eliminate middleman markups while maintaining strict European standard tolerances.
2001
Founded in Guangzhou
30,000 m²
State-of-the-Art Factory
30,000 Tons
Monthly Steel Output
120+
Countries & Ports Served

In-House 10-Step Precision Manufacturing & Quality Control Pipeline

01
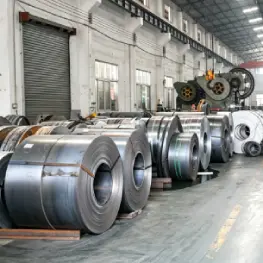
Raw Materials Coil Inspection

Steel Coil Testing

Spectrometric assay of certified Q235B/Q355B coils for yield strength & elongation.
02
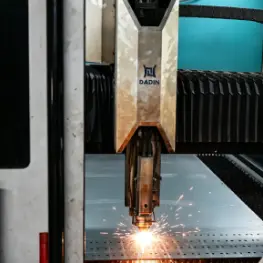
Precision Steel Laser Cutting

Precision CNC Cut

Fiber laser profiling with +/- 0.2mm tolerance for interlocking brackets and base plates.
03
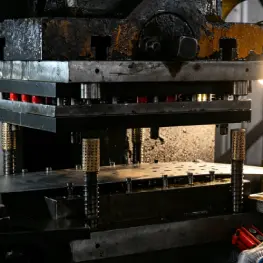
Automated Column Punching

Upright Punching

Continuous automatic rolling punch beds stamping pitch pitch holes with zero cumulative error.
04
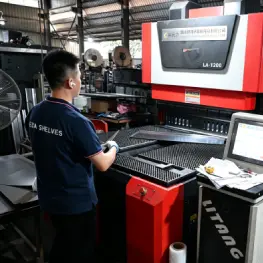
Cold Bending Forming

Cold Roll Forming

Multi-stand continuous roll forming producing stiffening ribs on structural column profiles.
05
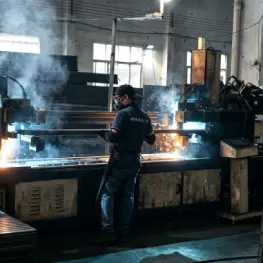
Robotic MIG Welding

Robotic Welding

Panasonic multi-axis robotic welders executing clean, deep-penetration seam joints on beam connectors.
06
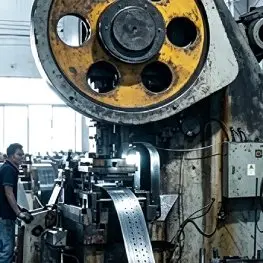
Surface Polishing

Shot Blasting

Mechanical centrifugal grit blasting stripping mill scale, rust, and oil down to bare metal.
07
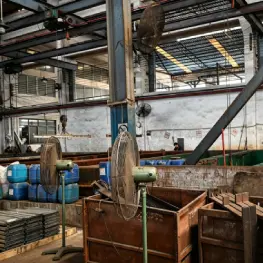
Pickling and Phosphating Pre-treatment

Chemical Wash

8-stage automatic immersion dip converting surface steel into a corrosion-resistant phosphate matrix.
08
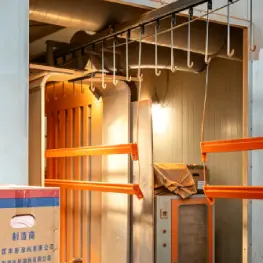
Electrostatic Powder Coating

Polymer Coating

Automated Gema electrostatic spray lines curing thermoset epoxy resin at 200°C for wear protection.
09
QC Inspection

Destructive QC

Full beam-deflection load tests, salt-spray chamber trials, and cross-hatch coating adhesion tests.
10
Container Packing

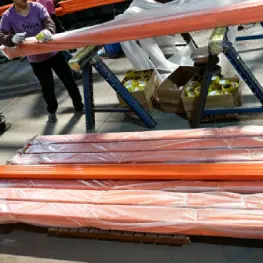
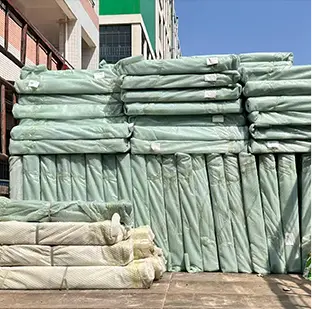
Secure Export Pack

Corrugated interleaving, steel strapping, and custom seaworthy timber skids preventing maritime transit strain.

Procurement Due Diligence

Site Engineering & Floor Slab Requirements for Mobile Systems

Because mobile shelving systems concentrate massive multi-ton dynamic loads onto narrow steel track footprints, prospective buyers must evaluate concrete slab specifications and seismic risk parameters during early budgeting.

1. Concrete Slab Load Dynamics

Unlike stationary selective racks where footings remain static, mobile carriages create alternating point loads and dynamic rolling shear stress. Slabs typically require a minimum compressive strength of 25–30 MPa (C25/30), with reinforced dual-layer rebar mesh to resist slab punching shear under high concentrated wheel wheelbases.

2. Floor Flatness & Leveling Tracks

Guide tracks must be leveled within strict tolerances—typically +/- 1.0 mm per 10 meters of run (meeting DIN 15185 or ASTM E1155 FF50 standards). Discrepancies cause carriage binding, motor amp spikes, and premature drive-wheel bearing failure. Options include floor-embedded rails during fresh pours or flush grouted retrofit channels.

3. Seismic Anchorage & Dynamic Mass

For installations in earthquake-prone belts (the Pacific Rim, Japan, the Philippines, Indonesia, or Chile), systems must comply with EN 15512 and RMI MH16.1. Mobile units feature electronic seismic trip switches that instantly park carriages in a distributed load orientation upon detecting initial P-wave tremors.

Need a Free 2D/3D BIM Warehouse Layout Design?

Our licensed senior structural racking engineers deliver full CAD layout schematics, pallet position calculations, and concrete load checks within 24 to 48 hours. Submit your warehouse architectural drawing today.

Get Catalog
B2B Procurement Knowledge Base

Frequently Asked Questions on Mobile Shelving & Racking Wholesale

Detailed engineering, manufacturing, and commercial answers addressing common technical inquiries from international project managers, supply chain directors, and warehouse contractors.

What is the structural difference between heavy-duty electric mobile pallet racking and manual hand-crank compactor shelving?
Manual hand-crank compactor shelving utilizes mechanical gear reductions (typically a 3:1 or 5:1 ratio) with bicycle chains to move light-to-medium loads (up to 800 kg per carriage bank), making it ideal for pharmaceutical archives, document storage, museums, and small spare parts rooms. In contrast, heavy-duty electric mobile racking utilizes structural I-beam or cold-formed boxed steel carriages driven by multiple three-phase AC electric geared motors synchronized via industrial Siemens or Omron PLCs. These heavy-duty industrial systems carry standard 1,000 kg – 1,500 kg Euro or GMA pallets, handling total train weights exceeding 400 metric tons per block with automated touch-screen aisle selection and radio remote controls.
How do you address rail installation on an existing warehouse concrete floor that cannot be deeply excavated?
When retrofitting an existing building where trenching or structural re-pouring is prohibited by the leaseholder or building code, we engineer surface-mounted guide rails combined with low-profile timber or aluminum chamfered ramps, or an elevated secondary false floor. Alternatively, shallow floor-sawing techniques (cutting narrow channels only 25mm to 40mm deep) allow flush guide track installation secured with high-tensile epoxy chemical anchors and non-shrink leveling grout. This allows standard counterbalanced and reach forklifts to traverse the rail footprint smoothly without wheel jarring or tire degradation.
What international engineering safety codes and certifications do your racking components hold?
Guangzhou Heda Shelves Co., Ltd. components comply strictly with European Racking Federation FEM 10.2.02 and EN 15512 design standards, alongside American RMI (Rack Manufacturers Institute) MH16.1 specifications. We hold official CE Factory Production Control Certification (Certificate No. 2435-CPR-8605159), ISO 9001:2015 Quality Management Certification (Certificate No. 18624Q00169R0M), and environmental RoHS compliance for our electrostatic thermoset powder coatings. Structural calculation reports and finite element analysis (FEA) stress validation dossiers are supplied for municipal permitting and third-party engineering reviews.
How do safety sensor networks protect personnel and forklift operators inside moving aisles?
Our systems utilize a multi-layered active and passive safety network. First, optoelectronic light barriers (safety curtains) guard the entrance of each aisle, cutting power to motor drives immediately if a person or forklift crosses the threshold while carriages are moving. Second, full-length mechanical bumper switches and optical sensor strips are mounted along the bottom edge of every carriage; any physical contact stops the drive within 50 milliseconds. Third, emergency stop mushroom buttons are placed on every carriage control faceplate, and overhead flashing LED visual alarms paired with acoustic buzzers announce carriage transit cycles in advance.
Can mobile racking be customized for cold chain logistics and sub-zero blast freezer warehouses?
Yes, cold storage is one of the highest-ROI use cases for electric mobile racking. Because refrigerated air volume is expensive to cool, compressing the storage block saves up to 40% on electrical power bills. For sub-zero operations down to -30°C, we specify specialized low-temperature carbon steel with high Charpy V-notch impact toughness to prevent cold embrittlement, IP65-sealed drive motors packed with low-viscosity synthetic polar grease, internal heating elements in the main electrical PLC enclosures to prevent condensation freezing, and polyurethane-sleeved wheels or heavy forged steel flanged rollers designed for cold room floor tracks.
What is the typical production lead time, container packing protocol, and overseas installation support?
Standard OEM production lead times range between 20 and 30 calendar days depending on tonnage and project complexity. We engineer optimized 3D container stuffing diagrams ensuring maximum weight and cube utilization in 40ft High Cube containers. All upright frames and beams are bundled with steel straps, separated by heavy-duty corrugated board, and packed on specialized steel lifting cradles for fast unloading at destination ports. For overseas installation, we provide detailed 3D step-by-step CAD installation manuals, high-definition video walkthroughs, and can dispatch seasoned installation field supervisors or project engineers directly to your job site anywhere across Southeast Asia, South Asia, or the Middle East.
How does HEDA Shelves protect structural steel from rust and corrosion in humid tropical regions?
Warehouses in tropical environments (such as Vietnam, Thailand, Malaysia, Indonesia, and coastal GCC ports) face relentless atmospheric humidity and saline corrosion. Prior to coating, all HEDA components undergo an 8-stage automatic pre-treatment process comprising hot alkaline degreasing, acid pickling, rinse passivations, and zinc-phosphate conversion coating. We then apply an electrostatic epoxy-polyester hybrid powder coating cured at 200°C, producing an impermeable dry film thickness of 60 to 90 microns. For outdoor lumber yards, chemical warehouses, or extreme humidity zones, full hot-dip galvanizing to ISO 1461 standards is available on request.
What technical data must an importer provide to receive an accurate CAD quotation and load analysis?
To generate an optimal engineering solution, please share: (1) Warehouse architectural drawings (DWG CAD file or dimensioned PDF) displaying internal clear ceiling heights, building columns, and overhead obstructions like fire sprinkler headers; (2) Pallet specifications including width, depth, overall height including cargo overhang, and gross pallet weight; (3) Operating forklift model, chassis width, turning radius, and maximum reach height; (4) Total active SKU count and required daily pallet turnover volume; and (5) Project location for local seismic and wind code compliance.