China Top Pick Flow Rack Factories & OEM Storage Engineering
An authoritative technical guide to high-density FIFO dynamic storage systems, carton and pallet roller mechanics, intelligent order fulfillment, and verified manufacturing standards from Guangzhou Heda Shelves Co., Ltd.
Enterprise Solutions
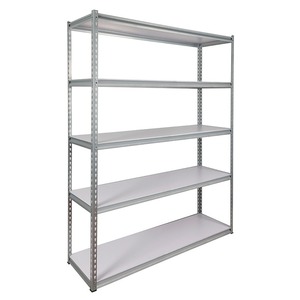
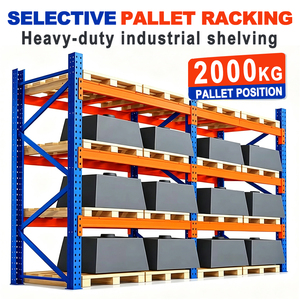
Premier Warehouse Racking & Gravity Flow Systems
Manufactured from high-grade Q235B/Q355 structural steel with multi-stage cold roll-forming and robotic phosphating. Engineered for fast-turnaround distribution, pharmaceutical supply chains, and bulk industrial consolidation.
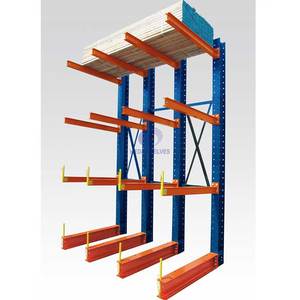
Unobstructed front arm configuration built specifically for timber, steel tubes, extrusion bundles, and non-standard bulky items with CE safety rating.
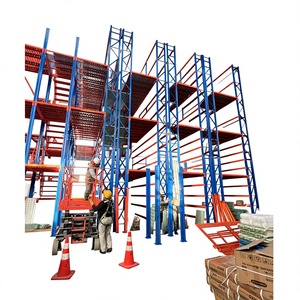
Engineered vertical space multiplier utilizing heavy upright columns to support structural steel floor decking, integral stairs, handrails, and lighting.
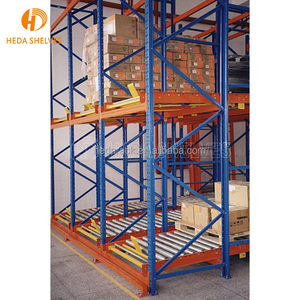
Dynamic roller bed live racking designed for automated stock progression under gravity. Ideal for fast-moving split-case picking and pharmaceutical DCs.
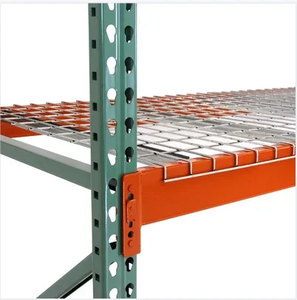
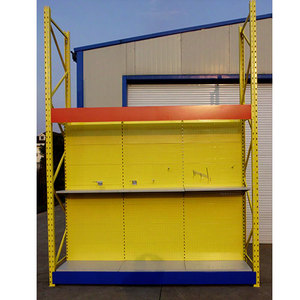
Integrated structural racking and modular perforated panel system that combines high under-shelf bulk storage with front-line hypermarket display versatility.
Full turn-key portal frame warehouse building with integrated crane girders, thermal envelope systems, and optimized column grids for high-bay flow racking.
In modern high-velocity distribution centers, storage density and order-picking velocity represent two conflicting optimization objectives. Conventional selective pallet racking offers 100% selectivity but suffers from excessive aisle footprint requirements, maintaining floor space utilization rates frequently below 40%. Conversely, drive-in systems increase spatial compaction at the cost of strict Last-In, First-Out (LIFO) inventory constraints and high forklift transit collision risks.
Dynamic live storage—specifically Carton Flow Racking and Pallet Flow (Gravity Roller) Systems—resolves this physical constraint by deploying an engineered gravitational incline plane. Operating along a precise gradient between 2.5% and 4.0% (1.5° to 2.3°), items roll seamlessly from the rear loading face to the active front picking plane. This decouples replenishment logistics from order fulfillment, achieving non-interfering dual-aisle throughput and guaranteeing strict First-In, First-Out (FIFO) batch management for perishable food, pharmaceuticals, and rapid-turn retail goods.
Controlled Kinetic Velocity
Equipped with internal centrifugal speed-controller rollers that maintain pallet speeds below 0.3 m/s, preventing terminal impact shock on downstream end-stops regardless of lane depth.
Ergonomic Tilting Trays
Integrated 10° to 15° angled presentation drop-shelves at the picking discharge point allow order selectors instantaneous line-of-sight and effortless case picking without lumbar overextension.
Dual-Flange Heavy Trackers
Cold-formed structural steel roller tracks with engineering-grade polypropylene or zinc-plated steel skate wheels, rated to withstand 15 to 80 kg individual wheel point loads.
Kinematic Formula & Incline Determination in Dynamic Gravity Flow
The operational reliability of a gravity flow system depends on the calculated balance between gravitational driving force and resistive frictional components. The acceleration vector $a$ along the roller bed is determined by the equation:
a = g × (sin(θ) - μk × cos(θ)) - (Fbrake / Mpallet)
Where θ represents the incline angle, μk is the rolling friction coefficient between the container contact plane and wheel bearings, Fbrake is the resistive drag imparted by eddy-current or centrifugal speed brakes, and Mpallet is the payload mass. When dealing with cold-room temperatures down to -30°C, lubricant viscosity increases, requiring a 0.5% upward gradient adjustment (θ ≈ 3.5%–4.2%) to prevent zero-velocity line blockages.
Enterprise Pedigree
Why Top Global Brands Partner with Guangzhou Heda Shelves
Founded in 2001, Guangzhou Heda Shelves Co., Ltd. has evolved into South China's benchmark manufacturer of precision pallet racking, heavy mezzanines, and dynamic gravity flow systems.
2001
Established Pedigree (25+ Yrs)
30,000m²
Guangzhou Modern Plant
30,000Tons
Monthly Cold-Form Output
120+
Export Destined Countries
Strict 10-Stage Precision Production & Quality Architecture
01
Raw Material Test
Certified prime Q235B & Q355B coils verified via spectrometer.
02
Precision Slitting
High-speed laser and rotary slitting lines within ±0.2mm tolerance.
18-pass dedicated roller tooling ensuring zero micro-fracturing of profiles.
05
Profile Bending
Automated continuous bending of heavy-duty boxing and step beams.
06
Robotic Welding
Pulse-shielded MIG welding of heavy connector brackets and base plates.
07
Surface Polishing
Automated de-burring and centrifugal shot blasting to remove scale.
08
Pickling & Phosphating
Multi-tank chemical wash establishing crystalline corrosion resistance.
09
Powder Coating
Electrostatic GEMA powder coating cured at 200°C (RoHS compliant).
10
Final Load Check
Batch test to EN 15512 safety deflection limits prior to export pack.
Industry Horizon
Flow Racking Procurement Trends: The 2025–2030 Outlook
Driven by automated warehousing initiatives, e-commerce micro-fulfillment centers, and escalating square-meter lease costs worldwide, procurement directors must evaluate systems against evolving automation frontiers.
1. Hybrid AGV/AMR Interface Integration
Traditional carton flow beds are evolving to integrate automated mobile robot (AMR) docking ports. Smart gravity tracks feed totes straight into autonomous retrieval systems, eliminating human travel time across primary picking zones.
2. Embedded Pick-to-Light (PTL) Tracks
Next-generation flow rack extrusions now feature integrated data cable raceways and click-in busbar channels. This facilitates plug-and-play installation of digital pick-to-light LED modules, boosting picker speed to over 400 lines/hour with 99.98% accuracy.
3. Thermal-Resilient Cryogenic Roller Alloys
Surging global cold-chain investment requires roller bearings functioning effortlessly down to -35°C without grease embrittlement. Modern specs prioritize composite acetal resin rollers and sealed precision stainless steel bearings to prevent thermal seizure.
Engineering Decision Matrix
Comparative Analysis: Live Flow Racks vs. Alternative High-Density Systems
Choosing the optimal warehouse layout requires balancing density, cycle times, throughput selectivity, and long-term operating costs.
Storage System Type
Space Utilization
SKU Selectivity
Inventory Rotation
Throughput Speed
Forklift Damage Risk
TCO Payback Period
Carton Flow Racking
High (70–80%)
100% at Picking Face
Strict FIFO
Ultra Fast (Manual/PTL)
Negligible (Protected Face)
12–18 Months
Pallet Flow (Gravity)
Very High (85%)
One SKU per Lane
Strict FIFO
High (Decoupled Aisle)
Low (External Access)
18–24 Months
Selective Pallet Rack
Low (35–45%)
100% Instant
Flexible
Moderate
Moderate to High
Baseline
Drive-In Racking
High (75–80%)
Poor (Last Pallet Only)
Strict LIFO
Slow (Deep Maneuver)
Extremely High
24–36 Months
Radio Shuttle System
Maximum (85–90%)
One SKU per Lane
FIFO or LIFO
Very High (Automated)
Very Low (In-Lane Shuttle)
20–30 Months
Procurement Knowledge Base
Frequently Asked Questions for Global Flow Rack Buyers
Clear, expert-level technical guidance to help you navigate international standards, layout designs, and installation requirements.
What gradient angle should be specified for carton flow versus heavy pallet flow systems?
For standard plastic totes and corrugated cardboard cartons, a slope gradient of 2.5% to 3.5% (approx. 1.5° to 2.0°) is recommended. Weak corrugated boxes that deform under humidity require up to 4.0% with closely spaced roller wheels to distribute floor point pressure. For pallet flow racks carrying 500 to 1,500 kg wooden or plastic pallets, a 3.5% to 4.0% incline is standardized, supplemented by speed controller drums every pallet length to keep velocity below 0.3 m/s.
How does HEDA Shelves guarantee seismic resilience for warehouse projects in high-risk zones?
We engineer racking structures compliant with European EN 16681 and US RMI MH16.1 seismic criteria. When supplying to seismic zones like Indonesia, the Philippines, New Zealand, or Latin America, our structural engineers model the site's Peak Ground Acceleration (PGA) using finite element analysis (FEA). We scale column steel thicknesses up to 2.5mm or 3.0mm, engineer enlarged seismic baseplates, integrate reinforced vertical/horizontal K-bracing frames, and specify Hilti heavy chemical anchor bolts to handle dynamic lateral shear.
What international quality certifications and load calculation standards do you provide?
Guangzhou Heda Shelves Co., Ltd. holds verified CE Certification (No. 2435-CPR-8605159) under the Construction Products Regulation, alongside ISO 9001:2015 Quality Management certification (No. 18624Q00169R0M). Every customized flow rack and pallet rack project is delivered with structural calculation documentation adhering to EN 15512:2020 (Steel static storage systems) or ANSI/RMI specifications, complete with official material mill test certificates (MTC) for steel yield performance.
How are components pre-treated against corrosion for tropical and coastal environments?
Unlike budget suppliers who only wipe steel surfaces before painting, our components complete an automated multi-stage immersion treatment: alkaline degreasing, acid pickling to eliminate scale, and chemical phosphating to create an anti-rust molecular barrier. Finally, products receive electrostatic thermoset polyester powder coating cured at 200°C (60–80 micron film thickness), verified by 500-hour salt spray testing. For extreme cold-storage, maritime, or corrosive chemical zones, full hot-dip galvanization to ISO 1461 is available.
Can carton flow roller tracks be retrofitted onto our existing pallet racks?
Yes. Our carton flow beds are designed for universal compatibility. Utilizing adjustable front and rear hanger brackets, our roller beds mount cleanly onto conventional box beams, step beams, or structural steel angles from almost any manufacturer. We only require your clear beam opening dimension, beam profile width, and upright frame depth to supply custom-length tracks and drop-in lane dividers.
What information is required to receive a free customized 2D/3D layout design within 24 hours?
Simply supply: (1) Warehouse architectural CAD plan or dimensioned layout showing column positions and clear building height; (2) Pallet or carton dimensions (Length × Width × Height) including packaging weight; (3) Forklift model, turning radius, and maximum reach height; and (4) SKU volume and daily unit movement metrics. Our team will return a complete 2D layout, 3D perspective rendering, and structural load analysis free of charge within 24 to 48 hours.
Engineer Your High-Density Dynamic Warehouse Layout Today
Eliminate dead aisle space, accelerate fulfillment rates, and reduce ongoing labor expenses. Partner directly with Guangzhou Heda Shelves' dedicated engineering team for tailor-made CAD layouts, structural load checks, and verified factory direct pricing.
24-Hour Drawing Turnaround
CE & ISO 9001 Certified
Global Containerized Shipping
Consult a Racking Engineer
Ready to evaluate flow rack feasibility or request a customized layout proposal for your facility?