Structural Safety • FEM 10.2.02 • ANSI MH16.1 Certified
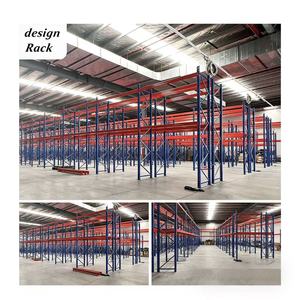
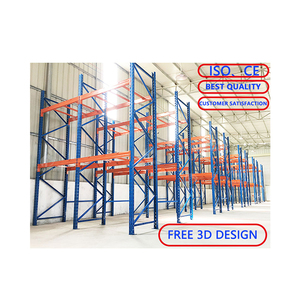
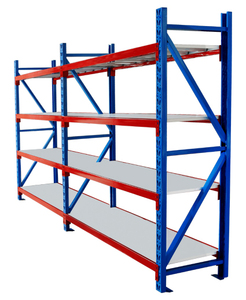
China Best Large Pallet Racking Supplier & Exporters
Global engineering whitepaper and specification manual on heavy-duty industrial storage racks, seismic-certified load frameworks, and end-to-end logistics manufacturing by HEDA Shelves.
Enterprise Product Inventory
Engineered Large-Capacity Pallet Racking Series
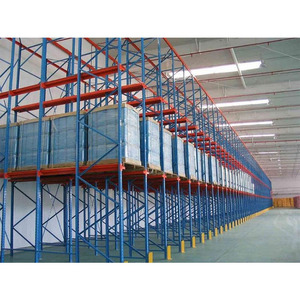
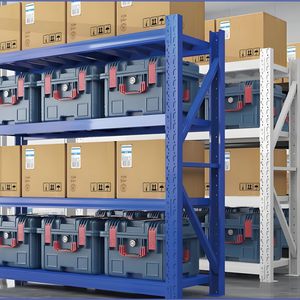
Fabricated from prime cold-rolled Q235B and Q355B structural steel, our heavy-duty racking systems deliver precision roll-formed upright sections, high torsion-resistant box beams, and fail-safe safety pins verified for high-bay logistics facilities.
Large-scale industrial pallet racking requires deep consideration of material yield properties, residual stress mitigation, and seismic elastic-plastic deformation. As China's leading exporter of warehouse steel infrastructure, Guangzhou Heda Shelves Co., Ltd. specifies high-grade, continuous cold-rolled steel (predominantly certified Q235B and high-yield Q355B with minimum tensile strengths of 510 MPa).
Unlike light commercial shelving, industrial racks encounter dynamic cyclic loads produced by reach trucks, counterbalanced forklifts, and semi-automated pallet shuttles. Beam deflection calculations strictly conform to the L/200 criteria stipulated in FEM 10.2.02 and ANSI MH16.1, ensuring serviceability deflection under maximum rated uniform distributed load (UDL) does not exceed 1/200th of the clear horizontal beam span.
Key Engineering Metric: Under full pallet payload, column upright profiles undergo Finite Element Analysis (FEA) to confirm buckling resistance over unbraced lengths. Omega-shaped column profiles featuring 11 to 13 distinct folding facets deliver up to 34% greater torsional rigidity than generic European or American C-profiles.
Beam-to-column connections integrate cold-stamped five-hook claw brackets with high-shear carbon steel locking pins. This joint geometry eliminates catastrophic accidental dislodgement from upward forklift impact while offering substantial rotational stiffness to curb building sway during seismic events.
Precision Fabrication Tolerances vs. International Norms
Exporting large structural pallet racking to rigorous jurisdictions like Australia (AS 4084), the European Union (EN 15512), and North America requires millimeter-level geometric tolerance control throughout punching, rolling, and automated robotic welding.
Yield Strength VerificationMill cert heat analysis accompanying every production batch.
Future Procurement Trends in Large Warehouse Storage (2025–2030)
Global supply chain disruptions, rising urban square-meter lease rates, and accelerating warehouse automation are fundamentally reshaping heavy-duty storage acquisition. Forward-thinking procurement teams assess four overarching structural shifts.
ASRS & RGV Hybrid Symbiosis
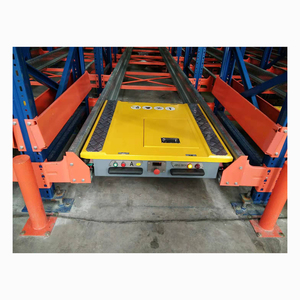
Warehouses are moving rapidly away from pure manual forklift handling. Specifiers now insist on "Automation-Ready" racking. Systems must be engineered with the deflection stiffness, guide rail mountings, and optical sensor targets necessary to transition seamlessly into 4-way radio shuttles or automated rail-guided vehicles without dismantling steel columns.
Vertical Height Maximization & FAR Constraints
In mega-hubs like Singapore, Dubai, and Hong Kong, logistics real estate demands optimal Floor Area Ratio (FAR). High-bay installations routinely scale between 12 and 22 meters. This transition mandates roll-forming lines capable of producing single-piece un-spliced uprights that eliminate splicing joint weak points under extreme top loads.
Seismic Resilience & Micro-Zoning
Standard safety factors no longer satisfy sovereign code compliance across the Pacific Rim, the GCC, and Southeast Asia. Project engineers increasingly demand site-specific nonlinear response history analysis, ductility calculations, and enlarged footplates that dissipate base-shear energy during major seismic events.
Green Steel Sourcing & ESG Traceability
International tenders now audit the embodied carbon of warehouse racking. HEDA Shelves utilizes scrap-recycled EAF (Electric Arc Furnace) and low-emission BF-BOF steel supplies, paired with heavy-metal-free, low-VOC thermoset powder formulations that comply rigorously with European REACH and RoHS standards.
Modular Rack-Supported Mezzanine Synthesis
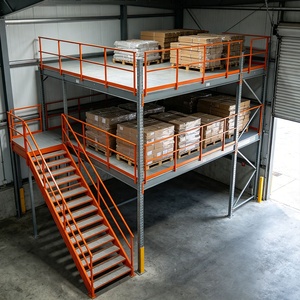
Instead of executing expensive civil expansions, industrial tenants favor multi-tier rack-supported platforms. These multi-level mezzanines effectively triple picking volume over identical warehouse foundations, offering flexible disassembly and relocation when lease contracts expire.
BIM Integration & Digital Twin Design
Racking procurements now require accurate IFC/Revit 3D models. Warehouse planners integrate racking blueprints directly into broader warehouse architecture simulations, verifying sprinkler pipe clearances, conveyor junctions, and automated forklift turning radiuses long before containers arrive on-site.
Enterprise Reliability & Manufacturing Power
Guangzhou HEDA Shelves: 25 Years of Global Racking Leadership
Established in 2001, Guangzhou Heda Shelves Co., Ltd. has developed into an internationally respected OEM & ODM manufacturer of warehouse storage racks, heavy cantilever systems, and structural mezzanines, deploying over 10,000 logistics installations worldwide.
2001
Founded Year (25+ Yrs Industry XP)
30,000m²
Advanced Guangzhou Factory Facility
30,000Tons
Monthly Cold-Formed Steel Capacity
120+
Export Destined Countries & Regions
Full In-House Industrial Value Chain
Unlike export trading intermediaries, HEDA Shelves directly controls every link in production: structural engineering, raw strip slitting, automated roll-forming, laser profiling, robotic welding, 9-stage surface pre-treatment, and electrostatic powder coating. Maintaining our entire workflow in our Guangzhou manufacturing hub guarantees mill-certified dimensional repeatability and rapid container turnaround to major maritime shipping lanes.
Our engineering division delivers free customized CAD layouts and 3D architectural renders within 24 to 48 hours. Whether your facility stores standard EUR/GMA pallets, awkward industrial drums, or automotive dies, HEDA engineers tailor upright pitch, beam depths, row-spacer ties, and anti-collapse mesh walls to your operational forklift mast and floor capacity parameters.
Accredited Export Credentials: HEDA Shelves operates under verified CE Certification (No. 2435-CPR-8605159), ISO 9001:2015 Quality Management System (Certificate No. 18624Q00169R0M), and certified chemical coatings complying strictly with RoHS environmental safety requirements.
Optimized Container Stuffing & Freight Economics
Heavy pallet racking shipping costs are driven by cargo volume and steel tonnage balances. Our logistics logistics team executes specialized mathematical 3D container packing software for every single shipment, maximizing TEU and FEQ container cube utilization to 92–96%.
Beams, uprights, and accessories are packaged with protective shock-absorbing corrugated interleaves, reinforced structural strapping, and anti-abrasion edge protectors to survive long intermodal ocean journeys across Southeast Asia, the Middle East, Europe, and the Americas.
Guangzhou Port Proximity:Huangpu / Nansha Maritime Terminals (Under 40km)
How do Q235B and Q355B steel grades impact pallet racking load safety factors?
Q235B steel offers a minimum yield strength of 235 MPa and ultimate tensile capability of 370–500 MPa, serving as the dependable worldwide standard for selective pallet racks with tier capacities up to 3,000 kg. For deep-lane, heavy dynamic systems (such as Drive-In or Radio Shuttle racks) and extreme high-bay uprights exceeding 10 meters, HEDA utilizes Q355B (yield strength ≥ 355 MPa). This higher yield point increases axial load-bearing capacity by 28% without requiring excessive profile wall thickness, keeping structure weight efficient and minimizing total ocean freight expense.
How are HEDA racking systems customized for high-risk seismic environments?
For earthquake-prone destinations across the Pacific Rim and Southeast Asia (e.g., the Philippines, Indonesia, Japan, New Zealand) as well as the Middle East, our design engineers apply dynamic modal and seismic response spectrum calculations in accordance with local building regulations. We specify heavy-duty ductile baseplates with enlarged surface areas, dual anchor bolting, heavy-gauge diagonal bracing frameworks, and back-to-back row spacers engineered to dissipate lateral ground acceleration shocks.
What anti-corrosion protection is implemented for tropical humidity and cold rooms?
Standard warehouse racks undergo a 9-stage pre-treatment cycle comprising chemical degreasing, acid rust-pickling, and zinc phosphating, followed by automated electrostatic deposition of an 80–100 micron thermoset polyester powder coat cured at 200°C. For cold storage and blast freezers (−30°C) or high-humidity coastal sites across ASEAN territories, we provide continuous hot-dip galvanizing (HDG) per ISO 1461, achieving a robust zinc barrier exceeding 65–85 microns that permanently wards off rust and flaking.
What precise data is required to generate a complimentary 2D CAD & 3D layout?
To deliver an engineering-grade layout within 24–48 hours, our technical team requires: (1) Warehouse architectural drawings indicating clear ceiling heights, column grids, fire doors, and obstructions; (2) Pallet specifications including overall dimensions (Width × Depth × Height) and maximum loaded pallet weights; (3) Forklift equipment models, turning radius, and maximum reach lift heights; (4) Total SKU profile count and anticipated stock turnover methodology (FIFO or LIFO).
How does HEDA ensure international compliance certifications (CE, ISO, RoHS)?
All HEDA manufacturing processes are strictly certified under ISO 9001:2015 Quality Management standards (Certificate No. 18624Q00169R0M). Structural pallet racking and mezzanine components exported to Europe and the West carry authentic CE Certification (No. 2435-CPR-8605159) based on structural calculation standards EN 15512 and EN 1090-1. Coating powders are tested by third-party laboratories to guarantee total compliance with RoHS and REACH environmental health guidelines.
What are standard export production lead times and ocean shipping cycles?
Standard production runs for full container loads (1 to 5 × 40HQ containers) average 15 to 20 working days following technical drawing approval. Our manufacturing plant is situated under 40km from the deep-water maritime hubs of Guangzhou (Nansha/Huangpu) and Shenzhen (Yantian/Shekou). Ocean transit times span approximately 3–7 days to ASEAN ports, 12–18 days to the Middle East, and 20–28 days to European and North American ports.
Can existing selective pallet racking be converted into automated shuttle lanes?
Yes. If upright profiles, baseplates, and concrete floor slab compression strengths meet the required engineering thresholds, selective frames can be retrofitted with specialized galvanized shuttle guide rails, entry guide funnels, and horizontal stability portal ties. Our engineers review your original rack engineering documentation to verify structural safety margins before proposing a shuttle retrofit.
How are site installations handled for overseas logistics projects?
Every shipment is accompanied by comprehensive, color-coded 3D installation drawings, component identification manifests, anchor tightening torque charts, and instructional video tutorials. For major turnkey industrial projects or complex multi-tier mezzanine floors, HEDA Shelves deploys experienced on-site installation supervisors to direct your local installation teams, ensuring flawless assembly and local authority inspection clearance.
Ready to Optimize Your Warehouse Capacity & Floor Efficiency?
Request an engineering review today. Receive a free structural load check, professional 2D CAD layout, 3D architectural render, and a direct factory quotation from China's leading pallet racking manufacturer.