Featured Industrial Storage Systems & Dynamic Racks
Explore heavy-duty selective frames, carton live storage platforms, gravity roller beds, and cantilever structures directly engineered and roll-formed in our ISO 9001 certified manufacturing plant.
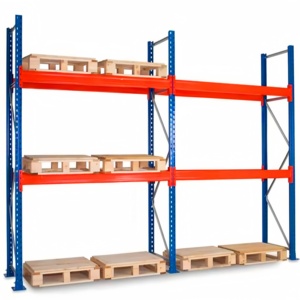
High Quality Kaku KKPR0001 Double Deep Rack Heavy Duty Steel Selective Pallet Rack Bin Rack 500-1500kg/Level for Warehouse
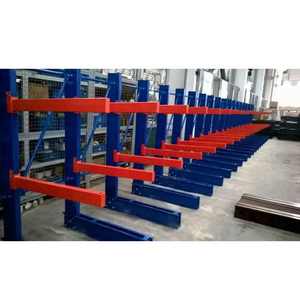
High Quality Boltless Adjustable Metal Selective VNA Pallet Rack Factory Direct Cantilever Rack For Warehouses
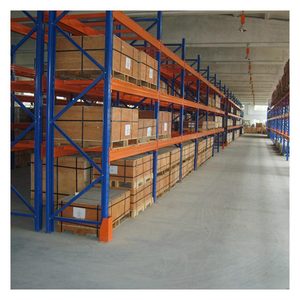
Heavy Duty Boltless Shelving Industrial Metal Racking System Steel Warehouse Rack Shelf for Selective Pallet Storage
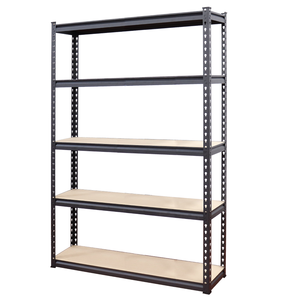
5 Tier Storage Shelving 1.5mm Boltless Carbon Steel Frame 12mm MDF Shelf Board Heavy Duty Garage Shelves 2200Lbs
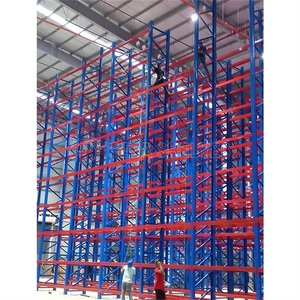
Warehouse Pallet Racking System Heavy Duty Metal Storage Rack And Rack Shelves For Warehouse
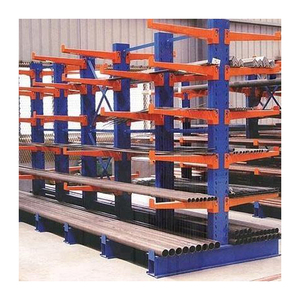
H-Beam Heavy Duty Cantilever Racks Steel Structural Shelf Industrial Warehouse Racking for Storaging Wooden Boards, Pipes
Customized Warehouse Pallet Racking Steel Galvanized Wire Mesh Decking Storage Rack Dividers with Good Price for
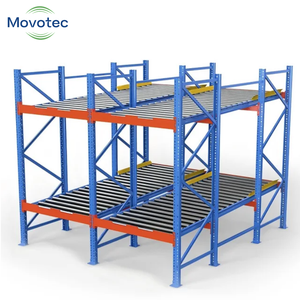
Warehouse Storage Racks Shelving Systems Pallet Rack Gravity Roller Flow Racking Movotec MTG100 1 Year Warranty
Kinematics & Structural Mechanics of Carton Flow Shelving
Carton flow shelving—also internationally classified as carton live storage or dynamic roller racking—operates as a high-density, dynamic order picking engine that harnesses gravitational force to propel plastic totes, corrugated cardboard boxes, and split cases from rear replenishment faces to front picking terminals along inclined skate-wheel beds.
The Physics of Gravity Incline & Friction Dynamics
The core mechanical stability of a carton flow bed depends directly on the calculated declination angle (θ), the dynamic rolling friction coefficient (μd) between the carton base and the roller material, and the dynamic load distribution across successive wheel tracks.
In standard warehouse operations, carton flow tracks are calibrated at a slope between 2.5° and 4.5° (representing a pitch gradient of approximately 45mm to 75mm per linear meter of track). When corrugated shipping boxes exhibit bottom sag under humid tropical ambient conditions, dynamic resistance increases by up to 35%, necessitating the integration of secondary roller tracks or zinc-coated steel roller tracks rather than traditional virgin ABS wheels.
Our Guangzhou engineering department utilizes high-precision cold-formed side guide rails and full-length aluminum sub-tracks that guarantee continuous carton tracking without lateral binding or run-out derailment.
-
75% Travel Reduction Drastically cuts operator order picking footsteps
-
Strict FIFO Compliance Guarantees batch freshness and expiration control
-
Dedicated Split-Aisle Replenishment never obstructs picking traffic
-
Drop-In Flexibility Easily mounts into existing selective pallet rack frames
Carton Flow vs. Alternative Storage Systems
Warehouse designers must balance capital expenditure (CapEx), operational throughput, and volumetric spatial efficiency. Below is a comparative operational matrix evaluated by industrial storage engineers.
| Evaluation Parameter | Carton Flow Shelving | Static Longspan Shelving | Push-Back Rack (Carts) | Mini-Load AS/RS System |
|---|---|---|---|---|
| Primary Material Flow | Strict FIFO (First-In, First-Out) | Static (Manual Access) | LIFO (Last-In, First-Out) | Dynamic Software Governed |
| Picking Travel Reduction | 60% – 75% Reduction | Baseline (High Travel) | 30% – 40% Reduction | Up to 90% (Goods-to-Person) |
| SKU Presentation Density | Extreme (Full Frontal Faces) | Moderate to Low | High (Palletized) | Maximum |
| CapEx per SKU Location | Low to Moderate ($$) | Low ($) | Moderate ($$$) | Very High ($$$$$) |
| Aisle Traffic Segregation | 100% Split (Pick vs. Restock) | Zero (Shared Aisle Conflict) | Shared Front Face | Complete Automated Enclosure |
| Installation & Commissioning | 3 – 5 Days (Modular Boltless) | 1 – 2 Days | 5 – 7 Days | 6 – 12 Months |
| Maintenance Overhead | Near Zero (Gravity-Driven) | Zero | Low (Track/Wheel Checks) | High (Sensors, Motors, PLCs) |
Why HEDA Shelves Is China's Premier Racking Manufacturer
Founded in 2001 in Guangzhou, Guangzhou Heda Shelves Co., Ltd. has spent over two decades engineering precision warehouse storage systems. Operating from our 30,000 square meter advanced industrial manufacturing hub, we maintain continuous in-house quality control across every production stage.
Rigorous Certified Compliance
Full compliance with CE Certification (No. 2435-CPR-8605159), ISO 9001:2015 Quality Management (Certificate No. 18624Q00169R0M), and RoHS-compliant environmental powder formulations.
Automated In-House Roll Forming
From raw decoiling to CNC multi-station cold roll-forming lines, automated upright column punching, and precision robotic welding arms, we eliminate dimensional deviation and assembly field errors.
Tropical & Seismic Regional Engineering
Tailored engineering for seismic hazard regions (Japan, Philippines, Indonesia) and tropical monsoon climates (Vietnam, Malaysia, UAE) featuring high-adhesion phosphating and hot-dip galvanized protections.
10-Step Quality Verification & Traceability Protocol
Every linear meter of carton flow rail and pallet rack upright passing through our Guangzhou manufacturing facility undergoes an uncompromising 10-phase inspection pipeline.
Raw Coil Audit
Spectrometric and tensile verification of certified Q235B/Q355B steel coils for carbon and yield uniformity.
Slitting & Cutting
High-speed computerized uncoiling and precision slitting to ±0.1mm dimensional tolerance.
CNC Punching
Automated hydraulic punch presses stamping teardrop, diamond, and hexagonal pitch patterns.
Cold Roll-Forming
Multi-station cold roll profile forming maintaining consistent wall thickness across upright contours.
Robotic Welding
Multi-axis robotic GMAW welding for beam end connectors ensuring zero slag inclusions and full penetration.
Shot Blasting
Mechanical shot blasting and micro-polishing to remove mill scale, surface oxides, and oil films.
Phosphate Pretreatment
Chemical degreasing, acid pickling, and hot zinc phosphating creating an active anti-corrosive anchor layer.
Powder Coating
Electrostatic powder deposition cured in 200°C baking tunnels for scratch-resistant 80μm polymer film.
Deflection Testing
Static load tests enforcing maximum beam deflection limits of L/200 under 125% rated maximum payload.
Export Container Stowing
Computerized container packing plans, steel banding, corrugated cushioning, and waterproof wrap.
Future Sourcing & Engineering Trends (2025–2030)
Global supply chains demand higher SKU throughput, micro-fulfillment precision, and seamless compatibility with autonomous mobile robotics. Discover where carton live storage engineering is heading.
Hybrid Flow Beds for AMRs
Next-generation carton flow beds integrate automated feed stops and laser-guided roller tracks designed for collaborative Autonomous Mobile Robots (AMR) and robotic case-picking end effectors.
Pick-to-Light & IoT Sensing
Universal snap-on aluminum front extrusions wired with embedded digital pick-to-light displays, optical stock-out infrared sensors, and real-time SKU depletion telemetry connected to warehouse WMS.
Cryogenic Cold-Chain Composites
Specially formulated low-temperature impact polyolefins and synthetic low-viscosity ester lubricants that resist roller brittleness, binding, and fracturing in -30°C pharmaceutical and frozen food storage.
Modular Universal Drop-In Tracks
Shift from rigid dedicated shelf systems toward modular roller rail assemblies that drop seamlessly into standard step beams, giving 3PL warehouses the agility to reconfigure lanes in under 15 minutes.
Overseas Sourcing & Factory Audit Checklist for China
Direct procurement from Chinese racking suppliers provides immense pricing and customization advantages. However, professional supply chain directors evaluate rigorous engineering standards prior to issuing a Purchase Order.
Essential Technical Milestones for Tender Verification
When auditing potential suppliers in China for heavy-duty carton flow and selective racking projects, prioritize physical manufacturing verification over generic trading agency claims:
1. Mill Test Certificates (MTC): Request EN 10204 Type 3.1 chemical analysis and tensile yield test verification demonstrating certified minimum yield strength (typically ≥ 235 MPa for Q235B and ≥ 355 MPa for Q355B structural steel).
2. Salt Spray Corrosion Endurance: Confirm third-party salt spray testing per ASTM B117 or ISO 9227. Premium electrostatic coatings must demonstrate no blister creepage after 500 hours of continuous saline exposure.
3. Shipping Volume & Stowing Optimization: Structural racking profiles and roller tracks represent volumetric cargo. HEDA Shelves engineers utilize dedicated 3D container stowing simulations that nest beam profiles, stack upright trusses, and optimize 40ft High Cube container filling rates above 92%, saving buyers thousands in ocean freight per megawatt-hour equivalent.
Purchasing & Engineering Inquiries
Clear answers to frequent technical, logistical, and structural questions raised by international warehouse managers, project engineers, and supply chain executives.
How do engineers determine the exact bed slope for carton flow shelving?
Can carton flow roller tracks be retrofitted into our existing pallet racks?
What is the maximum weight capacity per lane on carton flow systems?
How do you safeguard racking against seismic activity in vulnerable zones?
What documentation accompanies every overseas export shipment?
How does HEDA Shelves prevent coating corrosion in high-humidity climates?
Request an Engineered Warehouse Layout & Factory Quote
Send your warehouse floor plans, carton dimensions, and throughput goals. Our engineering department delivers complimentary 2D CAD layouts, 3D renderings, and structural price evaluations within 24 to 48 hours.