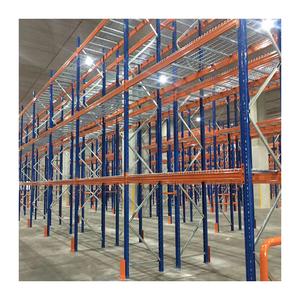
 100% Direct Access
Heavy Duty Industrial Storage Warehouse Rack Selective Pallet Racking Shelves
Load: 1000–4500 kg/lvl
Q235B Steel
75mm Pitch
From standard high-turnover selective systems to harsh-environment bulk mining and corrosive material racks, explore our factory-tested, CE-compliant pallet storage series engineered with premium Q235B and Q355B structural steel.
100% Direct Access
 Anti-Pressure / Mining
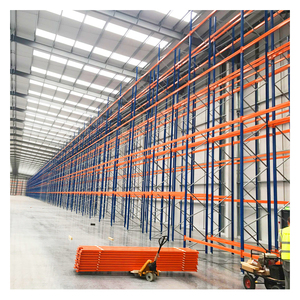 Factory Direct
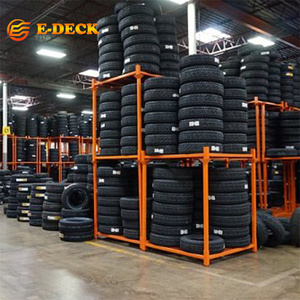 Modular Stacking
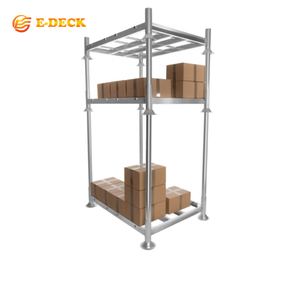 Portable Flexible
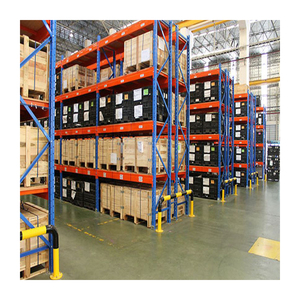 OEM & ODM Series
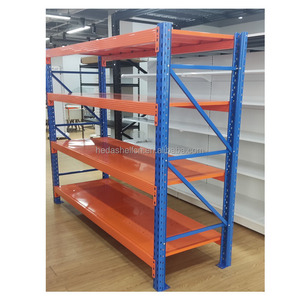 Medium-Heavy Longspan
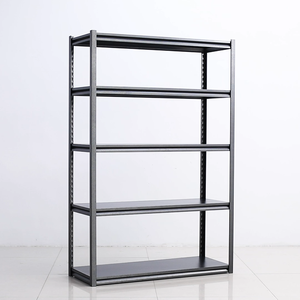 Boltless Adjustable
Specifying industrial racking for modern high-bay facilities demands rigorous adherence to structural engineering benchmarks. In static steel storage systems, structural failure is rarely the result of a single overload event; rather, it stems from progressive fatigue, under-engineered upright-to-beam connection moments, and uncalculated torsional buckling under eccentric forklift dynamic impact.
At Guangzhou Heda Shelves Co., Ltd., our heavy-duty racking columns and load beams are calculated under limit state principles adhering to EN 15512:2020 (European Standard for Steel Static Storage Systems) and American RMI (Rack Manufacturers Institute) MH16.1. Utilizing high-tensile certified structural carbon steel (grades Q235B and Q355B), our cold roll-formed upright sections possess a minimum yield strength ($f_y$) of 235 to 355 MPa, designed with continuous multi-bend omega (Ω) profiles to maximize the section modulus and second moment of area ($I_x, I_y$).
Every beam tier is engineered so that under maximum allowable safe working load (SWL), vertical deflection strictly satisfies $\delta \le L/200$ for standard pallet storage, and $\delta \le L/300$ for automated crane and shuttle systems, mitigating dangerous pallet creep and dislodgement risks.
Beam-end connectors feature 3 to 5 claw precision-punched hooks engaging with heavy-duty column slots. Combined with high-shear safety locking pins resisting vertical disengagement forces exceeding 5.0 kN, our structural connections prevent accidental uplift caused by operational mast collision during rapid pallet retrieval.
| Structural Metric | Standard Heavy Duty | HEDA Engineered System |
|---|---|---|
| Base Steel Standard | Commercial Q195 / Q215 | Certified Q235B / Q355B (EN 10025) |
| Upright Yield Strength | $\approx 195\text{ MPa}$ | $\ge 235\text{–}355\text{ MPa}$ Tested |
| Deflection Tolerance | $L/150$ | Strict $L/200$ to $L/300$ |
| Pre-treatment Process | Simple solvent wipe | Continuous Pickling & Phosphating |
| Powder Coating Thickness | 40–50 $\mu\text{m}$ | 65–85 $\mu\text{m}$ Electrostatic Cure |
| Seismic Load Calculation | Generic nominal load | Site-specific AS 4084 / Eurocode 8 |
| CE Conformity File | Self-declaration | Notified Body No. 2435-CPR-8605159 |
Continuous automated roll-forming lines ensure millimetric precision with zero edge cracking. Profiles incorporate stiffening ribs along upright webs to resist flexural-torsional buckling under concentrated compressive loads.
Beam connectors and base plates are welded via robotic CO2/MIG arc systems. Full-penetration fillet welds prevent localized stress fractures under heavy cyclic pallet dynamic loading and seismic ground motion.
Components pass through automated 9-tank pickling, degreasing, and zinc-phosphating lines before applying thermosetting polyester epoxy powder, verified to withstand 500+ hours of continuous salt spray testing.
Industrial supply chain infrastructure is undergoing seismic transformation. Rising urban industrial land costs, automated guided vehicle (AGV) integration, and decarbonization mandates are reshaping how enterprise logistics directors procure static storage.
Procurement is pivoting away from low-density wide-aisle formats toward automated 2D Radio Shuttle and Autonomous Mobile Robot (AMR) compatible racks. Eliminating forklift access aisles increases cubic volumetric efficiency by up to 75%.
Global logistics hubs situated along the Pacific Rim and Mediterranean seismic zones now mandate site-specific dynamic response spectrum calculations. Upright baseplate anchor embedment depth and ductile bracing topology are engineered directly into tenders.
Multinational 3PLs require Scope 3 embodied carbon disclosure. Procurement specifications prioritize manufacturers leveraging scrap-based electric arc furnace (EAF) steel and TGIC-free thermosetting powder with zero heavy-metal leaching.
With cold storage facilities facing surging energy tariffs, refrigerated warehouses demand high-density drive-in and deep-lane flow racks. Minimizing refrigerated void spaces directly lowers refrigeration compressor energy draw per stored pallet.
Enterprise procurement professionals increasingly recognize that initial steel tonnage cost accounts for less than 35% of a warehouse racking system’s 15-year lifecycle expense. Premature upright deflection from inferior steel grades, recurring forklift impact repairs, and non-compliant pallet beam locks generate catastrophic operational downtime. Specifying certified structural engineering reduces operational maintenance overhead by over 60% across the asset's active life.
Every steel batch must be accompanied by EN 10204 Type 3.1 mill test certificates, validating carbon equivalent (CEV) values for weldability and notch toughness at sub-zero temperatures.
VNA (Very Narrow Aisle) high-bay installations require floor flatness ratings aligned with DIN 18202 Table 3 or Concrete Society TR34 (DM1/DM2 specifications) to prevent mast oscillation.
Future-proof racking frames are cold-formed with standard 50mm or 75mm adjustability increments, allowing seamless multi-tier mezzanine conversion or automated roller integration.
Established in 2001 in Guangzhou, China, Guangzhou Heda Shelves Co., Ltd. has developed from an engineering metal fabrication workshop into a world-class manufacturing powerhouse for heavy-duty industrial pallet racking and multi-tier structural mezzanines.
Spectrometric & tensile testing of certified Q235B/Q355B coils.
CNC slitting of master coils with width tolerances within ±0.1mm.
Multi-punch CNC lines stamping precise 50/75mm pitch teardrop or diamond holes.
Continuous progressive roll-forming of intricate omega (Ω) upright geometries.
Continuous seam roll-forming of heavy-duty interlocking box beams.
Mechanical surface smoothing eliminating sharp flash and stress points.
Automated robotic CO2 shielded welding of connector claws & baseplates.
Submersion degreasing, acid pickling, and micro-crystalline zinc phosphating.
Automatic powder booth with 200°C high-temperature thermoset curing.
Destructive batch testing, steel strapping, and export container blocking.
Guangzhou HEDA Shelves provides comprehensive structural documentation required by civil structural engineers, municipal building authorities, and international customs clearance agencies. We do not provide off-the-shelf static shelving; every system is engineered against your local building code and seismic zone requirements.
Clear, technically verified answers regarding structural engineering, CE compliance, floor slab loads, and logistics consolidation directly from HEDA's Senior Engineering Team.
To prepare an accurate structural calculation report and CAD plan, our engineers require: (1) Warehouse architectural drawings showing clear height to lower roof truss obstruction and column grid; (2) Concrete slab compressive strength ($f'_c \ge 25\text{–}30\text{ MPa}$), thickness, and reinforcement details; (3) Pallet specifications including width, depth, overall height (including load), and maximum gross weight; (4) Forklift specifications including model, turning radius (Aisle AST), collapsed mast height, and maximum lift height; and (5) Local seismic acceleration parameters ($S_s, S_1$) if applicable.
Our racking systems are produced under Factory Production Control (FPC) audited pursuant to the European Construction Products Regulation (CPR 305/2011/EU) and EN 15512:2020. Our CE Certificate No. 2435-CPR-8605159 is issued by a recognized European Notified Body. Every export order is accompanied by a formal Declaration of Performance (DoP), structural calculation datasheets, and steel mill test certificates (EN 10204 3.1) confirming chemical composition and mechanical yield strength.
Standard industrial upright columns exert significant concentrated point loads through baseplates to the building slab (often ranging from 40 kN to over 150 kN per column foot). Typically, an uncracked reinforced concrete slab with a minimum thickness of 150mm to 200mm and compressive strength of C25/30 (25–30 MPa) is necessary. We engineer custom enlarged, heavy-gauge baseplates to distribute point loads and prevent localized concrete punching shear failure.
Yes. Low-temperature environments (down to -30°C) cause structural carbon steel to undergo ductile-to-brittle transition. For deep-freeze warehouses, we specify low-temperature impact tested structural steel (Q355D/E or S355NL) with proven Charpy V-notch energy values. For surface protection against condensation and corrosion, hot-dip galvanizing conforming to ISO 1461 is available alongside our cold-resistant thermosetting epoxy coatings.
Q235B is standard carbon structural steel with a minimum yield point of 235 MPa, offering high ductility and optimal roll-forming properties for standard height pallet racks. Q355B is a high-strength low-alloy (HSLA) steel with a yield point of 355 MPa (~50% stronger). We utilize Q355B for tall high-bay uprights (over 8 meters), heavily loaded Drive-In cantilever arms, and high-capacity mezzanine primary beams, reducing overall deadweight while ensuring exceptional buckling resistance.
We engineer a multi-layered impact protection system: (1) Heavy-duty column wrap-around guards manufactured from 4mm–6mm formed plate anchored directly to the slab; (2) Heavy-duty C-channel end-of-row barrier frames absorbing kinetic energy at turning intersections; (3) Internal column stiffening sleeves inserted in bottom upright segments; and (4) High-visibility safety yellow powder coating (RAL 1023) adhering to international safety visibility standards.
Typical fabrication lead time for standard project sizes (2–10 full container loads) is 15 to 25 working days. Located in Guangzhou with direct proximity to Nansha and Shenzhen container terminals, we engineer specialized export packing bundles with steel strapping, corrugated board interleaving, and custom timber cribbing. This ensures maximum 40ft High Cube container volumetric utilization (typically 24–26 metric tons per container) and zero transit friction damage.
Every project shipment includes fully dimensioned CAD assembly drawings, anchor bolt torque specifications, and component identification tags matching the packing list. For large-scale international warehouse implementations, we provide step-by-step video installation guides, remote engineering supervision via video conference, or deploy Senior Installation Superintendents to oversee and certify your local contractor’s installation on site.
Don't base critical warehouse capital investments on guesswork. Submit your warehouse floor plan, ceiling clear height, and pallet details to receive an engineer-verified CAD layout design, static load simulation, and comprehensive bill of materials within 24 to 48 hours.
Access our comprehensive 2026/2027 Heavy Duty Pallet Racking Engineering Handbook, complete profile load tables, and CE certification documentation.
Get Catalog